Formula details
Product Details
Overview
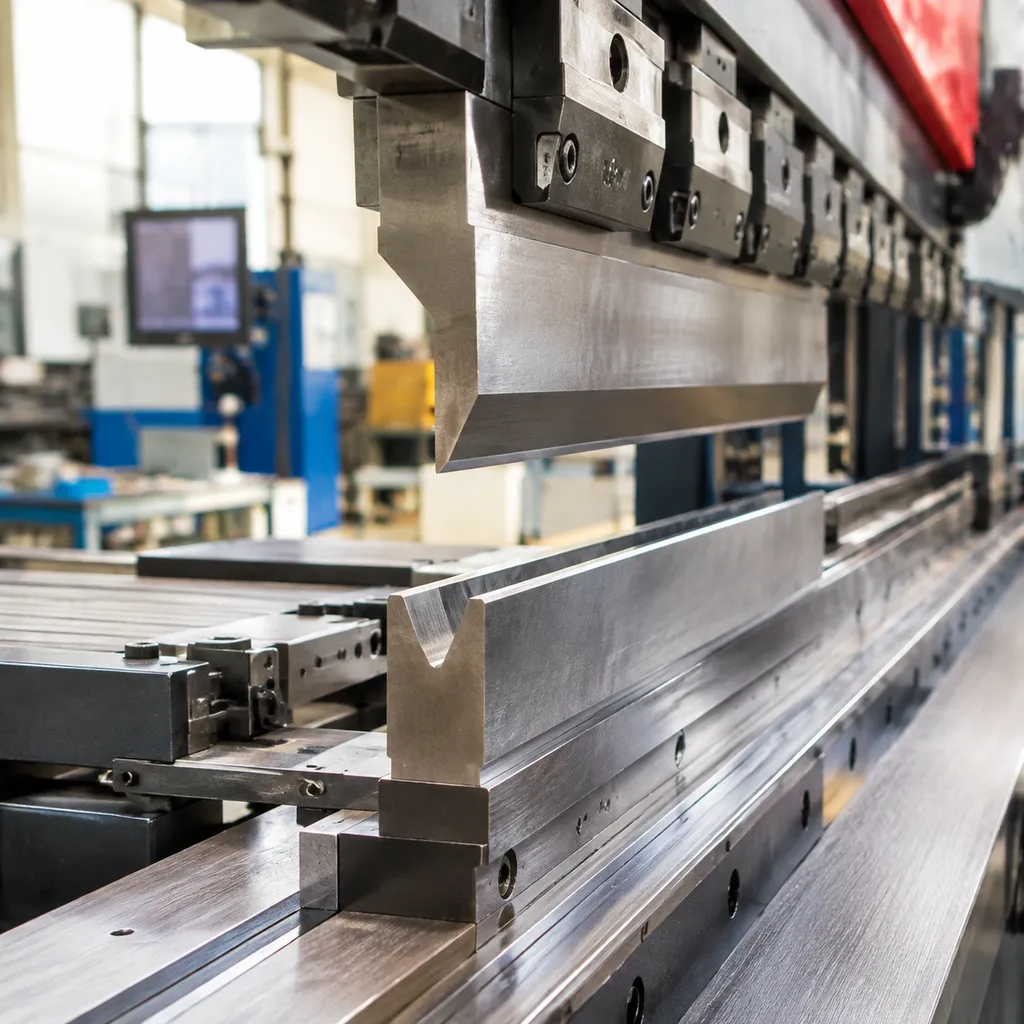
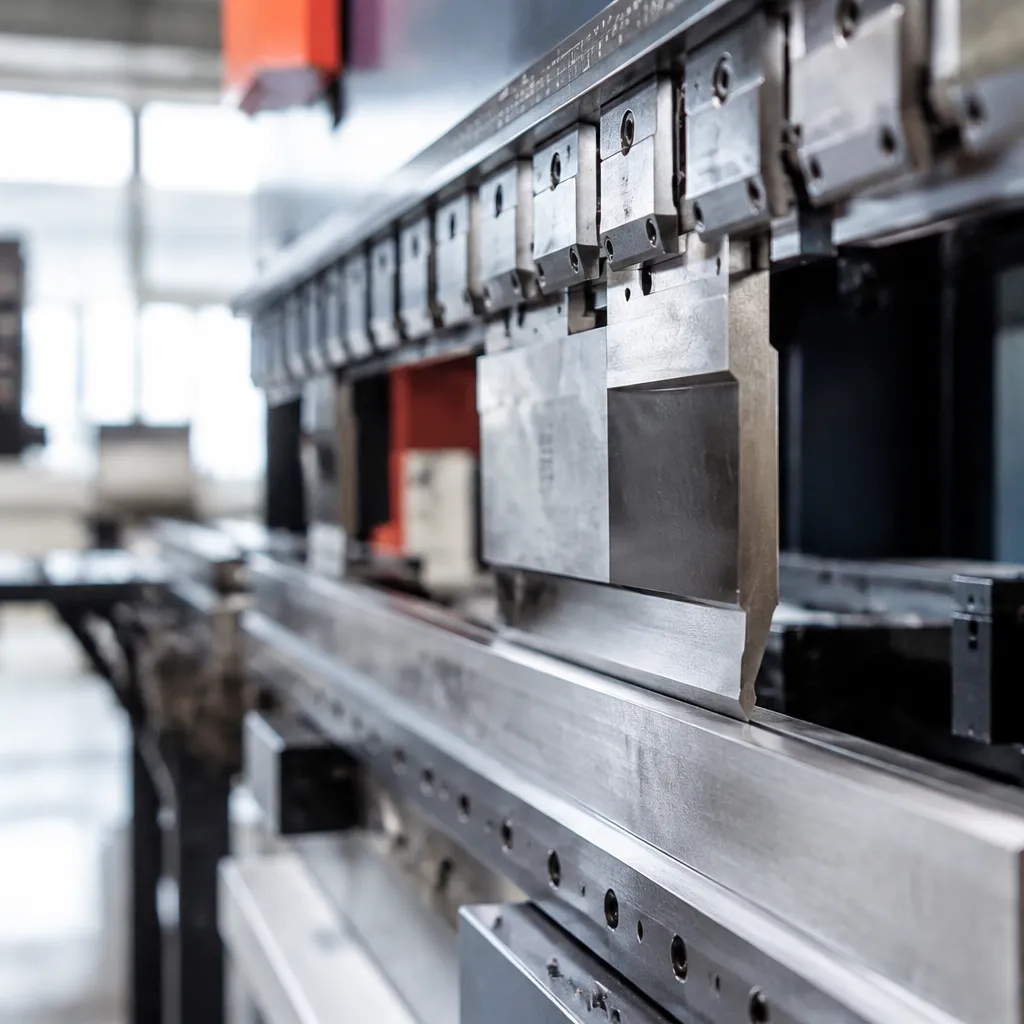
Bystronic Press Brake Punch Type RF-A 30 Overview
Technical Profile Summary
| Parameter | Specification |
|---|---|
| Tool Type | RF-A Style Upper Punch (30° Acute Angle) |
| Machine Compatibility | Bystronic / Beyeler RF-A Clamping Systems |
| Clamping Style | Hydraulic Quick-Clamping & Mechanical Clamping |
| Base Material | Premium 42CrMo / 42CrMo4 Alloy Tool Steel |
| Working Edge Hardness | 47–53 HRC / 56–60 HRC (Induction/Laser Hardened) |
| Manufacturing Process | Full-Length CNC Deep Grinding |
| Standard Lengths | 500 mm, 515 mm, 1000 mm, and Sectionalized Sets |
Seamless RF-A Clamping Integration
Every precision Bystronic press brake punch type RF-A 30 features a standardized RF-A tang designed for instant alignment in both hydraulic and mechanical tool holders:
- Direct Drop-in Fit: Mounts directly into original Bystronic upper beams with zero modification or secondary shimming.
- Rapid Tool Setup: Fully compatible with automated and quick-clamping mechanisms to minimize changeover downtime.
- Firm Clamping Lock: Precision-machined contact shoulders eliminate tool shifting under high-tonnage forming cycles.
Engineered Precision and Material Durability
We manufacture each standard and custom Bystronic press brake punch type RF-A 30 using forged alloy tool steel, combining rigid core toughness with wear-resistant contact surfaces.
- Full-Length CNC Precision Grinding: Tangs, working radii, and reference shoulders are ground to ultra-tight tolerances, ensuring perfect interchangeability and uniform bend angles across the entire bed length.
- High-Grade 42CrMo4 Construction: Resists high compressive stress, preventing structural cracking or deflection under heavy tonnage.
- Localized Hardening: High-frequency induction hardening on the critical 30° tip preserves tip geometry and prevents premature tool wear.
Technical Specifications of Bystronic Press Brake Punch Type RF-A 30
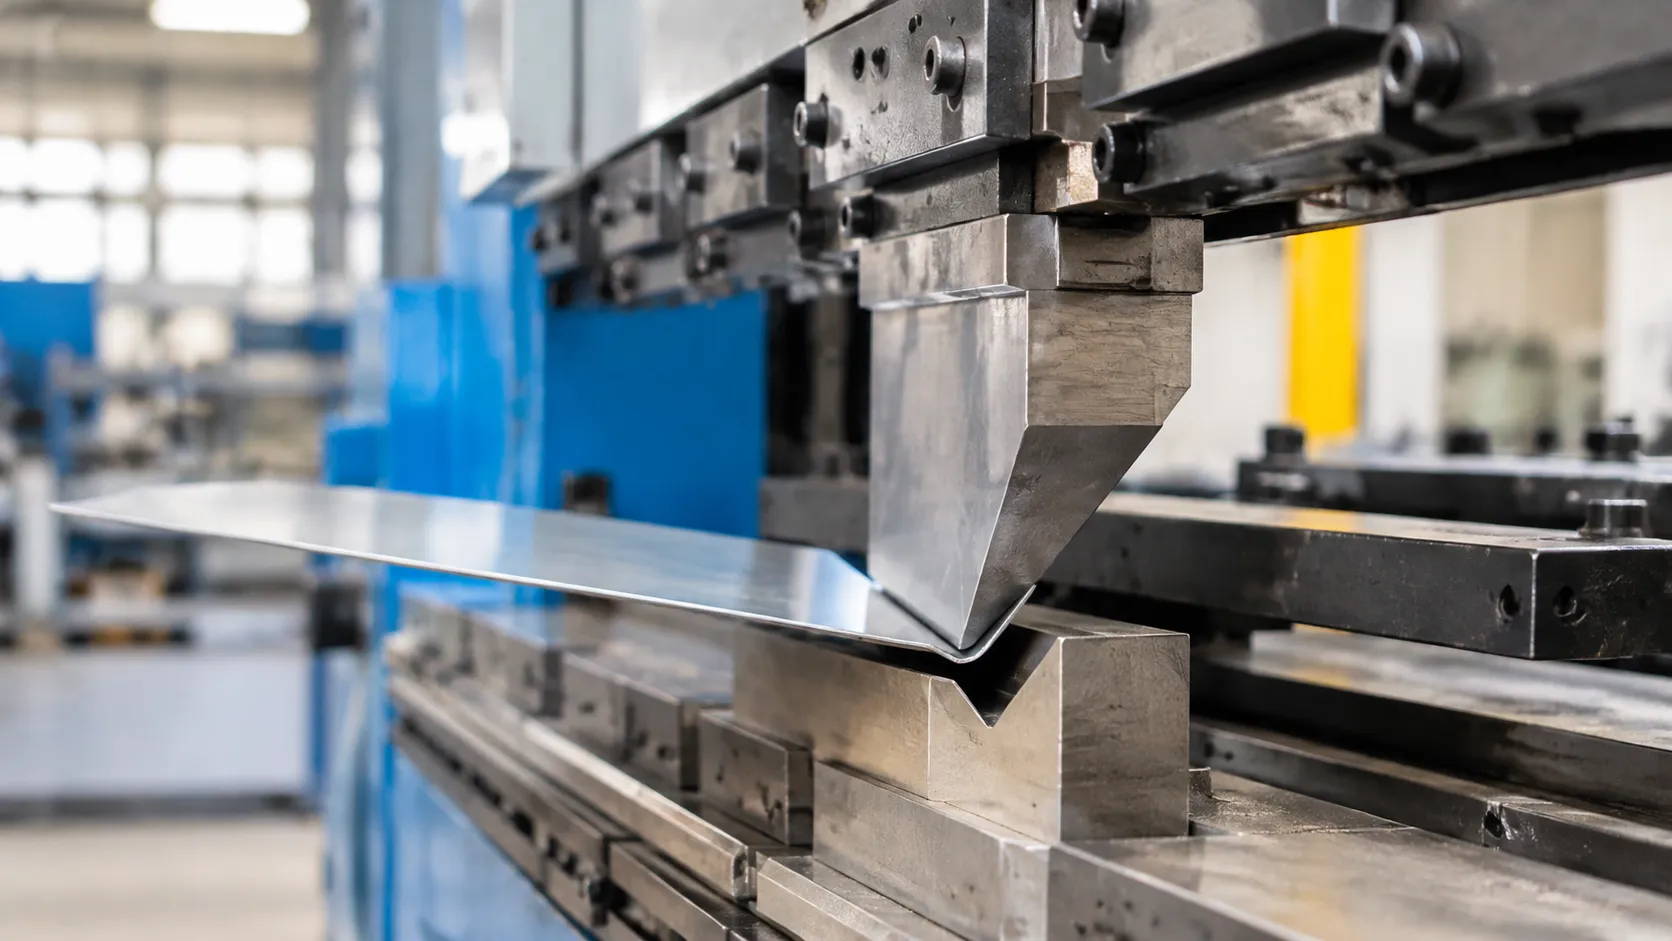
We manufacture every bystronic press brake punch type rf-a 30 to exact geometric standards, providing reliable performance for acute bending, deep channel forming, and pre-hemming operations. Seamlessly pair this tooling with a matching 30-degree press brake die for air bending and hemming to achieve stable angular precision across various sheet gauges.
Material Properties & Dual-Hardness Structure
- Steel Grade: Forged 42CrMo and 42CrMo4 alloy tool steel delivering superior core tensile strength and impact toughness under high tonnages.
- Dual-Hardness Treatment: Quenched and tempered body (28–32 HRC) prevents brittle tool fracture, while localized high-frequency induction hardening on the working tip reaches 52–56 HRC for extended wear resistance.
- Tight Manufacturing Tolerances: Full CNC precision grinding guarantees height tolerances within ±0.01 mm and total straightness within ±0.02 mm/m for continuous multi-segment setups.
- Safe Working Load: Engineered to handle bending forces up to 1000 kN/m (100 t/m). Always reference our press brake v-die chart and tonnage guide to confirm tonnage limits based on your sheet thickness and tip radius.
Standard Dimensions & Parameter Matrix
| Parameter | Standard Specification |
|---|---|
| Tool Style | Bystronic RF-A / Beyeler Style Upper Punch |
| Profile Angle | 30° Acute |
| Standard Tip Radii | R0.6 mm, R0.8 mm, R1.0 mm, R1.5 mm, R2.0 mm, R3.0 mm |
| Material Base | 42CrMo / 42CrMo4 Tool Steel |
| Working Edge Hardness | 52–56 HRC (Deep Induction Hardened) |
| Body Hardness | 28–32 HRC (Tough Core) |
| Working Height Tolerance | ±0.01 mm |
| Parallelism & Straightness | ±0.02 mm / 1000 mm |
| Maximum Load Capacity | Up to 1000 kN/m (100 t/m) |
| Clamping Compatibility | Bystronic RF-A Mechanical & Hydraulic Clamping Systems |
Precision Bystronic Press Brake Punch Type RF-A 30 Engineering
We manufacture every precision bystronic press brake punch type rf-a 30 to strict dimensional standards, ensuring direct compatibility and repeatable forming accuracy across Bystronic and Beyeler clamping systems. Our CNC grinding and finishing processes eliminate tooling deflection and minimize setup adjustments on high-volume production lines.
- CNC Deep-Ground Parallelism: We grind load-bearing shoulders, rear reference planes, and mounting tangs in continuous multi-axis setups. This tight parallelism across the full tool length ensures instant seated alignment and equal tonnage distribution across your upper beam.
- Wear-Resistant Tip Geometry: Each tip radius is precision-ground and hardened to prevent profile breakdown under continuous high-tonnage cycling. When paired with matching acute press brake dies for precision metal bending, our punches deliver consistent angle accuracy and clean bend lines from the first hit to the last.
- RF-A Quick-Clamping Integration: Engineered with standard RF-A mounting tang dimensions, our top tools support vertical click-in loading and rapid automated hydraulic clamping, cutting tool-change downtime.
- Anti-Marring Surface Treatments: Low-friction, fine-ground tool flanks prevent galling, reducing sheet drag and eliminating surface scratches on sensitive stainless steel, pre-painted sheets, and architectural aluminum.
Custom Bystronic Press Brake Punch Type RF-A 30 Options
Standard tooling cannot solve every forming challenge. When your sheet metal parts feature narrow channels, high return flanges, or severe material springback, we engineer every custom bystronic press brake punch type rf-a 30 to match your exact part geometry and production volume.
Engineered Modifications for Complex Bending
- Tailored Tip Radii (R0.2 mm to R6.0 mm): We grind custom punch nose radii to match diverse sheet gauges, preventing sheet cracking on thick stock and ensuring sharp inside corners on precision electronics.
- Extended Heights & Throat Relief Pockets: For deep box forming and complex return flanges, we manufacture punches with extended overall heights and milled relief windows to eliminate workpiece collisions.
- Custom Acute Angles for Springback Control: When air-bending stainless steel or high-tensile alloys, standard angles may not yield a true 90-degree finish. Refer to our press brake die angles guide for springback selection to match acute punch angles (such as 26° or 28°) with your material properties.
- Engineered-to-Order DXF/CAD Workflow: Send us your 2D/3D part profiles or DXF drawings. We verify bending simulation, calculate tonnage limits, and deliver custom prototypes rapidly.
| Customization Parameter | Standard RF-A 30 Profile | Custom RF-A 30 Options | Fabrication Benefit |
|---|---|---|---|
| Punch Tip Radius | R0.6 mm / R1.0 mm | R0.2 mm – R6.0 mm | Eliminates part cracking across varying sheet gauges |
| Bending Angle | 30° acute | 24° – 35° modified | Direct compensation for high springback metals |
| Tool Height / Clearance | Standard height | Extended height & deep relief cuts | Enables deep enclosure and 4-sided box forming |
| Tang & Safety Style | Standard RF-A tang | Mechanical pins or quick-lock systems | 100% compatibility with Bystronic clamping systems |
Our CNC grinding ensures every precision bystronic press brake punch type rf-a 30 modification maintains strict shoulder-to-tip dimensional accuracy, delivering consistent bending performance directly out of the crate.
Standard Lengths and Sectionalized Tool Sets
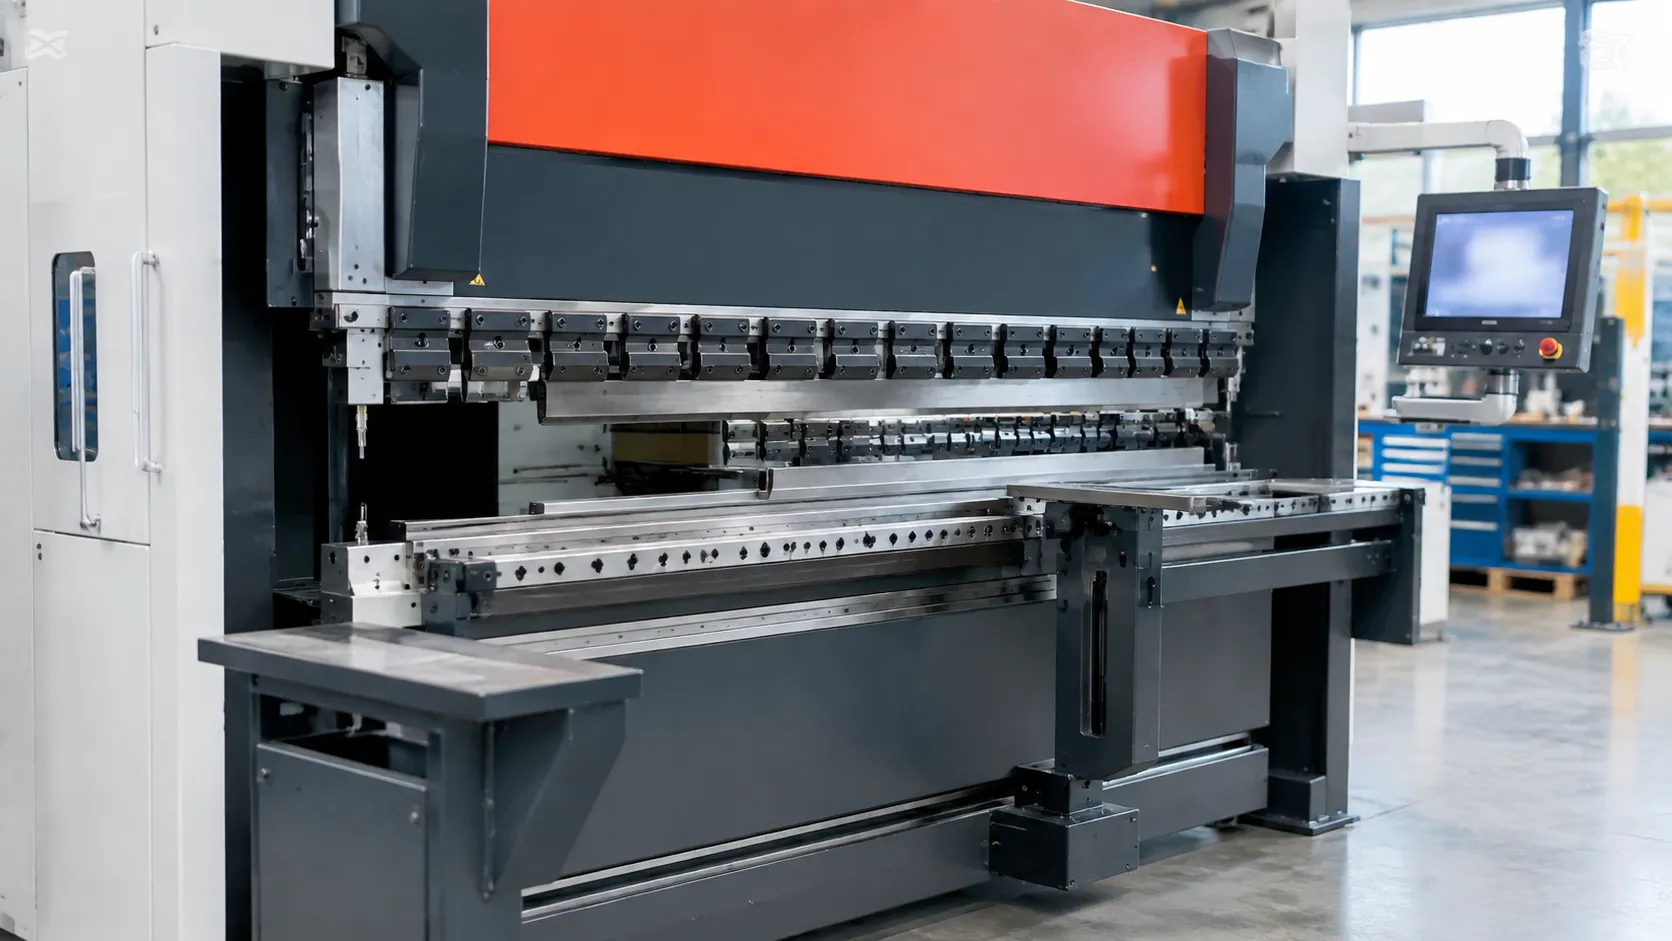
Standard Solid Lengths
For standard production runs and full-bed air bending, we stock solid punches in standard industry lengths:
500 mm solid
515 mm solid
1000 mm solid
Sectionalized Sets for Box and Pan Forming
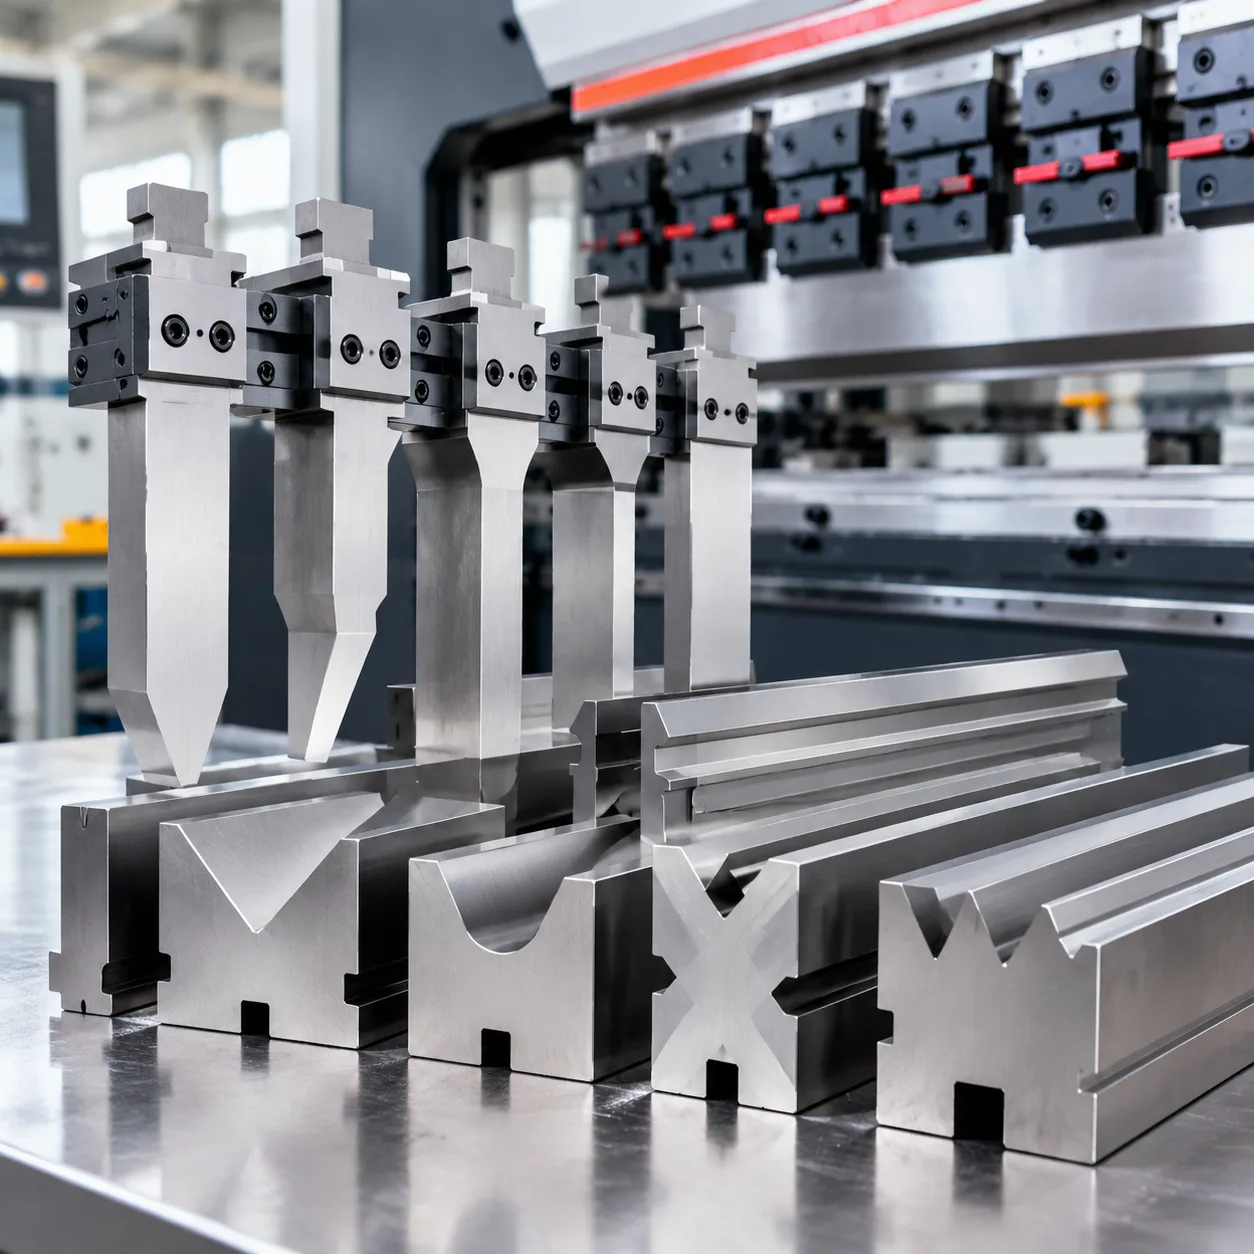
To handle return flanges, deep boxes, and closed pans, our sectionalized precision bystronic press brake punch type rf-a 30 sets come pre-cut with left and right horn pieces (ears) and multiple segment widths.
| Segment Type | Standard Available Widths (mm) |
|---|---|
| Horn Segments (Ears) | 100 mm Left / 100 mm Right |
| Intermediate Segments | 10, 15, 20, 40, 50, 100, 200, 300 mm |
| Total Standard Set Lengths | 550 mm, 1100 mm, or custom combined configurations |
Precision Height-Matching Across Segments
Every segment in a sectionalized set undergoes simultaneous CNC precision grinding. We match the working height tolerance across all segments within ±0.01 mm.
- Seamless Alignment: Combine any number of segments along the upper beam without steps or gap variations.
- Consistent Part Quality: Eliminates localized pinching and uneven bending angles when bending across multiple pieces.
- Complete Setup Compatibility: Matches perfectly with standard lower tooling and our precision press brake bottom dies for unified tooling alignment.
For specialized bending windows, we also configure custom bystronic press brake punch type rf-a 30 sectional layouts built to your exact box geometry and depth requirements.
Forming Applications and Material Compatibility
We engineer the bystronic press brake punch type rf-a 30 to handle versatile forming operations across tough production environments. The acute 30-degree profile gives your press brake maximum flexibility for tight geometries, deep return flanges, and multi-stage bends without workpiece interference.
Versatile Bending Operations
- Precision Air Bending: Delivers exact angular accuracy while overcoming springback on high-tensile metals.
- Acute Pre-Hemming: Forms the initial 30° sharp bend required for smooth, closed seams and safety edges.
- Bottoming & Coining: Supports precision bottoming setups on thinner gauge metals thanks to laser-hardened tip radii.
Sheet Metal & Alloy Compatibility
Our precision bystronic press brake punch type rf-a 30 is manufactured from deep-hardened 42CrMo4 alloy steel, delivering reliable performance across a broad range of sheet materials:
- Mild Steel & Galvanized Sheet: Smooth bending without tool surface wear or zinc pickup.
- Stainless Steel & High-Finish Alloys: Exceptional resistance to galling and tool marking during heavy-duty stainless steel processing.
- Aluminum Alloys: Prevents edge cracking on soft, ductile grades while keeping sharp inside radii consistent.
- High-Strength Alloys & Hardox: Handles extreme yield strengths without plastic tool deformation or edge chipping.
Target Industrial Applications
From standard production runs to specialized fabrications using a custom bystronic press brake punch type rf-a 30, our tooling is widely trusted across critical fabrication sectors:
- Electrical Enclosures & Cabinets: Deep channels, return flanges, and narrow box profiles.
- Industrial Server Racks & Chassis: High-density, tight-tolerance electronic hardware housings.
- HVAC & Ductwork: Hemmed edges, seam locks, and profile transitions.
- Architectural & Elevator Panels: Clean, scratch-free surface bends on decorative sheet metal.
Quality Assurance for Precision Bystronic Press Brake Punch Type RF-A 30
We maintain a strict quality control workflow from raw alloy ingot to final surface finish. Every standard and custom bystronic press brake punch type rf-a 30 goes through multi-stage testing to ensure total reliability under heavy bending loads.
- Ultrasonic Raw Material Testing: Before machining begins, we run full ultrasonic flaw detection on our 42CrMo4 steel billets to check for internal micro-cracks, inclusions, or voids. You can consult our press brake tooling material guide for in-depth steel grade and tensile data.
- Multi-Stage Heat Treatment: We through-harden the core to 28–32 HRC for optimal shock absorption, followed by high-frequency induction hardening on the 30-degree tip radius and load shoulders to achieve a wear-resistant 56–60 HRC working zone.
- CMM and Optical Profile Verification: Our quality team uses high-precision Coordinate Measuring Machines (CMM) and optical profile projectors to verify working heights, tip radius concentricity, and straightness within ±0.01 mm per meter.
- 100% Fitment Validation: Every precision bystronic press brake punch type rf-a 30 is test-mounted on standard Bystronic hydraulic and mechanical clamping beams to verify automatic alignment, seating depth, and quick-clamp engagement across our entire Bystronic tooling lineup.
Frequently Asked Questions: Bystronic Press Brake Punch Type RF-A 30
Is this RF-A 30 punch fully interchangeable with original Bystronic tooling?
Yes. Every standard and precision bystronic press brake punch type rf-a 30 we manufacture features exact tang dimensions and reference shoulder heights. They drop directly into original Bystronic and Beyeler mechanical or hydraulic clamping systems without modification, allowing seamless integration alongside your existing acute punches and factory tooling.
What is the standard lead time for custom-engineered RF-A 30 punches?
Standard stocked lengths ship immediately from our warehouse. For a custom bystronic press brake punch type rf-a 30 with tailored tip radii, special throat relief, or non-standard working heights, our direct manufacturing workflow typically delivers completed, heat-treated tools within 2 to 3 weeks following CAD/DXF drawing approval.
Can you deliver custom-segmented punch sets matched to specific part drawings?
We regularly produce precision-matched sectionalized sets for complex box, pan, and chassis bending. All segments are ground together in a single clamping setup to maintain identical working heights across the entire bend length. You can explore our standard and custom configurations across our complete range of press brake punches.
How do we calculate the safe tonnage limit for this 30-degree acute punch?
Because a 30° acute profile features a narrower body than standard 86° or 90° tools, maximum allowable tonnage per meter depends on the tool's tip radius, overall height, and material grade (such as 42CrMo4). We laser-engrave the rated max load directly onto the tool body. When air-bending high-tensile sheet metal, selecting the correct tip geometry is vital to prevent tool overload and maintain part accuracy.