

Formula details
Product Details
Overview
30 Degree Press Brake Die Capabilities & Versatility
Precision Sheet Metal Bending
Our 30 degree forming press brake die provides the deep relief required for acute angle forming, return bends, and tight-clearance geometries. By maximizing space around the punch tip, this tooling eliminates workpiece collision issues common with standard 88° or 90° dies.
Air Bending Versatility: 30° Acute Folds to 90° Bends
Through air bending, a single 30-degree acute die handles a broad spectrum of bend angles without swapping lower tooling:
30° Acute Bends: Produces sharp, high-precision acute angles in standard and high-tensile sheet metal.
45° to 60° Intermediate Angles: Enables controlled over-bending to offset aggressive material springback.
90° Universal Bends: Forms precise 90-degree right angles, significantly cutting down machine setup time and tool inventory requirements.
Stage-One Pre-Hemming Integration
Our acute tooling works seamlessly as a stage-one pre-hemming tool for two-step hem creation:
1. Pre-Bend (Stage 1): The 30° acute die creates an initial tight pre-fold in the sheet metal edge.
2. Flattening (Stage 2): A dedicated flattening die or combination hemmer closes the fold to form a smooth, secure seam.
Precision Surface Grinding & Tolerances
- Profile Accuracy: Precision CNC ground to tight ±0.01 mm profile tolerances along the full tool length.
- Consistency: Delivers flawless angle accuracy and uniform flange heights across long production runs.
- Surface Quality: Smoothly finished V-groove working radii minimize friction and prevent surface galling on sensitive sheet materials.
30 Degree Press Brake Die Dimensions & Specifications
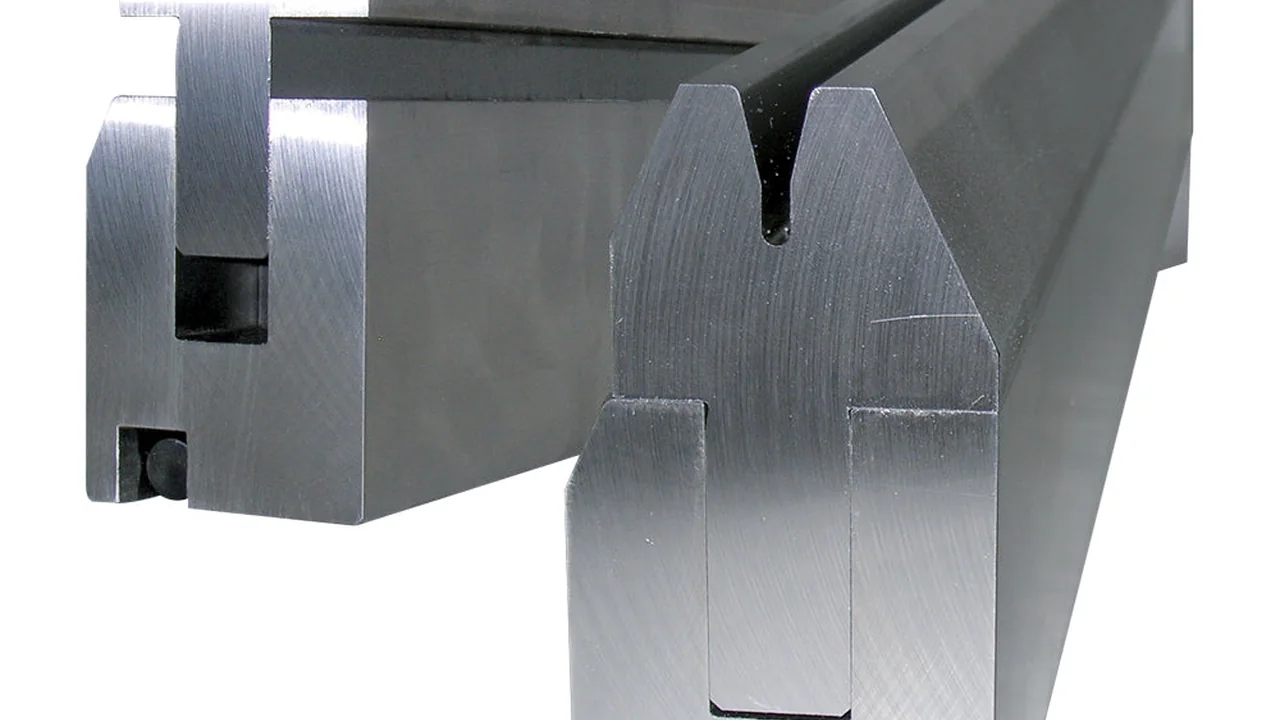
Key Dimensional Parameters
- Die Angle: 30° ± 0.5° acute profile for high springback compensation
- V-Opening Widths: 6 mm to 50 mm standard stock (custom widths available)
- Shoulder & Bottom Radius: Precision-ground radii (R0.6 mm to R3.5 mm) to prevent micro-fractures in high-tensile sheet metal
- Height & Centerline: Machined bed-to-centerline tolerances within ±0.01 mm for seamless tool interchangeability
Standard V-Opening & Load Specifications
Selecting the right V-opening acute bottom die depends directly on material thickness and required bending force. Before setting press brake pressure parameters, consult our press brake V-die chart and tonnage guide to verify max tonnage capacity per meter.
| Material Gauge (Sheet Thickness) | Recommended V-Opening | Standard Die Height | Max Tonnage Capacity (Tons/Meter) |
|---|---|---|---|
| 0.5 mm – 1.2 mm | 6 mm – 8 mm | 80 mm – 120 mm | 40 – 55 T/m |
| 1.5 mm – 2.0 mm | 10 mm – 12 mm | 80 mm – 120 mm | 60 – 80 T/m |
| 2.5 mm – 3.0 mm | 16 mm – 20 mm | 100 mm – 150 mm | 85 – 110 T/m |
| 4.0 mm – 6.0 mm | 25 mm – 50 mm | 120 mm – 160 mm | 120 – 160 T/m |
Stock Lengths and Segmented Tooling Options
Our 30 degree press brake die inventory is supplied in versatile length options to fit all major machine beds:
- Standard Solid Lengths: 835 mm and 415 mm full-length sections
- Segmented Sets: Pre-cut multi-piece sets (including 10 mm, 15 mm, 20 mm, 40 mm, 50 mm, 100 mm, and 200 mm pieces) for complex box-forming and return flange clearance
- Custom Cuts: Machined to exact lengths based on specific workstation requirements
High-Tensile Steel & Hardness for 30 Degree Press Brake Dies
We engineer every 30 degree forming press brake die to withstand heavy acute bending loads without sacrificing accuracy or structural integrity. For a deeper look at material performance under load, explore our press brake tooling material guide.
Metallurgy & Surface Treatment Specifications
- Certified Tool Steel Grades: Manufactured from high-tensile 42CrMo alloy steel and cold-work D2 equivalents to deliver exceptional yield strength and structural endurance.
- Dual-Zone Heat Treatment:
- Core Toughness (47–50 HRC): Through-hardened tool core absorbs shock and prevents catastrophic tool failure under maximum tonnage.
- Induction Hardened Edges (55–60 HRC): Deep induction hardening on high-wear V-shoulders keeps radius geometry sharp and minimizes friction wear over time.
- Anti-Galling Precision Finish: CNC ground working contact points featuring a surface roughness of Ra < 0.8 µm reduce sheet galling, lower bending friction, and prevent surface marking on stainless steel, aluminum, and pre-painted sheet metal.
Machine Clamping & Brand Compatibility for 30 Degree Press Brake Dies
Standard Clamping System Configurations
- American Precision Style: Manufactured with standard tang profiles and safety grooves for secure seating on traditional American-style press brake beds and die holders.
- European / Promecam Style: Features 13 mm standardized tangs and quick-change bottom rail alignment channels. Delivers rapid tool changes with tight self-centering tolerances.
- Wila Trumpf Style: Precision ground with hydraulic pin-and-groove self-seating profiles. Designed for high-speed automated clamping systems, ensuring full seating under hydraulic load. Learn more about our specialized Trumpf tooling compatibility options for high-precision setups.
Cross-Platform Brand Interoperability
Our 30 degree forming press brake die inventory is fully matched to factory specifications across top machinery brands:
| Press Brake Manufacturer | Supported Clamping Style | Alignment & Lock Method |
|---|---|---|
| Amada | European / Promecam / American | Quick-Change & Safety Pin |
| Trumpf & WILA | Wila NS / Hydraulic Pin | Self-Seating Pin & Groove |
| Bystronic | Beyeler / RF-A / European | Hydraulic Rail / Manual Clamping |
| Cincinnati | American Precision / Heavy Duty | Safety Tang & Bed Holder |
| LVD, Accurpress, Durma | Universal / European / American | Multi-System Rail Adapters |
We also supply custom-milled tang conversions and riser blocks, allowing you to run the same 30° bottom die across different press brake brands throughout your facility.
Acute Angle Press Brake Tooling Applications & Performance
Precision Enclosures & Return Bending
Acute bending profiles solve narrow clearance challenges when forming complex return flanges, deep channels, and tight seams.
Deep Return Flanges: Overcomes tool collision issues on narrow return bends.
Cabinet Housings: Streamlines frame construction for custom industrial control boxes and specialized electrical cabinets.
Compact Seams: Enables tight pre-bends required for seamless corner joints and interlocking panel assemblies.
Non-Marking Architectural & Stainless Steel Fabrication
Cosmetic surfaces require strict scratch prevention during high-angle bends. Combining our 30 degree press brake die configurations with non-marking urethane die insertion methods ensures flawless surface integrity.
Architectural Trim: Protects brushed, polished, and pre-painted metals from die lines and surface galling.
Specialty Metals: Delivers pristine surface protection during high-end stainless steel processing and architectural cladding production.
Eliminated Refinishing: Removes secondary grinding, polishing, and surface restoration costs.
Heavy Equipment Chassis & Thick Plate Acute Bending
Our heavy-duty bottom die 30 degree designs handle severe tonnage requirements when bending structural steel and heavy plate fabrications.
Structural Chassis Components: Forms acute structural channels for heavy machinery and transport trailers.
High Tonnage Resistance: Heavy-wall die construction prevents shoulder breakdown under extreme linear forces.
Thick Gauge Flexibility: Accommodates large-radius acute punches for thick plate air bending applications.
High-Tensile Springback Management
Springback control is essential when air bending high-strength sheet metals. Over-bending sheets down to an acute 30° angle provides the exact clearance needed to offset extreme material elasticity.
| Material Type | Yield Strength Range | Springback Allowance | Target Bent Angle |
|---|---|---|---|
| High-Tensile Steel (Hardox / Weldox) | 700 – 1100 MPa | 12° – 25° Over-bend | 45° / 60° / 90° |
| Stainless Steel (304 / 316) | 205 – 310 MPa | 3° – 6° Over-bend | 45° / 90° |
| Aluminum Alloys (5052 / 6061) | 193 – 290 MPa | 2° – 4° Over-bend | 45° / 90° |
Custom Engineering & 3D Bending Collision Simulation
We design and manufacture specialized custom press brake tooling tailored precisely to your production requirements. Every custom 30 degree forming press brake die is engineered to eliminate clearance bottlenecks, maintain exact profile tolerances, and prevent unwanted material deformation on complex part geometry.
Precision Die Modifications
- Tailored V-Widths & Heights: Customized V-opening widths, extended die heights, and narrow shoulder profiles built for deep channel bends or tight return flanges.
- Specialized Radius Grinding: Exact shoulder and bottom radii ground to minimize stress concentration and eliminate micro-cracking in high-tensile alloys.
- Relief Clearance Machining: Integrated relief clearance slots and step profiles machined directly into the die body to avoid collisions during multi-bend sequences.
CAD Evaluation & Virtual Bending Simulation
To guarantee flawless tool geometry before steel is cut, our team conducts complete custom tooling development using advanced virtual simulation software.
CAD File Analysis: Direct intake and evaluation of 2D DXF/DWG drawings and 3D STEP models.
Interference & Collision Detection: Virtual 3D simulation testing punch-to-die clearances, sheet metal travel, and machine ram movement to identify interference risk.
Springback Compensation: Precise angle calculations built directly into the 30 degree press brake die profile to compensate for material springback.
Rapid Prototyping to Factory-Direct Production
- Design Validation: Comprehensive 3D collision report and CAD confirmation within 24–48 hours.
- In-House Manufacturing: High-precision CNC wire EDM, core heat treatment, induction edge hardening, and surface grinding.
- Inspection: 100% optical CMM measurement and hardness testing before factory-direct dispatch.
Technical RFQ Checklist & Ordering Process for a 30 Degree Press Brake Die
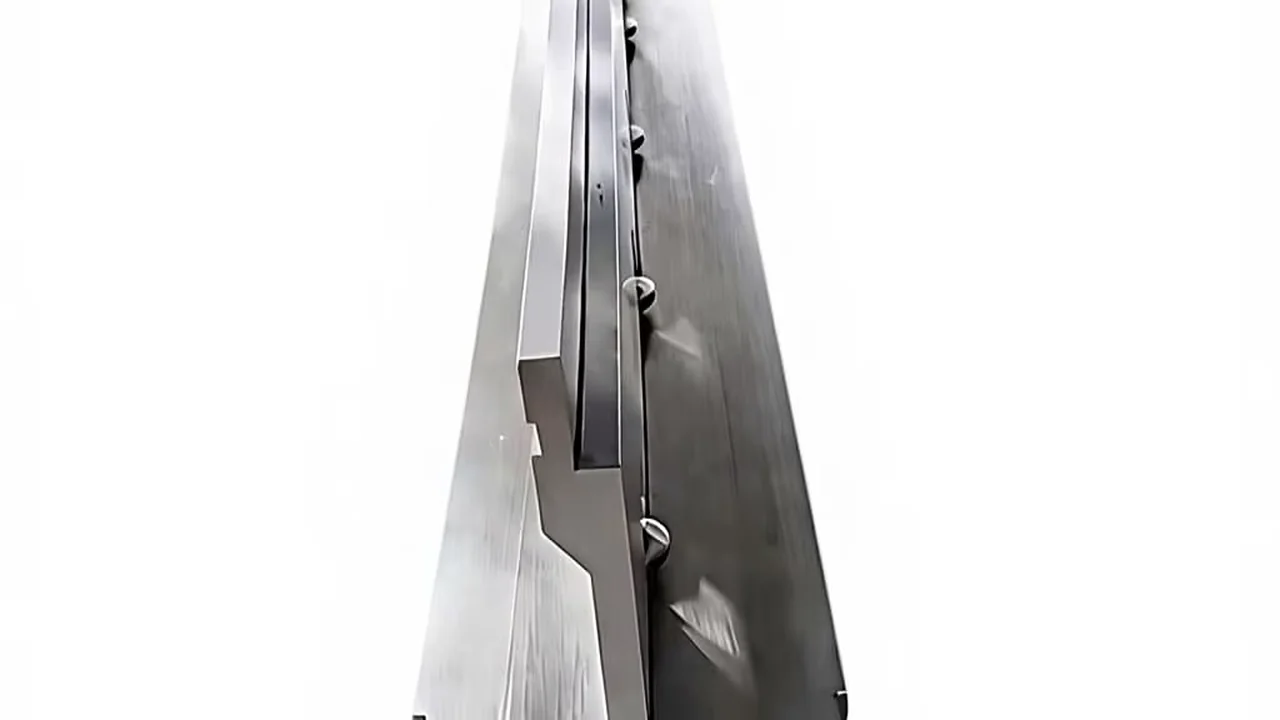
Following our detailed press brake die selection guidelines ensures your machine parameters perfectly match the selected tooling geometry.
Essential Technical Parameters for Quotes
| Technical Parameter | Information Required | Why It Matters |
|---|---|---|
| Workpiece Material | Material grade, yield, and tensile strength | Determines maximum tonnage limits and steel hardening requirements |
| Material Thickness | Minimum & maximum sheet thickness (mm/in) | Dictates necessary V-opening width and shoulder radii |
| Press Brake Model | Machine make, model, and total tonnage | Guarantees weight capacity limits and structural clearance |
| Clamping Style | American Precision, European, Wila/Trumpf | Ensures direct seating, safety groove alignment, and compatibility |
| Tool Length | Solid length or segmented set specs | Optimizes setup flexibility for complex cabinet or channel bends |
We analyze each parameter to verify that every 30 degree forming press brake die meets your specific bending tonnage and clearance requirements. If you require specialized acute bottom tooling, explore our precision female press brake V-die options to match your production needs.
Quality Assurance & Inspection Standards
We back every tool with strict in-house quality control procedures before shipment:
- 100% CMM Optical Inspection: Every die profile undergoes 3D Coordinate Measuring Machine scanning to guarantee angular precision (30° ± 0.5°) and profile tolerances within ±0.01 mm.
- Hardness Verification: Surface hardness testing verifies core toughness (47–50 HRC) and deep induction-hardened wear zones (55–60 HRC) along the entire working length.
- Material Traceability: Certified mill test reports (MTR) and dimensional inspection certificates are included with every order.
Technical FAQs for 30 Degree Press Brake Dies
How to Select the Proper V-Opening for a 30 Degree Acute Die?
Selecting the correct V-opening for a 30 degree press brake die requires accounting for deeper punch penetration during acute air bending. While standard 90° air bending typically uses an 8x sheet thickness rule, 30° acute bending demands a wider V-opening to accommodate punch clearance and prevent sheet binding against the die shoulders.
| Material Thickness | Recommended V-Opening | Minimum Flange Length |
|---|---|---|
| 0.8 mm – 1.2 mm | 8 mm – 10 mm | 5.5 mm |
| 1.5 mm – 2.0 mm | 12 mm – 16 mm | 9.0 mm |
| 2.5 mm – 3.0 mm | 20 mm – 25 mm | 14.0 mm |
| 4.0 mm – 6.0 mm | 32 mm – 50 mm | 28.0 mm |
For high-tensile materials with significant springback, we recommend stepping up to the next wider V-opening to reduce required bending tonnage and safeguard working edges.
Can a 30-Degree Press Brake Die Form Standard 90-Degree Bends?
Yes. In air bending operations, a 30 degree forming press brake die offers exceptional process flexibility. Because the sheet metal only makes contact with the two ground shoulder radii of the die, you can air bend any angle from 30° up to 179°, including standard 90° bends.
However, bottoming or coining a 90° bend inside a 30° acute die profile is not possible. If your production line transitions directly from acute pre-bending to flattened seams, explore our specialized hemming dies to streamline your two-stage bending process.
How Is Die Accuracy Guaranteed Over Long Tool Lengths?
We ensure precise linear accuracy across full-length rails and sectional sets through strict CNC manufacturing protocols:
- Precision Surface Grinding: Critical working edges and seating bases are CNC precision ground to profile tolerances within ±0.01 mm per meter.
- Matched Sectional Sets: Standard segmented sets (such as 835 mm or 415 mm split tooling) undergo matched-set grinding to guarantee seamless height alignment across extended bed lengths.
- 100% CMM Verification: Every tool undergoes Coordinate Measuring Machine (CMM) dimensional checks and laser profile inspection prior to shipment.
- Dual-Zone Heat Treatment: High-grade 42CrMo alloy steel cores (47–50 HRC) are paired with deep induction hardened working zones (55–60 HRC) to stop long-term wear and angular deviation.
What Is the Lead Time for Standard vs. Custom Segmented 30° Dies?
Lead times depend on profile complexity, clamping configuration, and stock availability:
| Tooling Type | Standard Stocked Specifications | Average Lead Time |
|---|---|---|
| Standard Stock Sets | 835 mm, 415 mm, or pre-segmented sets (Amada, Promecam, Wila styles) | Ships within 24 to 48 hours |
| Custom V-Width / Height | Custom V-openings, altered heights, or ground shoulder radii | 10 to 15 business days |
| Engineered Custom Sets | Specialized sectional cuts, non-marking urethane pockets, heavy-duty geometries | 15 to 20 business days |
Our technical team provides 2D DXF/DWG layouts and 3D STEP models within 24 hours for custom orders, allowing virtual press brake collision verification before machining begins.



