

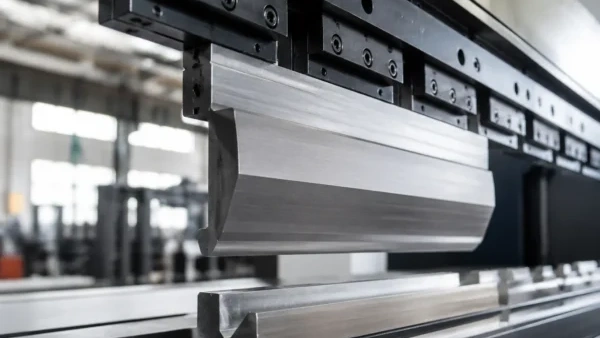
Formula details
Product Details
Overview
24 Press Brake Die: Product Overview & Engineering Features
Core Engineering Highlights
- Rotational 4-Way Efficiency: Rapidly switch between 4 distinct V-openings to bend material ranging from 16 gauge sheet metal to 1/4" plate steel on a single multi-V press brake die block.
- Industrial Durability: Precision-machined from heavy-duty AISI 4140 steel with induction-hardened working surfaces (50–55 HRC) to prevent deformation under high tonnage and maintain zero-deflection accuracy.
- Universal Compatibility: Features a standard press brake tang for traditional machines while serving as a reliable shop press brake attachment for hydraulic H-frame setups.
- Corrosion Protection: Finished with a durable black oxide coating to resist shop rust, friction wear, and surface degradation.
Quick Specifications
| Feature | Engineering Specification |
|---|---|
| Die Length | 24 Inch (610 mm) |
| Material Grade | Premium AISI 4140 Alloy Tool Steel |
| Surface Hardness | Working Surfaces Induction-Hardened to 50–55 HRC |
| Bending Capacity | 16 Gauge Sheet Metal to 1/4" Plate |
| Die Configuration | Rotational 4-Way Bottom V-Die |
| Finish | Industrial Black Oxide |
24 Press Brake Die Technical Specifications & Tonnage Matrix
Material Thickness & Tonnage Reference Chart
Our comprehensive press brake V-die chart and tonnage guide outlines baseline requirements for 90° air bending mild steel (60 ksi / 400 MPa tensile strength) on a 1-foot basis:
| Material Thickness | Recommended V-Opening | Inside Bend Radius (IR) | Tonnage Required (Tons / Ft) |
|---|---|---|---|
| 16 Gauge (0.060" / 1.5 mm) | 0.500" (12.7 mm) | 0.080" (2.0 mm) | 1.5 Tons |
| 12 Gauge (0.105" / 2.7 mm) | 0.875" (22.2 mm) | 0.140" (3.5 mm) | 4.0 Tons |
| 10 Gauge (0.135" / 3.5 mm) | 1.125" (28.5 mm) | 0.180" (4.5 mm) | 6.5 Tons |
| 1/4" Plate (0.250" / 6.35 mm) | 2.000" (50.8 mm) | 0.330" (8.4 mm) | 15.5 Tons |
- Stainless Steel: Multiply standard tonnage requirement by 1.5x.
- Aluminum (Soft Alloys): Multiply standard tonnage requirement by 0.5x.
Precision Inside Radius Calculation
To calculate exact sheet metal tolerances before cycling your machine, apply these industry formulas:
- V-Opening Selection: V = 8 x Material Thickness (T)
- Inside Radius (Air Bending): IR = 0.15 to 0.16 x V-Opening Width
Matching your workpieces to these parameters protects your sheet metal bending die 24" block against premature center deflection and overload. If your operations require dedicated single-purpose setups, you can pair this unit alongside a specialized female press brake V-die for precise sheet metal bending to expand overall shop capability.
Dimensional Schematics for 24 Press Brake Die
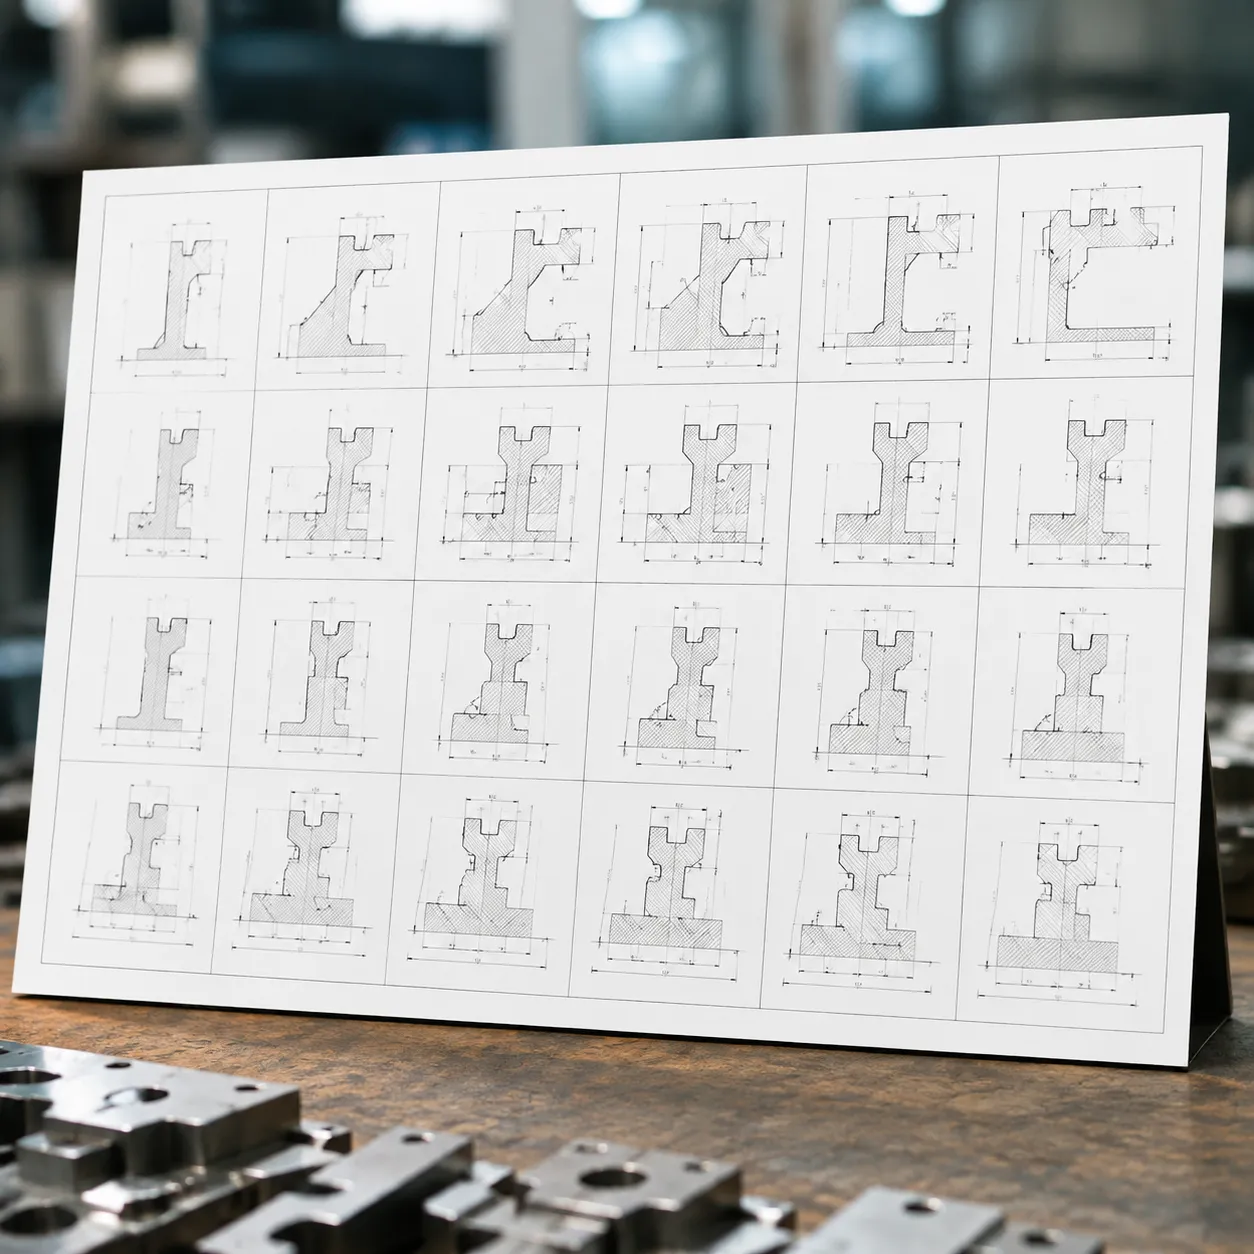
Technical CAD Callouts & Geometric Specifications
| Feature / Metric | Dimensional Callout | Engineering Purpose |
|---|---|---|
| Tang/Shank Style | Standard 0.500" x 0.625" American Style | Ensures drop-in compatibility with standard clamping systems |
| Safety Retention Groove | Full-length machined detent | Prevents accidental die drop during tool seating and rotation |
| V-Centerline Offset | ± 0.0008" true position alignment | Maintains absolute center alignment across all 4 V-openings |
| Shoulder Radius ($R_s$) | Precision-ground entry radii | Reduces sheet metal friction, wear, and surface marring |
| Relief Clearance Angle | 85° / 90° profile clearances | Delivers full bend clearance without web collision during air bending |
Cross-Sectional Engineering Details
- Centerline Alignment: Each V-opening centerline is indexed directly to the mounting tang. You can flip between 4 distinct V-grooves without re-centering your back gauge or adjusting machine offsets.
- Shoulder & Clearance Optimization: Smooth entry radii prevent galling on aluminum and stainless steel while allowing clean 90° air bending on structural carbon steel.
- Integrated Safety Grooves: Machined detents ensure positive lockup in press brake safety clamps and custom bottom die holders.
For detailed cross-sectional CAD models or custom shank configurations, consult our engineering technical support team for full DXF and STEP drawing files.
Workpiece Compatibility & Application Scenarios for the 24 Press Brake Die
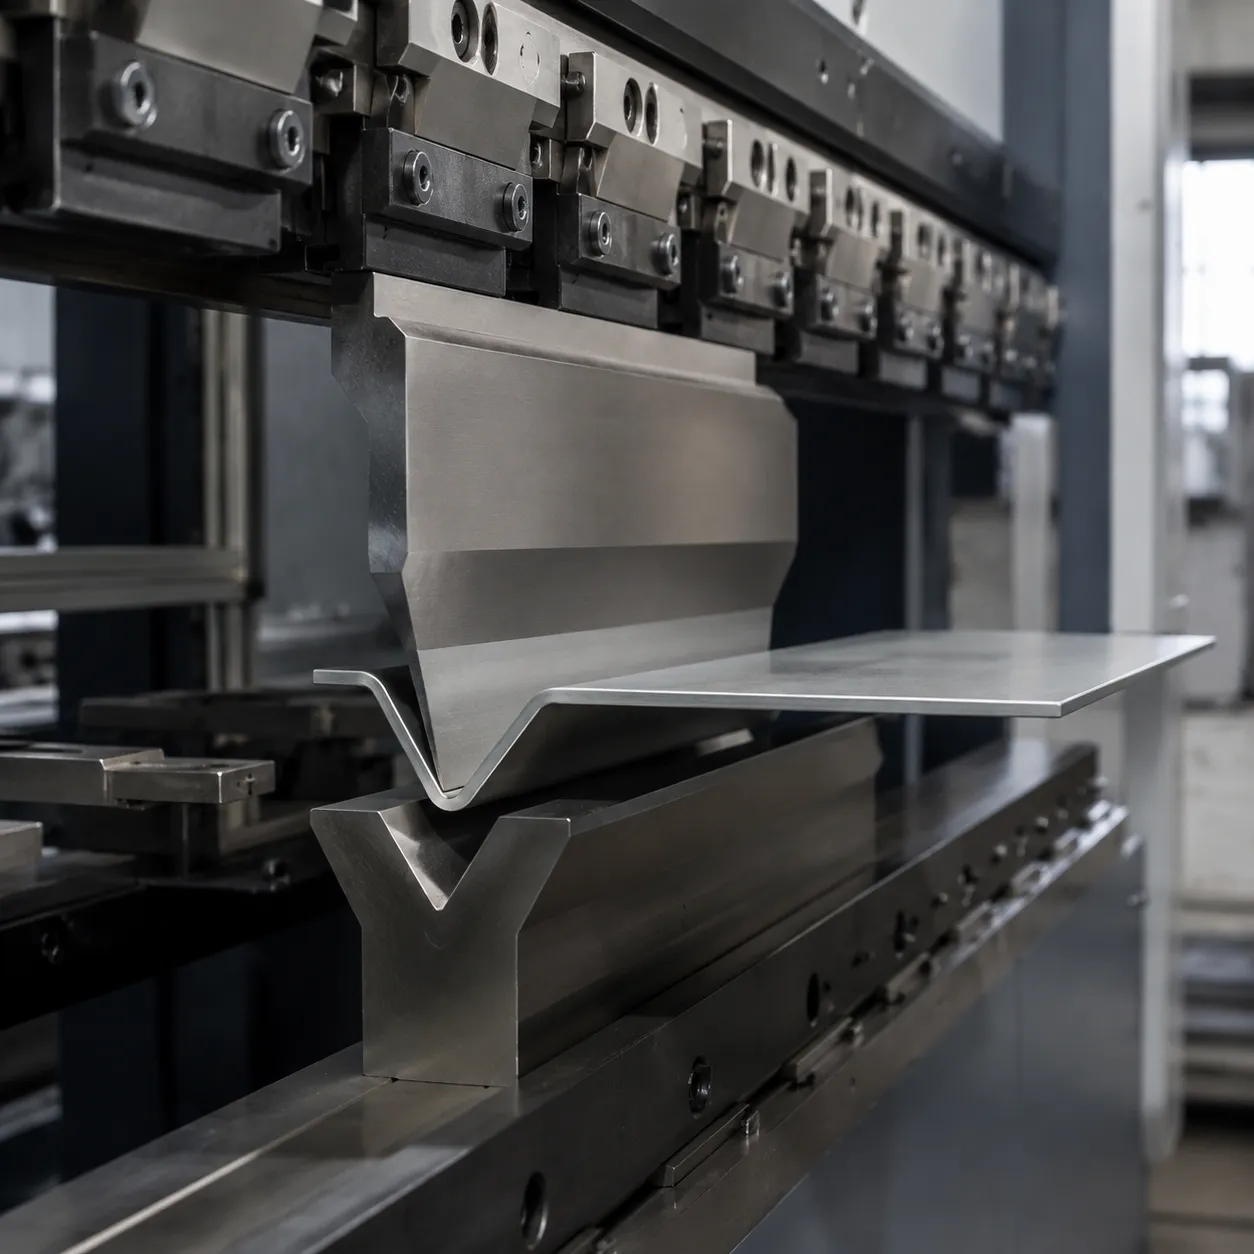
Mild Steel & Carbon Steel
- Air Bending & Bottoming: Handles sheet thicknesses from 16 gauge up to 1/4" carbon steel plate reliably.
- Tonnage Resistance: Maintains tight tolerances during high-tonnage bottoming runs without cracking or permanent deformation.
Stainless Steel & Aluminum Guidance
- Prevent Surface Galling: When forming aluminum or polished stainless steel, we recommend placing protective non-marring urethane film over the 4-way V-openings to eliminate metal pickup and die marking.
- Precision Clean Bends: Crucial for critical cosmetic components in stainless steel processing where post-bend grinding or polishing adds unnecessary labor costs.
Essential Fabrication Use Cases
Our 24 inch press brake tooling excels across a broad spectrum of general sheet metal fabrication work:
- Electrical Enclosures & Cabinets: Precise 90° bends for seamless corner fitment and tight sealing surfaces.
- Heavy-Duty Brackets & Mounting Hardware: Consistent, repeatable bend radii in structural carbon steel.
- Pans, Trays & U-Channels: Easy repositioning allows rapid multi-bend sequences on complex sheet profiles.
- Structural Sheet Components: High beam strength ensures zero-deflection accuracy across the entire 24" bed width.
Installing and Aligning Your 24 Press Brake Die
Proper setup guarantees repeatable bend angles and prevents permanent tool deformation. We built our 24 press brake die to seat cleanly into standard lower bed holders or press brake clamping systems. Follow this sequence for precise centerline alignment:
- Clean the Bed and Ram: Wipe down the bed rail and upper ram surface to clear away mill scale, metal shavings, and shop debris.
- Position the Multi-V Block: Seat the 24 inch press brake tooling on the lower bed holder with your selected V-opening facing directly upward.
- Align Centerline Under Power: Bring down your upper tooling—such as standard punches or deep-relief gooseneck punches—at low jog speed until the punch tip rests centered in the V-groove.
- Lock Clamping Hardware: Tighten bed set screws evenly from the center working outward to hold the 4-way bottom V-die perfectly parallel to the ram.
Tonnage Safety Rules & Load Limits
Never exceed maximum load thresholds. Concentrating high tonnage into narrow V-openings can split lower tooling or deform working shoulders.
| V-Opening Width | Recommended Max Gauge (Mild Steel) | Safe Limit Per Foot | Safe Limit Across Full 24" Length |
|---|---|---|---|
| 0.25" V-Groove | 16 Gauge (0.060") | 6.5 Tons/ft | 13 Tons |
| 0.50" V-Groove | 11 Gauge (0.120") | 12 Tons/ft | 24 Tons |
| 0.875" V-Groove | 3/16" Plate (0.187") | 18 Tons/ft | 36 Tons |
| 1.50" V-Groove | 1/4" Plate (0.250") | 22 Tons/ft | 44 Tons |
When running narrow air-bending profiles or acute punches, re-calculate tonnage requirements to eliminate side-thrust loads on the die shoulder.
Storage & Maintenance Schedule
Keep your 4140 hardened tool steel die performing accurately with a consistent shop maintenance routine:
- Post-Shift Cleaning: Blow out embedded mill scale and carbon dust using compressed air, then wipe the V-openings clean with solvent.
- Shoulder Lubrication: Apply a light coat of anti-wear machine oil or rust preventative along precision-ground shoulders to reduce friction during heavy cycle runs.
- Horizontal Storage: Store your sheet metal bending die 24" horizontally on wooden or polyurethane-padded rack surfaces to protect ground edges from impact damage and maintain optical straightness.
Recommended Tooling & System Integration for the 24 Press Brake Die
24" 90° Standard Punch & Gooseneck Top Punch
To get maximum utility from a 24 inch press brake tooling setup, matching your top punch profile to your target bend shapes is critical:
- 90° Standard Straight Punch: Built for standard air bending, heavy plate forming, and general sheet metal fabrication where clearance around the ram is non-restricted.
- Gooseneck Top Punch: Essential for clearing return flanges, deep channels, and four-sided pan enclosures without workpiece collision.
Proper punch selection prevents uneven pressure points across the die bed, protecting both the upper punch tip and the lower multi-V surfaces. When expanding your setup, reviewing our resource on how to choose press brake tools will help you match punch tip radiuses and tonnage limits directly to your material thickness.
Hydraulic Shop Press Adapter Bracket Set
We designed our hydraulic press brake tooling 24 inch series to bridge the gap between dedicated CNC press brakes and standard H-frame equipment:
- Universal Mounting Brackets: Allow quick, secure installation onto standard 12-ton, 20-ton, and 50-ton H-frame shop presses.
- Self-Centering Base Plates: Lock the bottom 24 press brake die directly along the press centerline, eliminating side-load risks during high-tonnage forming.
Back Gauge Systems & Magnetic Alignment Guides
Repeatability relies on precise workpiece positioning before the top punch makes contact with the sheet:
- Manual & CNC Back Gauges: Deliver accurate stop locations down to ±0.002", accelerating multi-step bracket and channel bending.
- Magnetic Alignment Guides: Snap directly onto the shoulder of our multi-V dies for quick, rock-steady depth indexing on small or narrow sheet metal parts.
24 Press Brake Die FAQs
Can the 24" press brake die be used on a standard 20-ton H-frame shop press?
Yes. When paired with an adapter bracket set, this 24 press brake die mounts directly into standard 20-ton or 50-ton hydraulic H-frame shop presses. Ensure your press bed provides even support across the full 24-inch length and that your ram stays centered over the tool centerline to prevent off-center loading.
How do I select the right V-opening for my metal thickness?
Follow the standard 8x rule for air bending mild steel: choose a V-opening equal to 8 times the material thickness (V = 8 × T).
16-gauge sheet metal (0.060"): Use a 1/2" V-opening.
1/8" plate (0.125"): Use a 1" V-opening.
1/4" plate (0.250"): Use a 2" V-opening.
Our 4-way press brake die with high-strength multiple V-openings allows you to rotate between four standard V-widths in seconds without unbolting the tool block.
Is this die suitable for bottoming or only air bending?
We build this die primarily for precision air bending, which requires significantly less tonnage and increases tooling lifespan. However, because we induction-harden the working surfaces of our 4140 tool steel, it handles bottoming on lighter gauge sheet metal (16-gauge to 11-gauge). Always double-check your tonnage-per-foot calculations before bottoming heavy plate to stay within safe working load limits. For other bending operations and setups, explore our complete line of metal-forming press brake dies for sale.



