

Formula details
Product Details
Overview
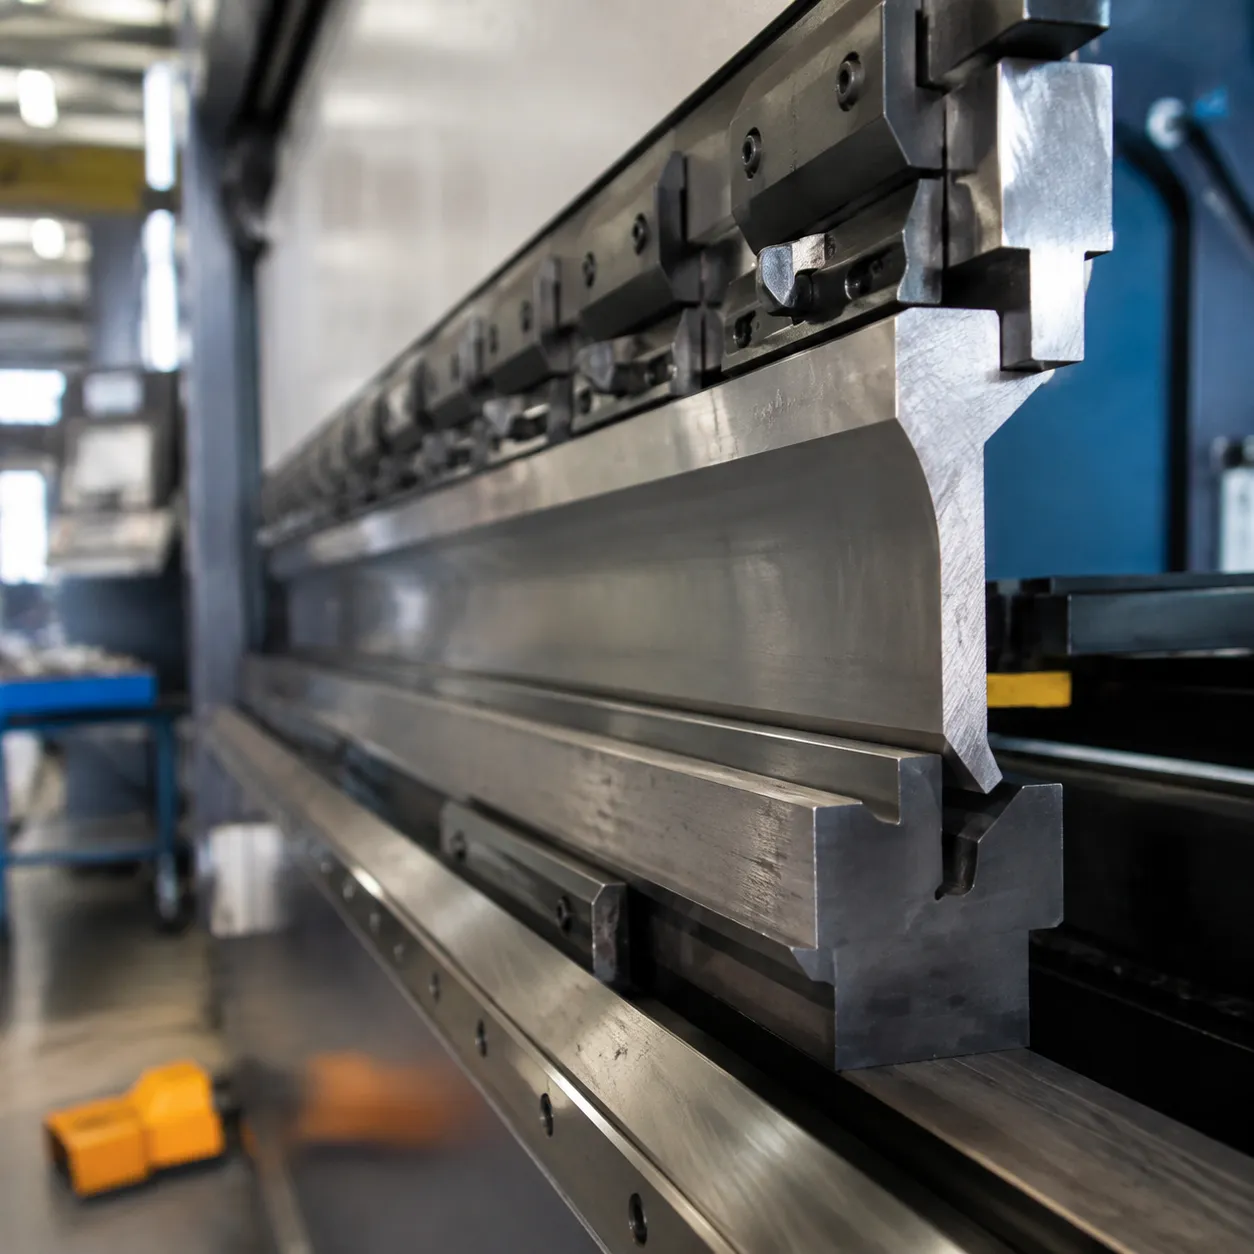
50 Ton Press Brake Die
| Feature / Metric | Engineering Specification | Shop Floor Advantage |
|---|---|---|
| Bending Capacity | Matched for 50-ton tonnage limits | Prevents tool deformation and structural fatigue |
| Edge Hardness | HRC 55–60 (Deep Induction Hardened) | Extends service life on high-cycle production runs |
| Mounting Compatibility | European Precision & American Standard | Cuts setup downtime and eliminates adaptor costs |
| Surface Finish | CNC Precision Ground (Ra < 0.8 µm) | Eliminates tool-marking on stainless and aluminum |
Built for Extended Service Life and Rapid Setups
Our 50 ton bending die line addresses daily wear-and-tear while keeping changeover times to a minimum.
- Deep Edge Hardening: Thermal induction treatment along the working radius resists grooving and galling when processing hard alloys or scale-heavy stock.
- Dual Ram Compatibility: Fits directly into standard press brake die holder slots and safety-tang systems, simplifying tool replacement across your fleet.
- Precision Angle Consistency: Tight manufacturing tolerances ensure angular accuracy across short sections and full-length bed setups.
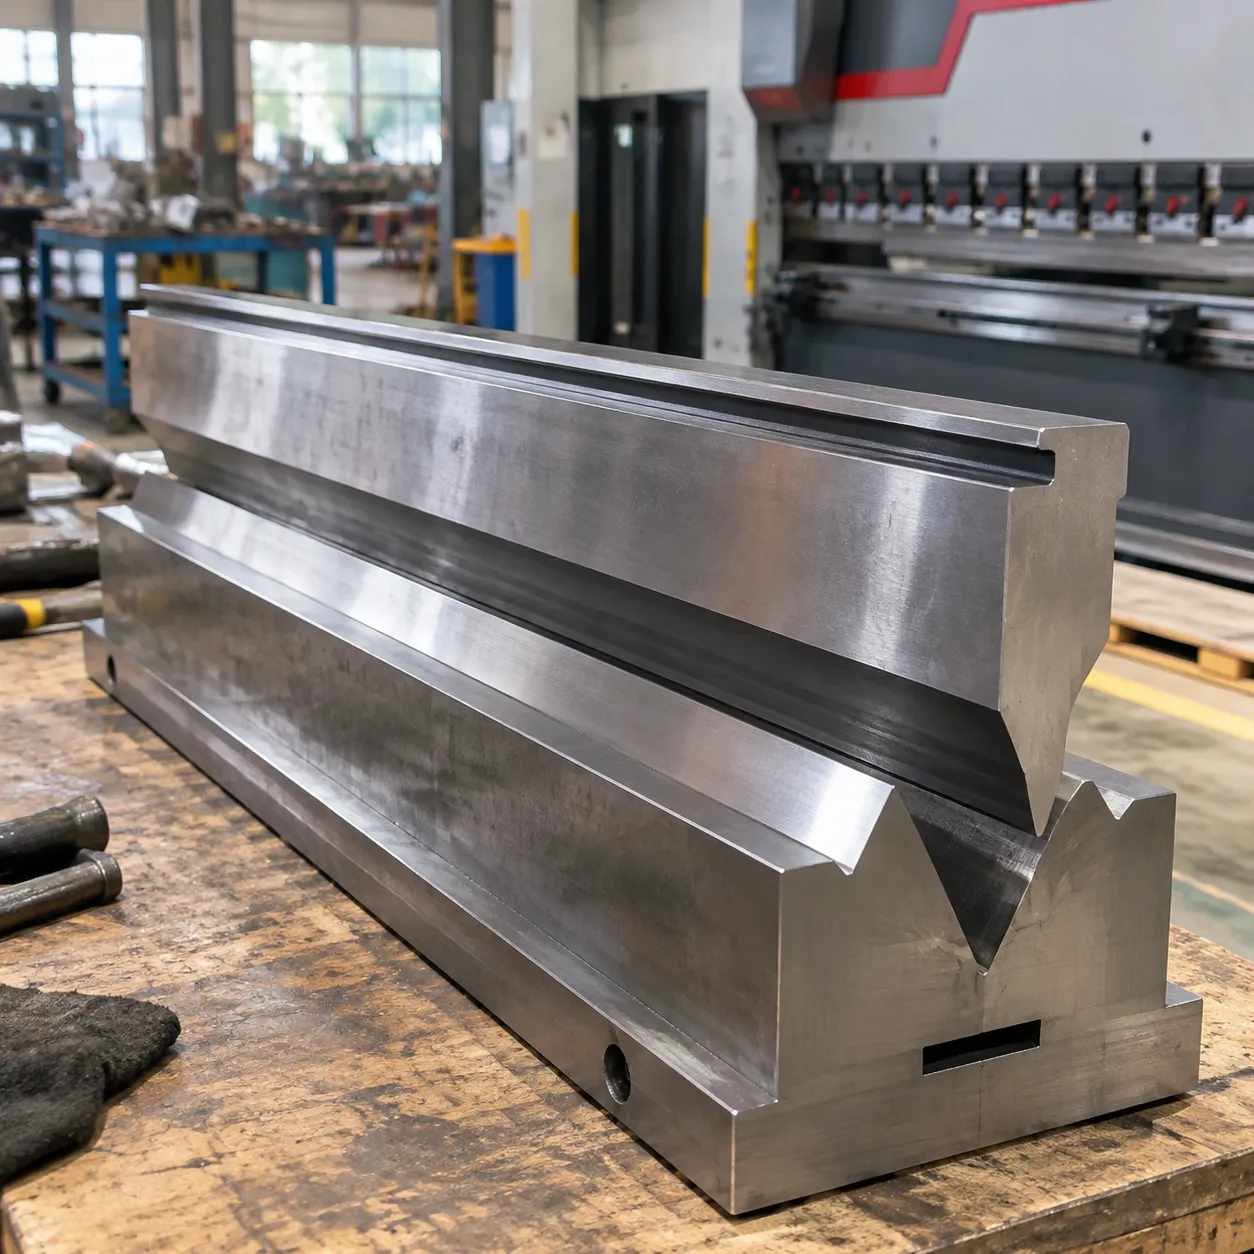
50 Ton Press Brake Die Specifications
| Feature | Specification |
|---|---|
| Steel Grade | Certified 42CrMo / 4140 alloy steel (1045, D2, or custom alloy options) |
| Working Edge Hardness | HRC 55–60 (deep induction hardened) |
| Core Hardness | HRC 28–32 (shock-absorbing core) |
| Precision Tolerances | CNC precision ground to ±0.01 mm |
| Surface Finish | Ra < 0.8 µm standard (down to Ra 0.4 µm for delicate alloys) |
| Standard Lengths | 415 mm, 835 mm, sectionalized sets, and full-bed single-piece options |
Material Performance & Engineering Specs
- Certified Tool Steel: Standardizing on 42CrMo (4140) alloy tool steel provides maximum fatigue resistance under repeated 50-ton loads.
- Dual Hardness Profile: Deep induction hardening along the working edge (HRC 55–60) resists edge wear and pitting, while the softer HRC 28–32 core absorbs high mechanical impact.
- Tight CNC Grinding: Machined to a ±0.01 mm grinding tolerance to ensure seamless height matching across sectionalized die sets.
- Tailored Options: For unique profiles, custom lengths, or non-standard ram setups, explore our specialized custom press brake tooling engineered for specific shop applications.
50 Ton Press Brake Die Types & Configurations
We manufacture every 50 ton press brake die to match specific shop-floor bending operations, balancing tonnage limits with maximum bend accuracy.
| Tooling Configuration | Opening / Specs | Primary Application | Key Advantage |
|---|---|---|---|
| Single & Double V Dies | Precision ground, 88° / 90° / Acute | Standard sheet metal air bending | High angular precision & fast alignment |
| 4-Way Multi-V Die Blocks | 6 mm to 100 mm indexable V-grooves | Multi-thickness plate processing | Zero downtime tool changes via block rotation |
| Hemming & Combination Dies | Spring-loaded or fixed 30° sharp | Edge reinforcement & seam flattening | 2-in-1 stage bending in a single setup |
| No-Mar / Mark-Free Inserts | Polyurethane / Synthetic inserts | Polished, aluminum, and painted stock | 100% elimination of surface scoring under load |
Single V and Double V Bottom Dies
We engineer high-precision single V and double V bottom die profiles for exact 88°, 90°, and acute angle bends. Designed for standard hydraulic press brake tooling setups, these dies deliver tight radii on mild steel, stainless, and aluminum without deflection.
4-Way Multi-V Die Blocks
Our indexable 4-way multi-v die block options pack V-groove openings from 6 mm up to 100 mm onto a single square tool. Flip the block directly on your bottom die press brake bed to jump between different sheet thicknesses without stopping production to swap tooling.
2-in-1 Hemming and Combination Dies
We combine stage pre-bending and final seam flattening into a unified tooling setup. Utilizing a 30-degree press brake die for air bending and hemming lets your operator run stage-bend hems in one quick press stroke to maximize throughput on light-gauge parts.
No-Mar Inserts for Scratch-Free Bending
To prevent die lines and surface marring on architectural aluminum, stainless, or pre-painted stock, we equip our 50 ton bending die options with heavy-duty polyurethane and synthetic contact pads. Swapping standard steel edges for a plastic press brake die for non-marking bending preserves cosmetic finishes even when bending near maximum press force limits.
Tooling Selection & Tonnage Guidelines
Properly matching sheet metal thickness to the correct V-groove is critical to protect your equipment and achieve consistent bend angles. When we set up a 50 ton press brake die, staying safely within the machine's rated pressure limits prevents permanent tool deformation and frame deflection.
V-Groove Calculation Formula
For standard air bending on mild steel, we rely on the industry-standard 8x rule to keep tonnage manageable across every run:
- Formula: V = 8 x t (where V is the V-opening width and t is the sheet metal thickness).
- Tonnage Safety: Narrowing the V-groove increases required bending force exponentially. For precise tonnage limits on various sheet metal gauges, consult our press brake V-die chart and tonnage guide.
Inside Radius & Springback Compensation
Material springback causes bends to open up after load release. We offset this elastic recovery through precise die angle selection and punch tip matching:
- Inside Radius Estimate: Ri = V / 6
- Die Angle Selection: We recommend 88° or 85° bottom die press brake tooling for standard air bending overbend, and 30° acute V-dies for high-springback materials like stainless steel. Refer to our press brake die angles guide for springback selection to match your specific sheet alloy.
Tang Styles & Machine Fitment
We manufacture our hydraulic press brake tooling in two industry-standard tang configurations to fit your machine's clamping setup:
- European Precision Style: Features quick vertical self-seating safety tangs for rapid, drop-in tool changes and automatic alignment.
- American Standard Style: Utilizes center-line safety tangs designed for traditional side-loading press brake die holder setups and manual clamping bars.
Precision Manufacturing & Quality Control Protocol
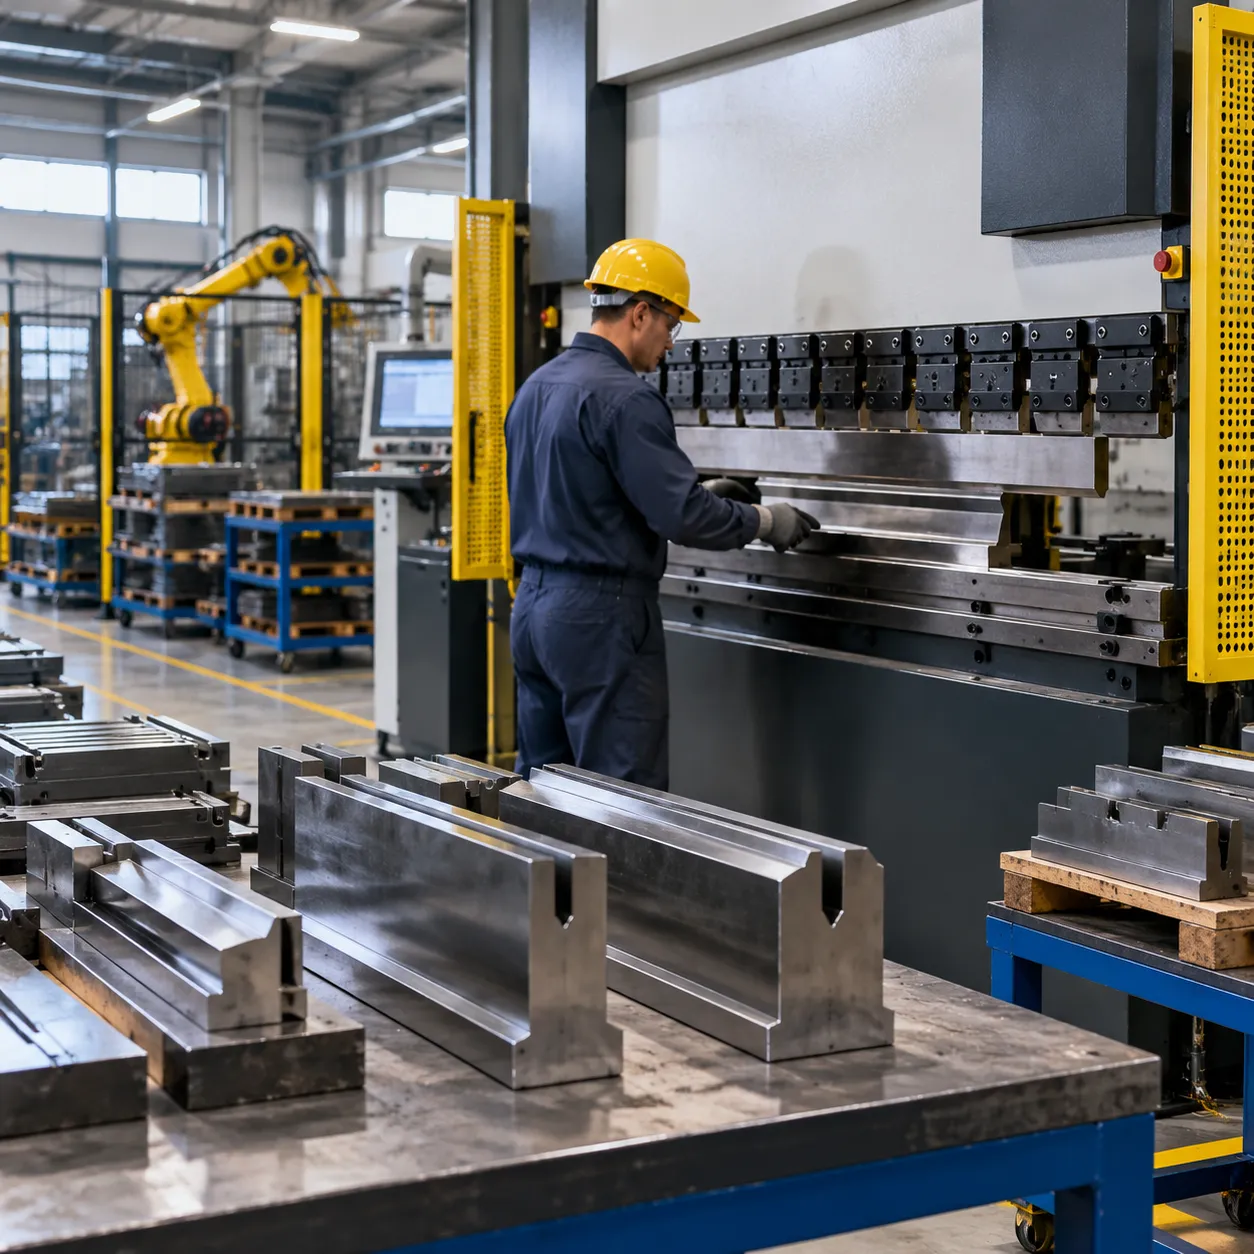
Deep Induction Hardening Process
We subject every 50 ton press brake die to controlled thermal stress relief prior to deep induction hardening. Hardening the working edges to HRC 55–60 while preserving a ductile HRC 28–32 core prevents micro-cracking under cyclic loads and stops premature edge wear during high-volume forming.
CNC Surface Grinding for High Precision
Our precision ground dies undergo full-length CNC surface grinding post-heat treatment. This process guarantees angular consistency and tolerances within ±0.01 mm across the entire working length, eliminating bend angle variation and tedious shimming during setup.
Quality Inspection & Dimensional Testing
We maintain strict press brake tooling specifications through a rigorous quality control inspection protocol on every finished piece:
- 100% CMM Testing: Coordinate measuring machines verify precise V-groove angles, tang geometry, and shoulder radii.
- Straightness Verification: Optical alignment tests ensure zero axial warp or twist across sectionalized or full-length units.
- Surface Finish Auditing: Profilometers verify surface roughness down to Ra < 0.8 µm (Ra 0.4 µm for sensitive non-marking tooling) to protect sheet metal bending tools and workpieces from friction galling.
Frequently Asked Questions on 50 Ton Press Brake Dies
How do I calculate the proper V-groove opening for a 50-ton press brake die?
We use the standard 8x rule for mild steel sheet metal bending. Match your material thickness to the V-groove opening using these guidelines to stay well within your 50 ton press brake die pressure limits:
| Material Type | Recommended V-Opening Formula | Inside Radius (Ri) |
|---|---|---|
| Mild Steel | V = 8 x material thickness (t) | Ri = V / 6 |
| Stainless Steel | V = 10 x material thickness (t) | Ri = V / 5 |
| Aluminum | V = 6 x material thickness (t) | Ri = V / 6 |
Exceeding these ratios drastically increases tonnage demand and risks overloading both the tooling and press ram.
What is the difference between European style and American standard press brake tooling?
The primary differences center on tang profile, precision clamping, and alignment mechanisms:
- European Precision Style: Uses a 13 mm safety tang with automatic vertical self-seating. It offers tight tolerances (+/-0.01 mm) for quick-change tool setups.
- American Standard Style: Features a traditional center-line tang clamped horizontally from the side.
We build both American and European press brake tooling to ensure seamless integration with your press brake ram and die holder.
How can I prevent sheet metal marking and scratching when using a 50-ton bending die?
Prevent cosmetic damage on aluminum, stainless, or pre-painted sheet metal with three effective shop-floor strategies:
- Polyurethane Inserts: Place synthetic no-mar pads directly inside the bottom die V-groove.
- Protective Bending Tape: Lay heavy-duty elastomer film across the die shoulders before forming.
- Large Shoulder Radii: Use CNC precision-ground dies with enlarged, polished shoulder radii to eliminate material galling under load.
What steel grade and HRC hardness offer the longest service life for 50-ton tooling?
We manufacture long-life 50 ton press brake die sets using premium 42CrMo (4140) alloy tool steel.
- Working Edges: Deep induction-hardened to HRC 55–60 to resist severe wear, abrasion, and edge chipping.
- Die Core: Heat-treated to HRC 28–32 to maintain high impact toughness and prevent brittle structural failure under full load.



