

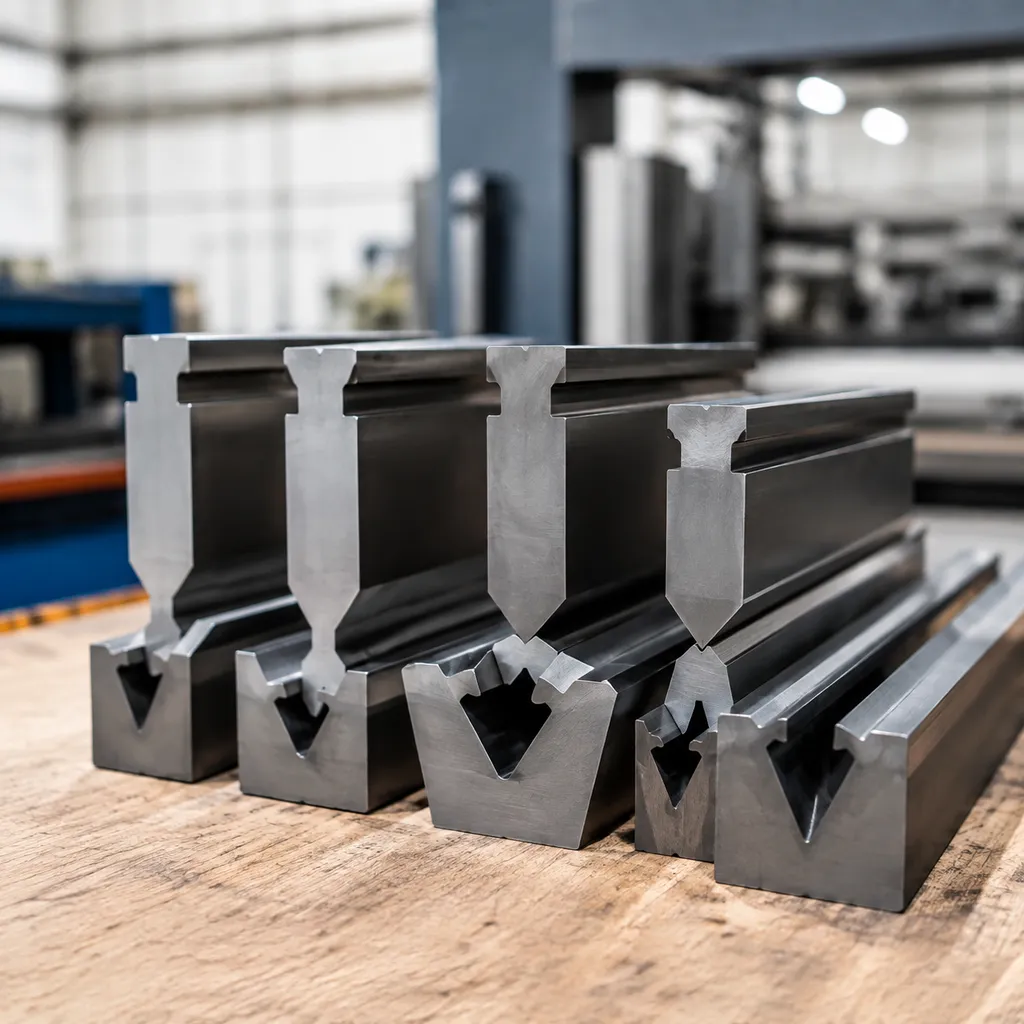
Formula details
Product Details
Overview
Precision Ground Press Brake Tooling Capabilities
Engineered for demanding sheet metal bending applications, our punches and dies deliver exact repeatability, minimal wear, and seamless integration into existing r k press brake die inc setups.
Key Performance Metrics
- Grinding Precision: Profile and height grinding tolerances held to ±0.01 mm for accurate multi-segment alignment.
- Hardness Profile: HRC 55–60 deep induction hardening on critical working contact points, supported by a ductile HRC 47–50 base hardness for impact resistance.
- Operational Longevity: Up to 3x operational service life compared to standard press brake tooling.
Technical Specifications & Metallurgical Standards
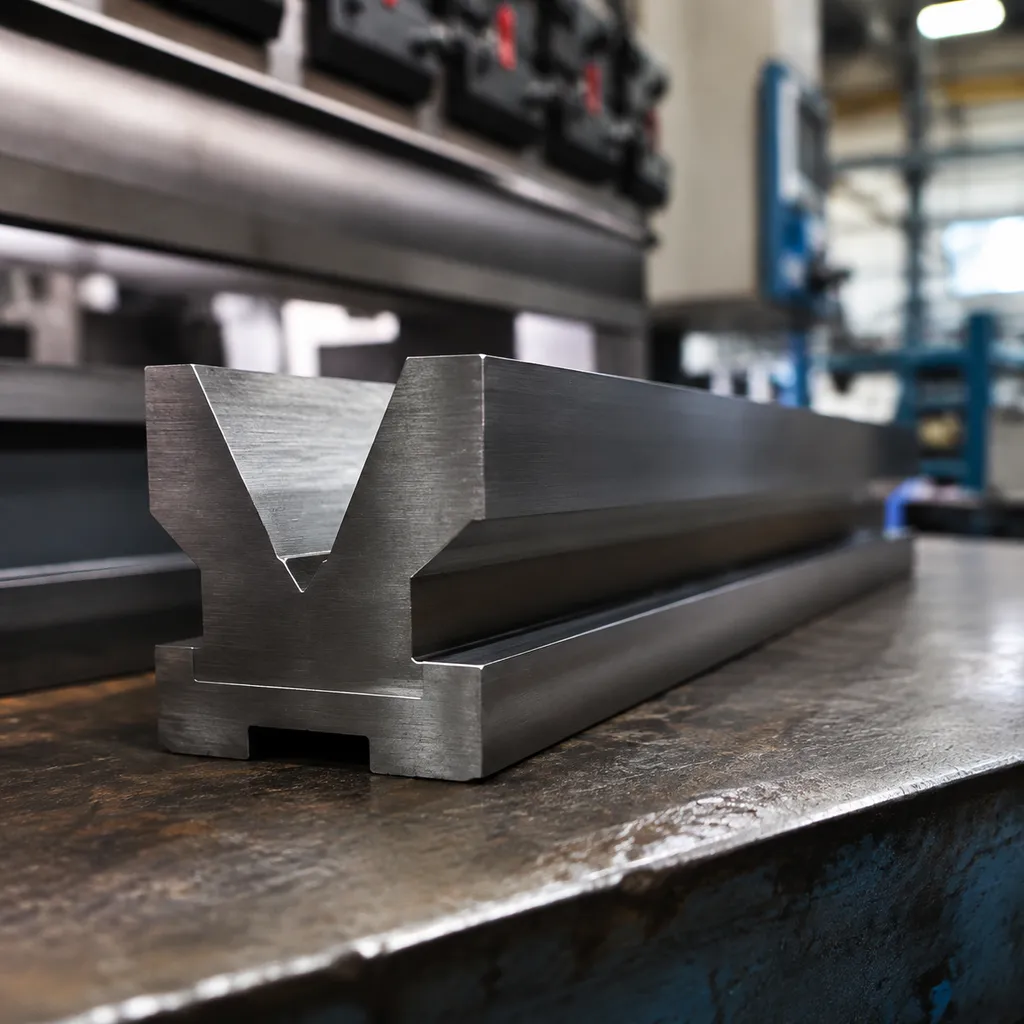
We manufacture precision ground press brake tooling designed to meet or exceed R-K Press Brake Die Inc. performance benchmarks. Our high-hardness alloy tooling utilizes certified alloy steel stock to withstand extreme tonnage and high-cycle sheet metal fabrication without structural deformation.
Steel Material Grades & Surface Engineering
We verify every raw material heat lot using spectrometric chemical analysis prior to machining. This guarantees consistent grain structure, high tensile strength, and superior wear resistance under repeated impact loading.
| Engineering Parameter | Standard Specification |
|---|---|
| Alloy Composition | High-grade certified 42CrMo, 42CrMo4, and Cr12MoV alloy tool steel |
| Chemical Analysis | Spectrometric verification per raw material heat lot |
| Surface Finish | Profilometer-tested finish at Ra < 0.8 µm to eliminate friction |
| Traceability | Permanent laser-etched batch codes and material certificates |
Quality Assurance & Inspection Protocol
We execute a rigorous four-stage quality assurance protocol across all production runs to ensure tight profile accuracy for our sheet metal bending dies:
- Raw Material Spectro-Verification: Confirms chemical alloy purity before entering the CNC machining process.
- Rockwell Hardness Depth Testing: Verifies deep induction hardness (HRC 55–60) on working contact zones while maintaining a core toughness of HRC 47–50.
- CMM & Optical Inspection: Coordinate Measuring Machine (CMM) and optical projection checks ensure critical profile height and angle tolerances stay within ±0.01 mm.
- Surface Quality Control: Low-friction surface finishing (Ra < 0.8 µm) prevents tool drag, work-piece galling, and cosmetic surface marking on stainless or aluminum sheet stock.
- Laser Batch Traceability: Individual tool tracking numbers are laser-engraved for material certification verification and seamless replacement ordering.
Tooling Classification & Geometry Taxonomy
Press Brake Punches
- Acute Angle Punches (30°, 45°, 60°): High-precision profiles built for sharp bend angles and initial air-bending sequences.
- Gooseneck Press Brake Punches: Deep-throat geometries designed to provide clear clearance for deep-box profiles, return flanges, and tight channels.
- Radius & Offset Tools: Precision-ground profiles for continuous large-radius bends and two-step offset forming.
- Sash & Narrow-Space Punches: Slim-body punches engineered for tight enclosure clearance and narrow-channel processing.
Press Brake Dies
- Single-V & Multi-V Die Blocks: Versatile die blocks accommodating multiple sheet metal gauges for rapid production shifts.
- Hemming & Flattening Combinations: Integrated tooling solutions for smooth seam closing; explore our specialized 30-degree press brake die for air bending and hemming to streamline multi-stage sheet operations.
- Adjustable V-Opening Dies: Heavy-duty dies engineered for thick plate fabrication, featuring adjustable openings to eliminate frequent tool changes.
- U-Bend & Custom Profile Dies: Purpose-built forming dies manufactured for custom industrial geometries, featured within our complete catalog of metal forming press brake dies for sale.
Adapters & Mounting Systems
- Ram Extension Blocks: Modular extensions to adjust shut height and extend working stroke length.
- Lower Die Rails: Precision-ground rails for exact die alignment and rapid seating across long press brake beds.
- Press Brake Ram Adapters: Conversion brackets and rails designed to integrate different tool tangs across mixed-brand machinery.
Machine Compatibility & Clamping Fitment
We engineer press brake tooling to seamlessly integrate with all major OEM machine standards, offering direct drop-in replacement or upgrade capabilities that meet R-K Press Brake Die Inc. operational benchmarks.
Supported Clamping Systems
- American Traditional & Precision: Built with standard tang configurations, making our precision-ground American style press brake tooling compatible with traditional ram setups and quick-clamping systems.
- European Style (Amada / Promecam): Formed with standard 8.4 mm x 3.5 mm push-button groove setups for direct fitment on European press brakes.
- Wila / Trumpf / New Standard: Manufactured with precise self-seating pins and safety keys designed specifically for automated Wila Trumpf style tooling hydraulic clamping systems.
- LVD / Bystronic / Cincinnati: Custom tang geometries and safety keyways machined to match specific OEM load profiles and seating mechanisms.
Tonnage & Length Specifications
| Tooling Format | Standard Dimensions | Typical Application |
|---|---|---|
| Sectionalized Sets | 500 mm, 835 mm, and micro-segments | Flexible box forming, localized bending, and quick punch-length adjustments |
| Continuous Solid Lengths | Up to 30 ft (9 m) single-piece construction | Heavy-duty structural bending, continuous long-run sheet metal fabrication |
| High-Tonnage Profiling | Custom heavy-duty load bases | Thicker plate fabrication requiring high tonnage ratings without tool distortion |
Custom OEM/ODM Tooling & Engineering Support
We engineer high-performance custom press brake tooling built to match R-K Press Brake Die Inc. operational standards for complex profiles and non-standard bending jobs.
5-Step Custom Collaboration Workflow
- Drawing Submission: Send us your 2D drawings (DXF/DWG) or 3D models (STEP). We immediately evaluate your geometry, flange lengths, and sheet specs.
- Feasibility Evaluation: We calculate exact tonnage limits and analyze material tensile strength to select the right tool steel and die design.
- 3D Bending Simulation: We run digital collision tests and optimize bend sequences to catch part-to-tool interference before manufacturing starts.
- Rapid Prototyping & Sample Verification: First-article tools undergo CMM dimensional checks to guarantee profile tolerances within ±0.01 mm. Learn more about our comprehensive custom tooling development services for specialized applications.
- Batch Production & Export Packaging: Mass production includes deep induction hardening, precision grinding, laser batch marking, and heavy-duty anti-rust export packing.
Press Brake Tooling FAQs: Standards for R-K Press Brake Die Inc. Fitment
How to select the correct V-die opening based on sheet thickness (the 8x rule)?
We follow the industry standard 8x rule for air bending mild steel: set the V-die opening to 8 times the material thickness (V = 8 × t). For high-tensile alloys or heavy plate, adjust the multiplier to balance force and inside bend radii:
- Thin Sheet (t ≤ 3 mm): V = 6 to 8 × t
- Medium Plate (3 mm < t ≤ 8 mm): V = 8 to 10 × t
- Heavy Plate (t > 8 mm): V = 10 to 12 × t
Consult our press brake die angles guide to match V-openings with target springback allowances and profile geometries.
What tonnage limits apply to acute gooseneck punches versus standard straight punches?
Straight punches transmit force directly along the vertical center axis at 100% rated capacity. Specialized gooseneck press brake punches feature an offset throat profile to clear return flanges, which introduces bending moments that require tonnage derating.
| Punch Geometry | Tonnage Rating | Core Application | Load Constraint |
|---|---|---|---|
| Standard Straight | 100% Full Load | General sheet metal, heavy plate bending | Direct axial compression |
| Acute Angle (30°–60°) | 70%–85% Full Load | Stainless steel, tight springback compensation | Concentrated tip stress |
| Gooseneck Clearance | 50%–70% Full Load | Deep box forming, wide-channel clearance | Bending stress across offset throat |
How does deep induction hardening compare to full-body hardening for tool longevity?
We apply localized deep induction hardening (HRC 55–60) extending 2–3 mm deep at high-friction contact points while keeping a core hardness of HRC 47–50.
- Induction Hardened: High surface wear resistance combined with a shock-absorbing core to eliminate catastrophic fracturing.
- Full-Body Hardened: Uniform hardness throughout the core, making tools brittle under off-center tonnage spikes.
This heat treatment matches original r-k press brake die inc performance benchmarks while extending operational service life by up to 3x.
How to request conversion adapters for fitting American tools on European press brakes?
We manufacture precise ram adapters and die rails to bridge different machine mounting standards. When requesting conversion adapters to mount American style press brake tooling onto European style press brake dies or receivers, provide:
- Machine Specifications: Brand, total tonnage capacity, and full bed length.
- Ram & Bed Profiles: Upper clamping receiver style and lower rail tang slot width.
- Dimensional Envelope: Target working height offset to protect daylight and stroke limits.
Technical Quote Request Checklist
To request a precision tooling quote matching r k press brake die inc operational standards, submit your production parameters using the checklist below.
Order Specification Matrix
| Parameter Category | Required Details | Purpose & Standards |
|---|---|---|
| Machine Setup | Brand, model, max tonnage capacity | Verifies seating fitment and safe working load limits. |
| Clamping Style | American style, European (Amada/Promecam), Wila/Trumpf | Ensures precise receiver compatibility and tang fit. |
| Workpiece Material | Alloy grade, thickness, tensile strength | Determines V-die opening sizing and springback compensation. |
| Bend Geometry | Target bend angle, inside radius requirements | Essential for tooling selection, including specialized radius punches. |
| CAD Attachments | 2D / 3D file formats (.DXF, .DWG, .STEP, .IGES) | Required for clearance checking and bending sequence simulation. |
Submission Guidelines
- Design Files: Attach native 3D STEP or IGES files for rapid collision analysis and custom profile validation.
- Tonnage Limits: Include maximum sheet length and yield strength to prevent tool overload during deep bending operations.
- Technical Guidance: For tooling selection guides and tonnage calculations, review our engineering technical articles.



