

Formula details
Product Details
Overview
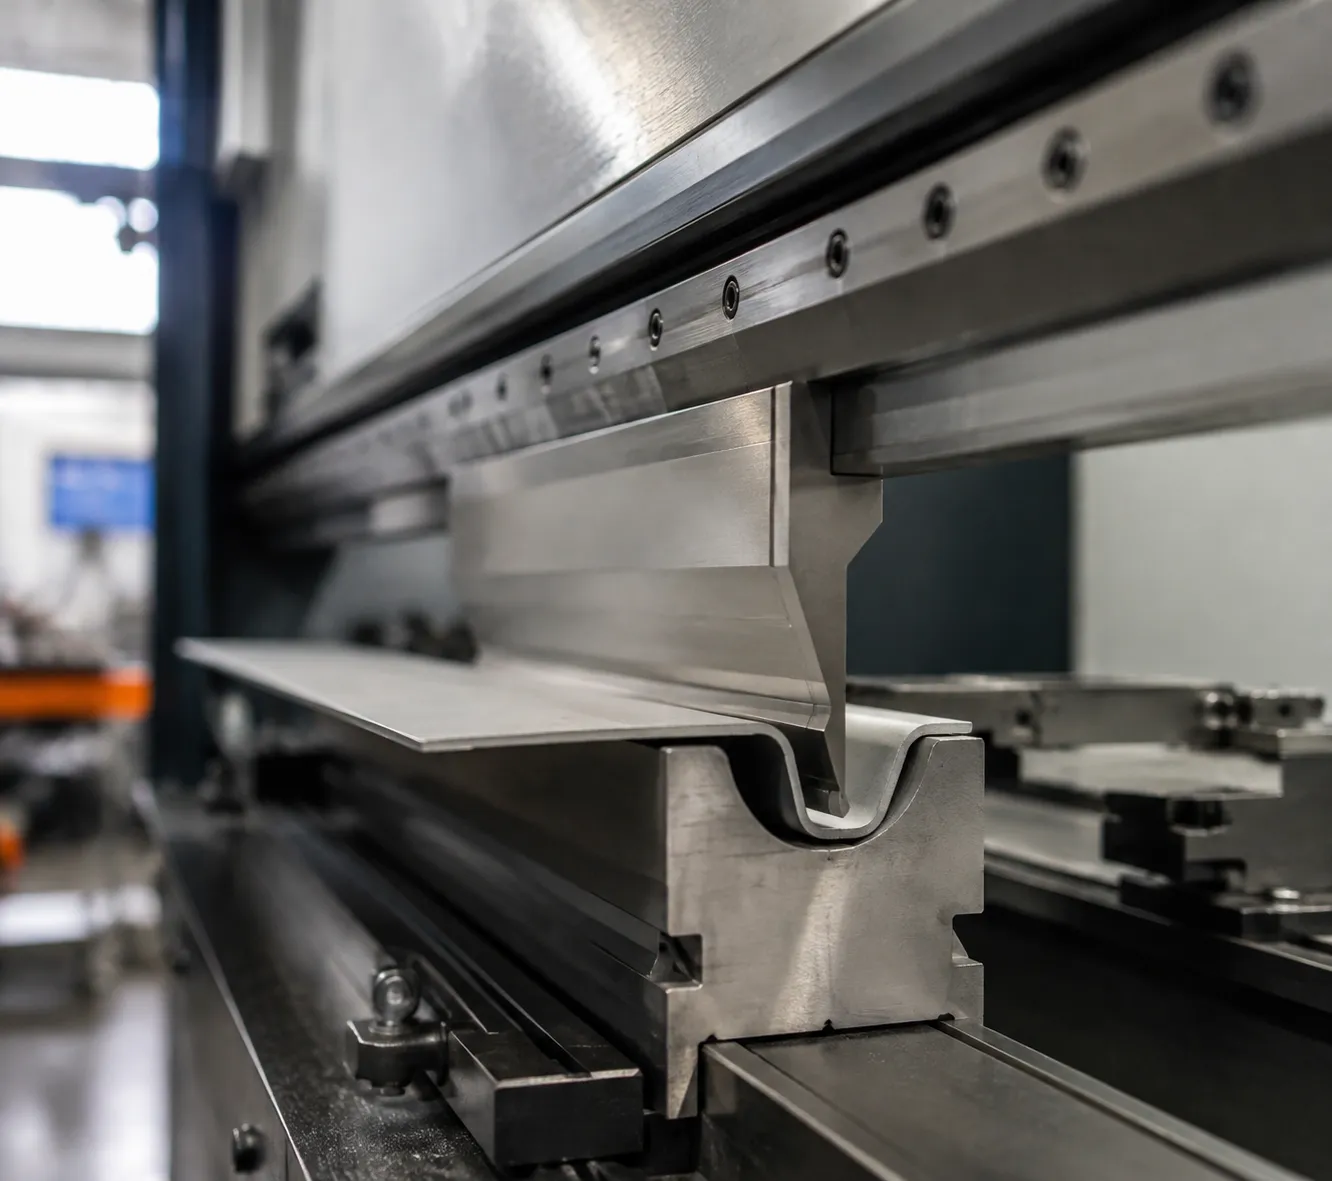
Press Brake Hemming Tools Overview
We engineer high-precision hemming press brake tools to fold sheet metal edges 180° back onto themselves, creating a smooth, reinforced perimeter. Integrating a hemming tool in the press brake eliminates sharp raw edges, doubles structural edge stiffness, and removes the need for additional stiffening hardware.
Core Industry Applications
- Electrical Enclosures: Encapsulates sharp edges to prevent cable abrasion and reinforce cabinet doors.
- HVAC Ductwork: Delivers tight seam seals and structural rigidity on sheet metal ducts.
- Elevator Panels: Strengthens heavy-duty panels against impacts and bending stresses.
- Automotive Components: Provides clean handling margins and structural border reinforcement.
- Architectural Metalwork: Achieves flush, high-end aesthetic finishes on exposed decorative trim.
Standard V-Die vs. Single-Station Hemming Tool
Using an integrated press brake hemming tool accelerates production efficiency compared to traditional two-die setups.
| Feature | Standard V-Die Setup | Integrated Combination Tool |
|---|---|---|
| Process Flow | Two separate tools & setups | Single-station continuous operation |
| Cycle Time | High (part transfer & re-alignment) | Up to 50% faster cycle times |
| Bed Space | Requires dedicated V-die and flattening station | Minimal footprint on press brake bed |
| Part Handling | Double handling increases scratch risk | One-step sequence protects surface quality |
| Tooling Investment | Requires purchasing two individual dies | Single hemming tool press brake unit |
3-Phase Edge Forming Mechanics
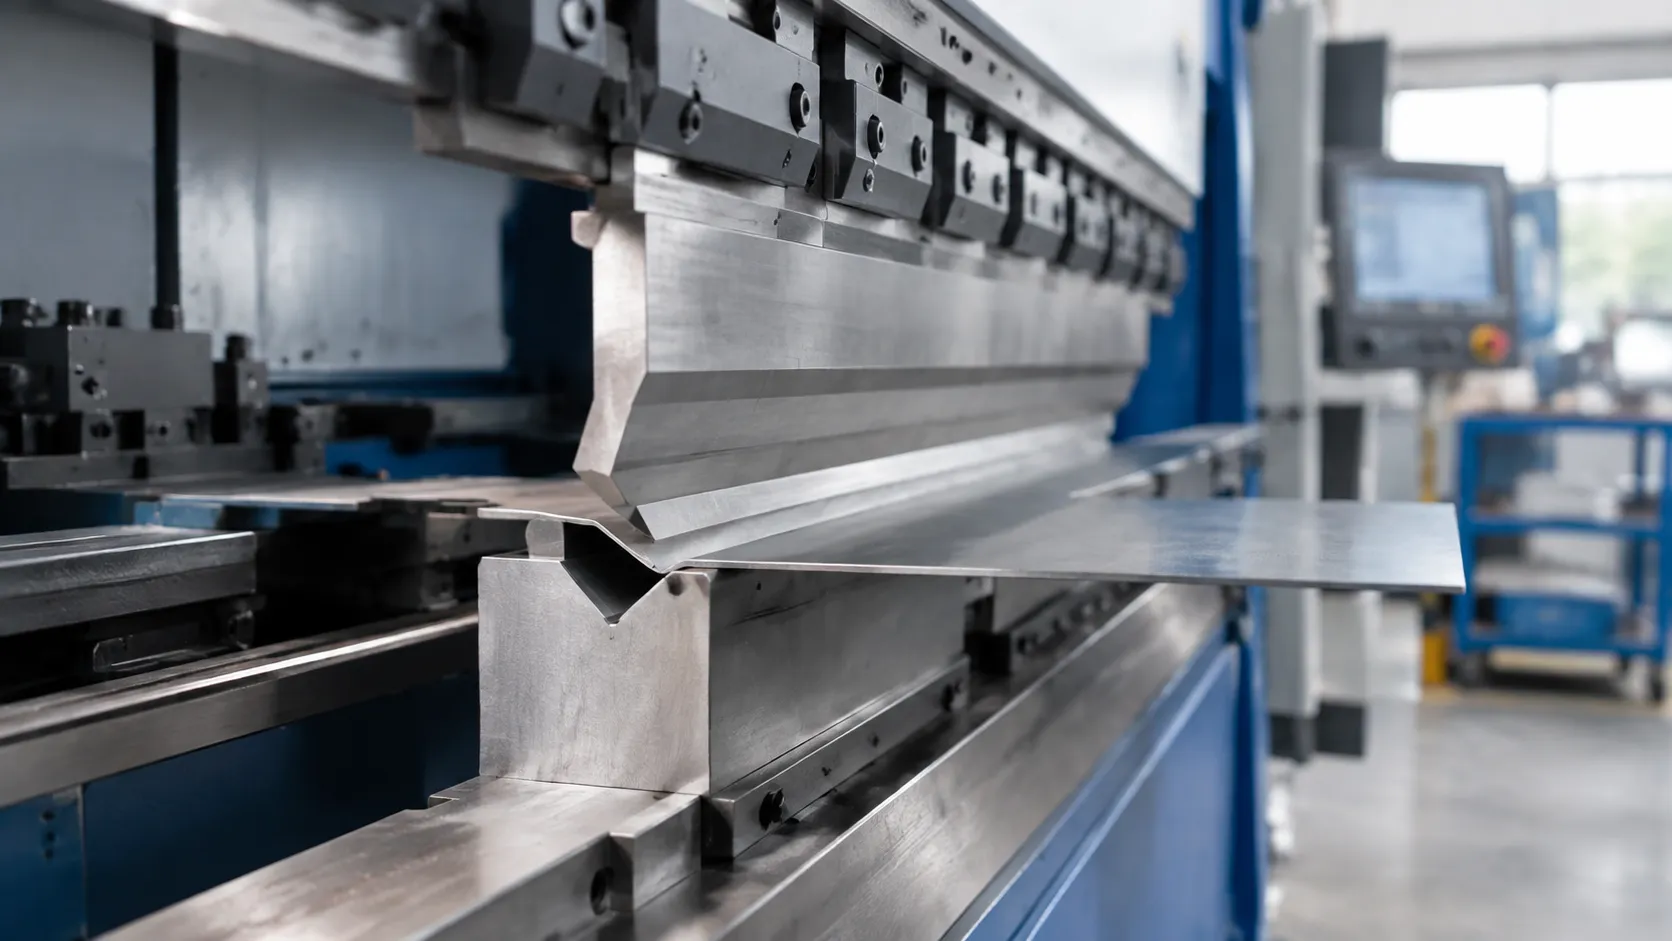
Achieving a clean, burr-free hem requires exact mechanical control. Our hemming press brake tools streamline sheet metal edge folding through a 3-phase process that turns raw edges into rigid, safe structural flanges.
- Phase 1 (Acute Pre-Bending): The upper punch performs an initial 30° to 45° pre-bend. By pairing targeted acute punches with a dedicated 30-degree press brake die for air bending and hemming, we establish the precise bend angle needed for clean flattening without material distortion.
- Phase 2 (Planishing / Flattening): The pre-bent flange moves directly to the lower compression stage. Utilizing a spring-loaded flattening die or Dutch bending table, our hemming tool press brake setup applies controlled tonnage to collapse the flange evenly.
- Phase 3 (Surface Finishing): The final compression stroke smoothly seals open, closed, or teardrop hem profiles. This locks in final part dimensions while completely eliminating sharp, hazardous edges.
Technical Specifications & Material Performance
Built from premium 42CrMo press brake tooling alloys, our tooling minimizes wear during repetitive, high-tonnage flattening operations.
| Feature | Engineering Specification |
|---|---|
| Base Material | Forged 42CrMo / 42CrMo4 alloy steel (Optional: Cr12MoV, D2 tool steel) |
| Hardness | Deep vacuum heat-treated to 56–60 HRC |
| Tolerance | Precision CNC ground to ±0.01 mm |
| Surface Roughness | Ultra-smooth Ra 0.4 µm mirror finish |
| Hem Geometries | Closed hem, open hem, teardrop hem, S-shape return flange |
| Machine Compatibility | European Precision, Wila/Trumpf, Bystronic/RF-A, American Standard |
Built for Versatility and Precision
Whether you run a standard two-stage setup or an automatic spring-loaded hemming tool press brake configuration, our tooling fits directly into your existing machine setup without custom adapters.
- Universal Modularity: Seamless integration with standard clamping profiles, including American and European style press brake tooling systems.
- Damage-Free Bending: Ra 0.4 µm mirror polish prevents surface scoring on stainless steel, pre-painted metals, and delicate aluminum alloys.
- Targeted Hem Profiles: Precision-ground contact surfaces consistently deliver crisp 180° flat closes, uniform open gap tolerances, and protective teardrop radius folds.
Key Advantages of Hemming Press Brake Tools
Structural & Operational Engineering Benefits
- 100% Operator Safety: Forming a closed or teardrop profile completely encapsulates sharp sheet metal edges. This eliminates dangerous burrs, protecting shop personnel during downstream assembly and end-users handling the finished product.
- Doubled Perimeter Rigidity: Folding sheet metal back onto itself doubles edge stiffness across long panels without adding extra weight, structural reinforcements, or hardware.
- Zero Surface Scratches: Our precision-ground contact surfaces prevent cosmetic marring. When working with delicate alloys, adhering to an optimized press brake die selection for aluminum guide ensures scratch-free results on stainless steel, aluminum, and pre-painted stock.
- Massive Cycle Time Reduction: Utilizing a spring-loaded hemming die eliminates secondary tool setups. Performing both the initial acute pre-bend and final planishing phase in a single station cuts handling steps in half and effectively doubles production output.
Performance Impact Breakdown
| Performance Metric | Standard Two-Setup Hemming | Integrated Hemming Tool Press Brake Setup |
|---|---|---|
| Setup Time | Dual-station tool changes required | Single-station continuous bending |
| Surface Finish | High risk of die marks and scarring | Precision-ground anti-marring protection |
| Edge Stiffness | Inconsistent due to manual re-alignment | Uniform, high-rigidity structural hem |
| Production Speed | Baseline output | Up to 2x throughput boost |
Tool Selection & Tonnage Calculation Guide
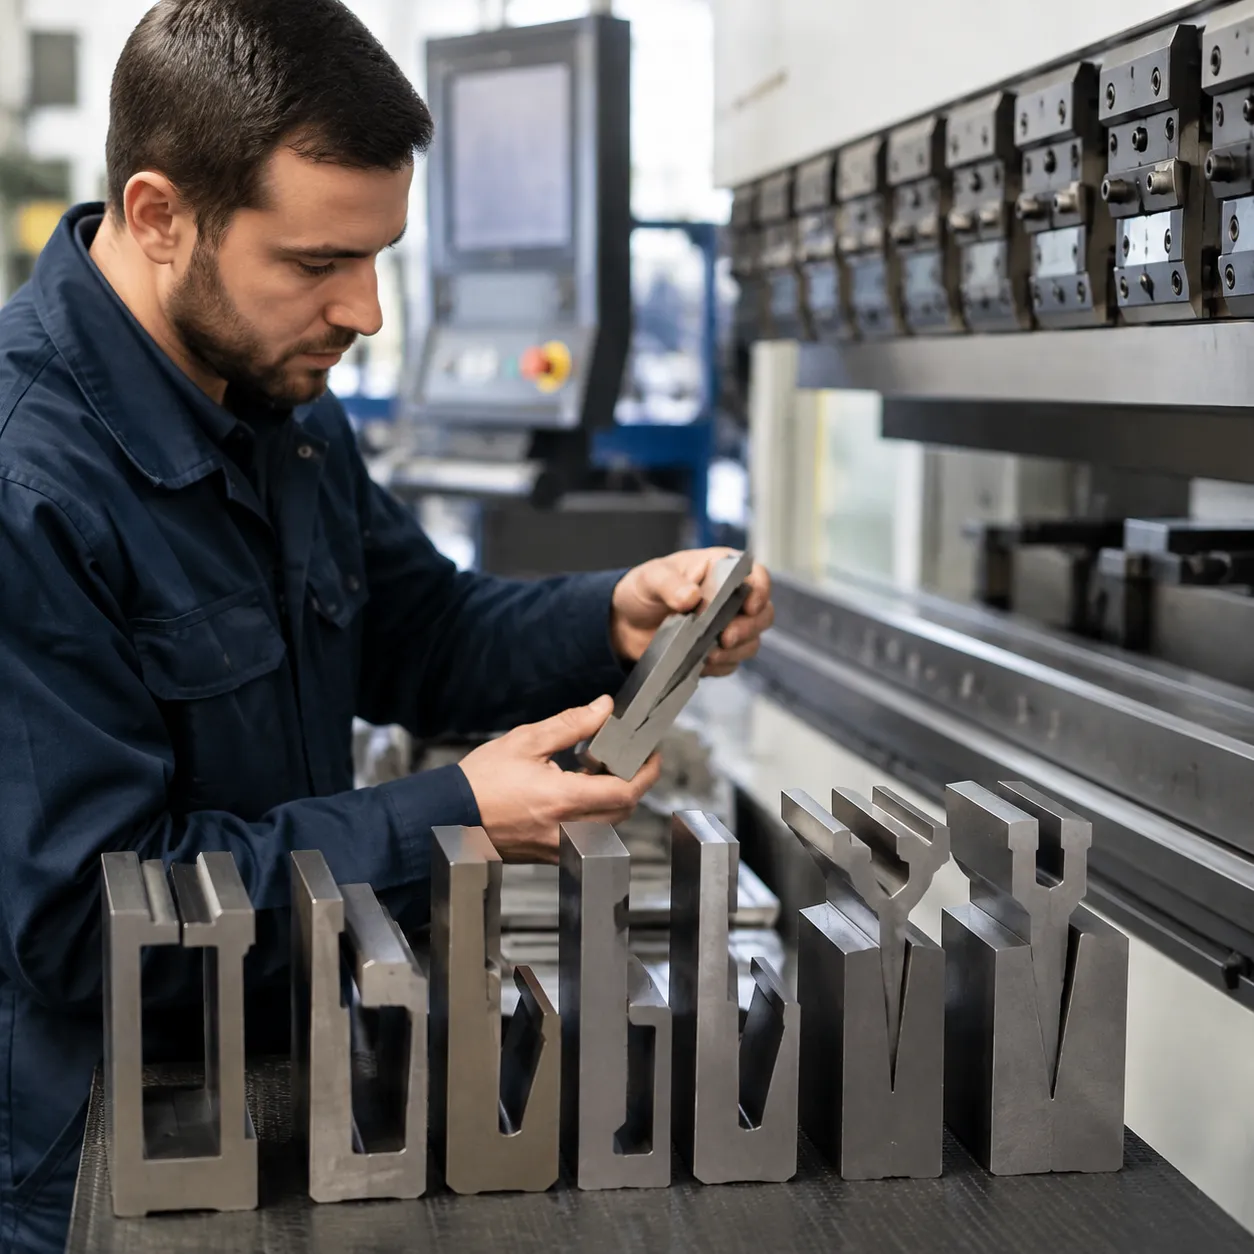
Material Tensile Strength & Force Requirements
Flattening an acute pre-bend into a tight hem requires approximately 3 to 4 times the tonnage of the initial 30° bend. Always verify machine capacity using our press brake die rating guide for tonnage safety before running high-volume jobs with any hemming tool in the press brake.
| Material Type | Tensile Strength | Pre-Bend Tonnage (per mm thickness) | Flattening Tonnage (per mm thickness) |
|---|---|---|---|
| Aluminum (3003-H14) | ~110–180 MPa | ~10–12 Tons/Meter | ~20–25 Tons/Meter |
| Mild Steel (S235/A36) | ~400–450 MPa | ~18–22 Tons/Meter | ~40–50 Tons/Meter |
| Stainless Steel (304/316) | ~600–700 MPa | ~28–35 Tons/Meter | ~65–80 Tons/Meter |
System Selection Matrix
Choosing the ideal hemming tool press brake configuration depends on batch sizes and tool change frequency.
| Selection Factors | Standard 2-Piece Hemming Dies | Spring-Loaded Dutch Bending Table |
|---|---|---|
| Best For | Low-volume, prototype, or heavy-gauge sheets | High-volume production, thin sheet metal runs |
| Setup Operations | Two separate setups (Acute pre-bend, then move to flat die) | Single-station 2-in-1 operation (Pre-bend and flatten in 1 tool) |
| Cycle Time Impact | Slower due to part re-handling between operations | Up to 50% faster cycle times per finished bend |
| Tooling Footprint | Requires double the bed space on the machine | Compact single-station footprint |
Essential Machine Clearance & Force Factors
- Daylight & Open Height: Ensure your press brake has enough daylight clearance to accommodate the collapsed height of a spring-loaded hemming die during full compression.
- Stroke Length Precision: Precise Y1/Y2 axis control guarantees consistent hem gap thickness without over-crushing the material.
- Side-Thrust Compensation: High-force flattening generates heavy lateral loads. Our hemming press brake tools feature built-in guide blocks and heel designs to neutralize side-thrust and protect your ram guides.
- Springback Control: Match the acute punch angle to the material's elastic recovery, as detailed in our press brake die angles guide for springback selection.
Quality Control & Manufacturing Process for Hemming Press Brake Tools
We enforce strict metallurgical standards from raw material selection to final dispatch. Every hemming tool in the press brake undergoes multi-stage testing to guarantee dimensional precision and long-term durability under high tonnage loads.
Raw Material Verification & Testing
Before machining begins, raw 42CrMo alloy steel billets undergo rigorous incoming material validation:
Spectrographic Analysis: Verifies exact chemical composition to ensure optimum hardenability and tensile strength.
Ultrasonic Flaw Testing: Scans raw forgings for internal micro-cracks, voids, and structural inclusions prior to milling.
Precision Machining & Heat Treatment
Our complete manufacturing process combines multi-axis machining with advanced thermal processing to yield tight tolerances:
CNC Milling: Rough-machines raw billets into precise geometries with high-speed 5-axis milling centers.
Deep Vacuum Heat Treatment: Hardens every press brake hemming tool to 56–60 HRC in vacuum furnaces, preventing surface decarburization while securing uniform core toughness.
Precision CNC Grinding: Finish-grinds contact profiles to a tight ±0.01 mm tolerance with an ultra-smooth Ra 0.4 µm surface finish to prevent sheet metal marring.
Audit & Export Packaging
To guarantee zero-defect delivery for critical bending operations, our complete quality control protocol covers every finished die set:
CMM 3D Profile Audit: 100% dimensional inspection using 3D Coordinate Measuring Machines to verify complex profile profiles.
Rockwell Hardness Validation: Multi-point HRC testing along the working edges and flattening tables.
Anti-Rust Export Packaging: Heavy-duty anti-corrosion oil coating, VCI protective wrapping, and custom reinforced wooden crate packaging for safe global transit.
Custom Press Brake Hemming Tooling & OEM Services
When standard dies cannot handle complex box profiles or multi-bend return flanges, we build tailored custom press brake tooling designed for your specific sheet metal edge folding applications.
Engineering Flexibility & Custom Modifications
- Custom Segmented Lengths: Multi-piece sets machined with left and right ear-cut combinations to clear side flanges without tool collisions.
- Special Offset Geometries: Custom acute pre-bend punches and spring-loaded flattening dies adapted for unique sheet thicknesses, non-standard offset dimensions, or tight clearance zones.
- System Integration: Precision ground adapter tangs built to fit European Precision, Wila/Trumpf, Bystronic/RF-A, and American Standard clamping systems.
24-Hour CAD Evaluation & Optimization
Send us your part drawings or CAD files (DXF, STEP, IGES). Our engineering team delivers a rapid 24-hour drawing evaluation along with expert 3D CAD drawing optimization. We analyze tonnage limits, stroke clearance, side-thrust load, and springback allowances to guarantee your custom press brake hemming tool runs reliably right out of the box.
Frequently Asked Questions
What is the difference between open, closed, and teardrop hem profiles?
Hem profile selection depends on material ductility, sheet thickness, and joint requirements:
| Hem Profile | Geometry | Primary Application |
|---|---|---|
| Closed Hem | 0° gap, completely flat fold | Maximum edge stiffness and safety edges on thin sheet steel. |
| Open Hem | Defined internal gap / radius | Heavy-gauge metals or pre-painted stock where full closure cracks the material. |
| Teardrop Hem | Curved, bulbous loop profile | Low-ductility alloys (e.g., aluminum) sensitive to tight bend radii. |
How do you calculate required press brake tonnage for hemming tools?
Edge flattening requires significantly higher force than standard V-bending:
- Pre-Bend Tonnage: Calculated using standard acute air-bending formulas based on material thickness and V-opening.
- Flattening Tonnage: Requires 3x to 4x higher tonnage than the pre-bend stage. As a baseline, flattening 1.0 mm mild steel requires roughly 40–50 tons per meter.
For detailed force charts matching your specific alloy, check out our guide on how to choose press brake tools.
Which clamping systems are compatible with spring-loaded hemming dies?
Our hemming tool press brake line is precision-ground to fit all major machine upper and lower clamping standards:
- European Precision System: Fits standard Amada and Promecam quick-change receivers.
- Wila / Trumpf Style: Direct integration with automatic hydraulic pin-clamping tangs.
- American Standard: 0.5-inch traditional tang design for standard North American press brakes.
- Bystronic / RF-A: Precision upper tang configurations for fast alignment.
We also build custom adapters and specialized metal forming press brake dies to match limited daylight clearance or non-standard stroke lengths.
How do press brake hemming tools prevent surface marring on delicate metals?
We engineer every hemming tool in the press brake setup to protect polished stainless steel, aluminum, and pre-painted metals from contact marks:
- Ra 0.4 µm Mirror Finish: Precision CNC-ground working surfaces eliminate micro-abrasions during sheet insertion.
- Radiused Lead-in Edges: Blunted contact zones distribute compression force evenly across the sheet surface rather than scoring it.
- Protective Film Support: Our lower flattening tables maintain exact alignment with protective urethane tape for critical architectural panels.



