


Formula details
Product Details
Overview
Engineering Specifications & Metallurgy
| Technical Parameter | Specification Standard |
|---|---|
| Mounting Profile | Standard 0.500" (12.7 mm) American tang with safety hook |
| Primary Materials | High-grade 42CrMo (AISI 4140) & Cr12MoV (D2) alloy tool steels |
| Working Edge Hardness | HRC 47–55 (CNC high-frequency induction hardened, 2–4 mm depth) |
| Core Toughness | HRC 28–32 (Through-tempered shock-absorbing core) |
| Machining Tolerance | ±0.01 mm (±0.0004") precision-ground critical surfaces |
| Clamping Compatibility | Standard mechanical and hydraulic American-style clamping bars |
Premium Material Selection
- 42CrMo (AISI 4140): Standard for high-tonnage bending, delivering superior tensile strength, structural fatigue resistance, and deep fracture toughness.
- Cr12MoV (D2): Premium cold-work tool steel engineered for extreme abrasive resistance in high-volume production and stainless steel bending.
Dual-Zone Heat Treatment
- Induction Hardened Wear Points: Tool radii and critical contact edges reach HRC 47–55 to prevent premature wear, deformation, and shoulder galling.
- Tempered Shock-Resistant Core: The structural core is stabilized at HRC 28–32, effectively absorbing heavy dynamic impacts without catastrophic fracturing under peak tonnages.
Precision-Ground Modular Alignment
All load surfaces, clamping tangs, and working tips are CNC ground to ±0.01 mm (±0.0004"). This exact tolerance allows operators to mix, match, and stage sectionalized punch-and-die setups seamlessly across the entire bed without shim adjustments or angular deviation.
Standard American Tang Profile
Featuring the universal 0.500" (12.7 mm) mounting tang equipped with an integrated safety hook/groove, our tooling drops directly into mechanical manual clamps or automated hydraulic clamping systems on all standard North American press brakes.
American Style Press Brake Punches & Upper Tooling Portfolio
We manufacture a complete range of American style press brake punches designed around the standard 0.500" (12.7 mm) tang. Each upper tool is precision-ground and induction-hardened to deliver tight bending accuracy, consistent flange angles, and extended tool life across high-tonnage sheet metal fabrication.
Standard Straight & Radius Punches (88° / 90°)
- Application: General-purpose 90-degree forming and air bending across light to heavy sheet gauges.
- Profiles: Available in sharp, standard radius, and extended reach profiles to match required inside bend radii (IR) and prevent material cracking.
- Specifications: CNC-ground tip radii with tight tolerances to ensure straight, streak-free bends across the full machine bed length.
Gooseneck Punches for Return Flange Clearance
- Application: Ideal for U-profiles, deep channel forming, and complex multi-bend parts.
- Geometry: Features a deep relief pocket that provides substantial clearance for return flanges and previously formed sides, eliminating workpiece collisions during complex bending sequences.
Acute Angle Punches (30°, 45°, 60°)
- Application: Extreme air bending, overbending to compensate for high springback in hard alloys, and primary stage pre-hemming.
- Process Synergy: Pairs directly with matched bottom tools, such as our 30-degree press brake die for air bending and hemming, enabling efficient two-stage safety hem production without tool changeovers.
Sash & Heavy-Duty Offset Punches
- Application: High-load structural bending, deep sash channels, and narrow offset profiles.
- Durability: Reinforced 42CrMo alloy steel bodies engineered to withstand high tonnage concentration while maintaining the required throat depth for specialized clearance.
Segmented Punch Sets with Horns
- Application: Rapid setups for 4-sided enclosure, chassis, and box-and-pan bending.
- Configuration: Supplied in standardized sectional kits featuring precision-cut segment lengths, complete with left and right horn (ear) pieces to clear return side flanges cleanly.
American Style Press Brake Dies Portfolio
Precision 1-Vee & 2-Vee Bottom Dies
- Tight-Tolerance Air Bending: Precision-ground V-grooves ensure exact angular accuracy and consistent springback control.
- Self-Centering Alignment: Standard 0.500" (12.7 mm) tangs center smoothly inside American tool holders to eliminate setup offset.
- Hardened Working Shoulders: CNC induction-hardened radii prevent shoulder wear and sheet galling. Explore our heavy-duty press brake bottom dies for reliable air bending performance.
Multi-V & 4-Way Die Blocks
- Fast Gauge Transitions: Rotate four distinct V-openings on a single block to switch between light-gauge sheet and heavy plate quickly.
- Job-Shop Versatility: Reduces tool changeover downtime and lowers overall tooling footprint.
- High Structural Mass: Solid alloy construction resists deflection under concentrated center-bed loads.
Acute & Hemming Die Combinations
- Two-Stage Hemming: Stage 1 uses a 30° acute V-groove to pre-bend; Stage 2 flattens the edge flush using a spring-loaded or flat top channel.
- Clean Architectural Trims: Eliminates surface cracking on painted, galvanized, or stainless sheet materials.
- Safety Edge Processing: Produces smooth, closed-edge hems for enclosures, panels, and ductwork.
Universal Die Holders, Risers & Conversion Adapters
- Extended Open Height: Precision-machined riser blocks raise lower dies to prevent punch ram collisions on deep box drops.
- Cross-Platform Flexibility: Easily mount American standard tools onto European or custom beds using specialized adapter plates.
- Modular Replacement: Upgrade or replace worn lower setups seamlessly with our dedicated solutions for press brake die replacement for American and European styles.
Tool Lengths & Sectionalization Options
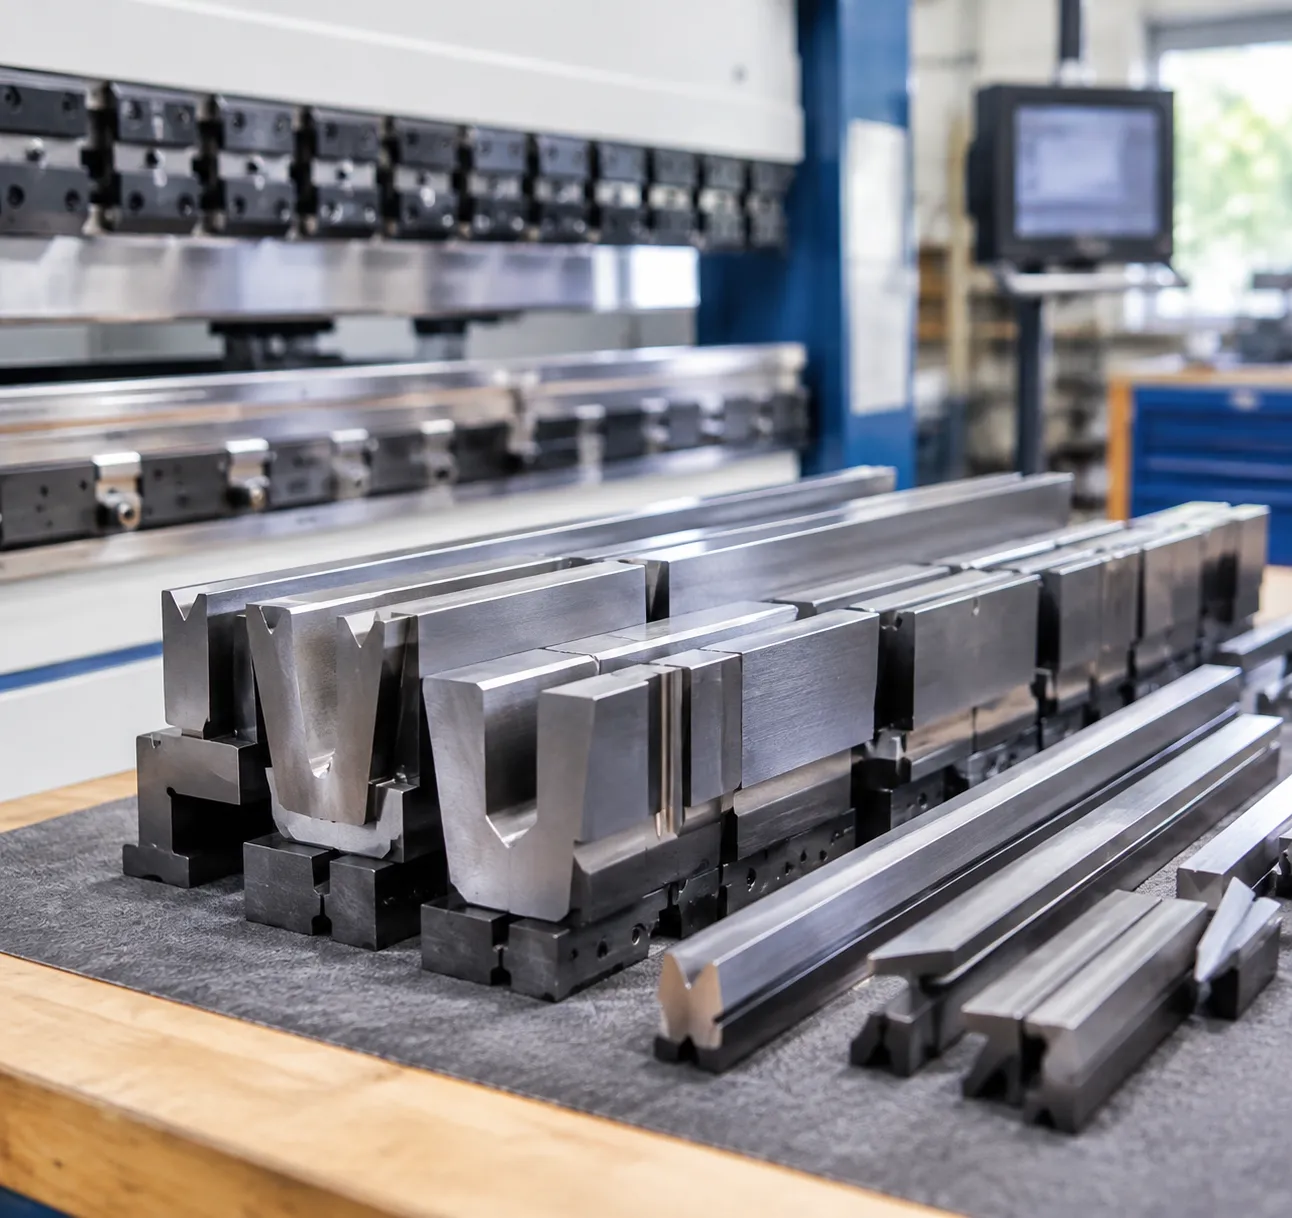
We supply American style press brake tooling in both solid full lengths and precision-cut sectionalized sets to match any bending bed width and component geometry.
Standard Solid Imperial & Metric Tool Lengths
Our solid punches and dies cover standard North American machine beds as well as global configurations. Every tool is precision-ground end-to-end to ensure exact center alignment when butting multiple sections together.
| Configuration Type | Available Lengths | Common Use Cases |
|---|---|---|
| Imperial Solid Lengths | 10", 12", 24", 36", 48" | Standard sheet metal runs, long panels, heavy plate forming |
| Metric Solid Lengths | 415 mm, 835 mm | Standard global lengths, continuous air bending setups |
| Pre-Cut Segmented Sets | Standard complete kits (e.g., 36" / 48" total width) | Complex box, tray, and pan bending with rapid reconfiguration |
Pre-Cut Segmented Tooling Kits for Rapid Setup
To minimize operator downtime during job changeovers, our segmented American press brake tooling kits come pre-cut into matched segments. This allows operators to quickly combine different section widths to bend enclosed boxes, return flanges, and narrow channels.
- Standard Segment Breakdowns: Kits typically include individual widths such as 0.5", 0.75", 1.0", 1.25", 1.5", 2.0", 3.0", 4.0", and 6.0" sections.
- Horned End Pieces: Segmented punch sets include left and right ear/horn sections (typically 3.0" or 4.0") to clear tall side returns on four-sided pan bending.
- Matched Tolerance Grinding: Every segment within a set is ground simultaneously to maintain strict ±0.01 mm (±0.0004") working height uniformity across the entire assembled length.
- Custom Segment Configurations: If your production line requires non-standard segment splits or extended lengths, we provide tailored configurations through our custom press brake tooling engineering service.
Machine Compatibility & Fitment Standards
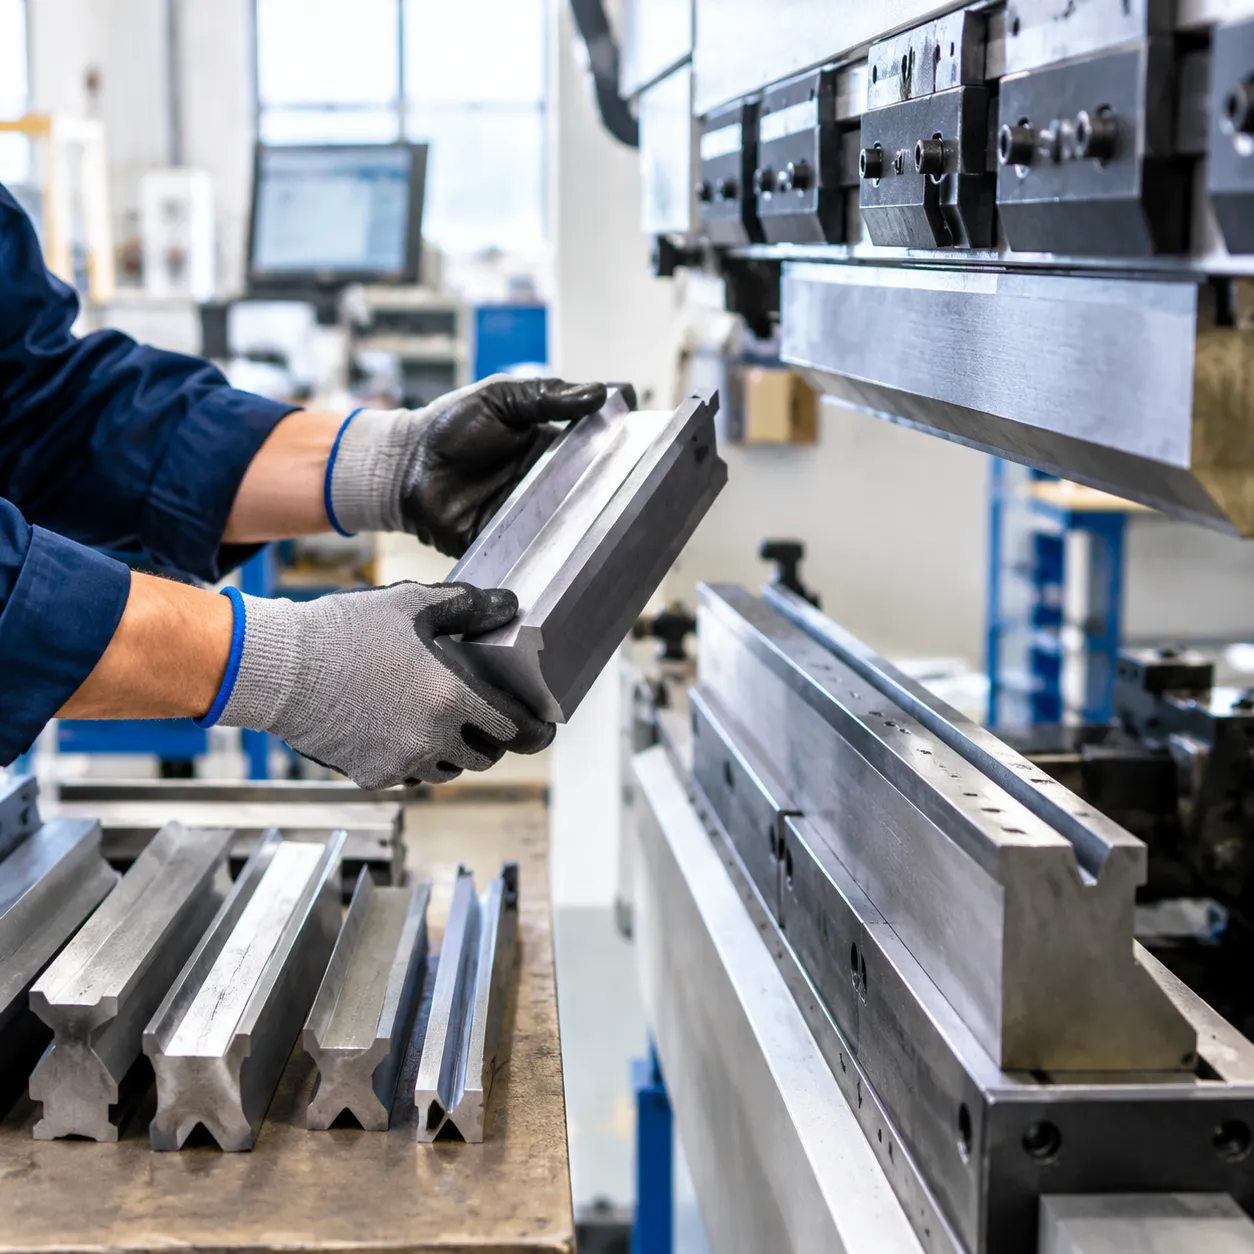
Our American style press brake tooling is precision-engineered to drop directly into standard North American clamping bars without modification. Built around the industry-standard 0.500" (12.7 mm) tang geometry with safety grooves, our punches and dies ensure exact centerline alignment and fast tool changes across standard mechanical, hydraulic, and CNC press brakes.
Direct Compatibility Across Major OEM Brands
We manufacture standard tang press brake punches and lower dies that provide 100% direct fitment for legacy and modern press brake models, including:
Accurpress: Standard mechanical and hydraulic clamping systems.
Cincinnati: Auto-flag and traditional mechanical wedge holders.
Amada (American Style): Fully compatible with conventional American-style tool holders (for dedicated setups, see our Amada tooling options).
Pacific & Wysong: Direct-fit replacement for standard beam and bed configurations.
Universal Clamping & System Integration
Whether your press brake uses manual set-screws or modern rapid-clamping systems, our tooling profiles maintain consistent load transmission across global machine brands:
Direct Integration: Seamlessly mounts to machines from Durma, Baykal, Standard Industrial, Betenbender, and Ermaksan configured with American-style receivers.
Modular Repeatability: Uniform tang dimensions ensure segmented tooling stacks seat flush and hold common working heights across full bed lengths.
Deflection-Free Seating: Ground shoulders and tang relief ensure solid contact against the upper beam, maintaining exact bending tolerances and reliable tonnage distribution under heavy forming loads.
Custom Press Brake Tooling Design & Application Engineering
When standard punches and dies cannot accommodate complex return flanges, tight-clearance geometries, or specialized radii, we provide full engineered-to-order manufacturing for American style press brake tooling. Our technical application team works directly from your DXF, DWG, or 3D STEP files to build dedicated bending solutions tailored to your machine's exact tonnage and clamping profile.
Engineered-to-Order Process
- CAD Review & Feasibility Analysis: We evaluate part drawings to detect potential interference, minimum flange constraints, and springback behavior.
- 3D Bend Simulation: Virtual collision checking confirms punch clearance, die penetration depth, and exact bend sequences before cutting steel.
- Tonnage & Deflection Calculations: Every custom tool design includes finite element analysis (FEA) to verify that bending tonnages stay well within safe working limits.
Specialized Custom Tooling Profiles
We manufacture purpose-built tooling profiles using premium 42CrMo and tool-grade alloy steels:
Large Radius & Special Profile Punches: Custom radius inserts and wide-arc top tools for forming heavy plate and aesthetic panel enclosures.
Deep Channel & Offset Forms: Single-stroke Z-bend and deep-channel tooling designed to eliminate multi-step operations.
Scratch-Free Bending Solutions: Custom urethane V-dies and tooling pads engineered to prevent surface marring on pre-painted sheets, polished stainless steel, and aerospace-grade aluminum.
Dimensional Verification & Quality Assurance
All custom-engineered American style press brake tooling undergoes strict quality control prior to dispatch. Critical centerlines, tang dimensions (0.500" / 12.7 mm), and tip profiles are verified using advanced Coordinate Measuring Machines (CMM) to guarantee ±0.01 mm (±0.0004") manufacturing tolerances. Every custom batch ships with detailed inspection and dimensional verification reports for full traceability.
Why Choose Our American Style Press Brake Tooling?
| Advantage | What We Deliver | Customer Benefit |
|---|---|---|
| Factory-Direct Value | Direct manufacturing without third-party markup | Maximum ROI on standard and custom profiles |
| 100% Quality Control | Strict verification of tangs, centerlines, and radii | Reliable alignment across segmented setups |
| Rapid Global Dispatch | Large stock of standard lengths and segmented sets | Reduced machine downtime and fast project turnarounds |
| Bending Consultation | Full tonnage, springback, and bend allowance guidance | Optimized tool life and defect-free sheet metal forming |
Direct Factory Advantages
- Eliminate Distribution Markups: Sourcing your American style tooling directly from our manufacturing facility delivers transparent, RFQ-based pricing and direct technical accountability.
- Strict Centerline and Tang Verification: Every tool undergoes comprehensive dimensional testing. We inspect 0.500" (12.7 mm) tangs, tip radii, and V-grooves on critical coordinate measuring equipment to guarantee ±0.01 mm interchangeability.
- Extensive In-Stock Inventory: We maintain large inventories of standard straight punches, goosenecks, acute tooling, and precision ground V-dies for immediate shipment.
- Technical Bending Support: Our application engineers assist your team with tonnage limit calculations, bend allowance tables, and springback compensation strategies to solve complex forming challenges before tooling hits the press brake.
American Style Press Brake Tooling FAQs
How to Select the Proper V-Opening for Air Bending Sheet Metal?
The standard rule of thumb for selecting a bottom V-die opening depends on the material thickness ($T$) and tensile strength:
- Mild Steel (T le 3 mm / 0.125''): V = 6 to 8 × T
- Mild Steel (T > 3 mm / 0.125''): V = 8 to 10 × T
- Stainless Steel: V = 10 to 12 × T (compensates for higher tensile resistance and strain hardening)
- Aluminum / Soft Alloys: V = 6 × T
Choosing the correct width maintains consistent inside bend radii and prevents exceeding tonnage limits. For specialized sheet setups, review our guide on press brake die types explained for better metal bending.
Can American-Style Punches Fit European-Style Clamping Systems?
Yes. Standard American-style punches featuring a traditional $0.500''$ (12.7 mm) tang integrate into European (Promecam-style) upper beams by using mechanical conversion adapter bars. These adapters securely clamp the American tang while providing the upper hook profile required for European quick-clamp systems.
What is the Maximum Tonnage Rating for 42CrMo Tooling?
Our 42CrMo (AISI 4140) alloy steel tooling features a dual-zone heat treatment: induction-hardened working surfaces (HRC 47–55) supported by a shock-absorbing tempered core (HRC 28–32). Standard load ratings depend on the tool profile:
| Tool Profile | Average Safe Working Load (Metric) | Average Safe Working Load (Imperial) |
|---|---|---|
| Straight Standard Punches | 100 kN/m - 1000 kN/m | 30 - 100 Tons/ft |
| Gooseneck Clearance Punches | 400 kN/m - 600 kN/m | 15 - 40 Tons/ft |
| Acute (30°/45°) Punches | 600 kN/m - 800 kN/m | 20 - 55 Tons/ft |
| Solid 1-Vee Bottom Dies | 800 kN/m - 1200 kN/m | 50 - 120 Tons/ft |
Air Bending vs. Bottoming vs. Coining Tooling Profiles
| Forming Method | Contact Geometry | Tonnage Requirement | Angle Matching | Tool Wear Factor |
|---|---|---|---|---|
| Air Bending | 3-point contact (tip & 2 die shoulders) | Lowest (Base reference 1×) | Punch angle narrower than part angle (e.g., 85° or 88° for a 90° bend) | Very Low |
| Bottoming (Bottom Bending) | Punch tip and die flank make full contact | Medium (3× to 5× Air Bending) | Punch and die angle match desired finish angle (90° into 90°) | Moderate |
| Coining | Punch penetrates neutral axis of sheet | Extreme (8× to 10× Air Bending) | Exact matching angles under extreme pressure | High / Tool Risk |


