

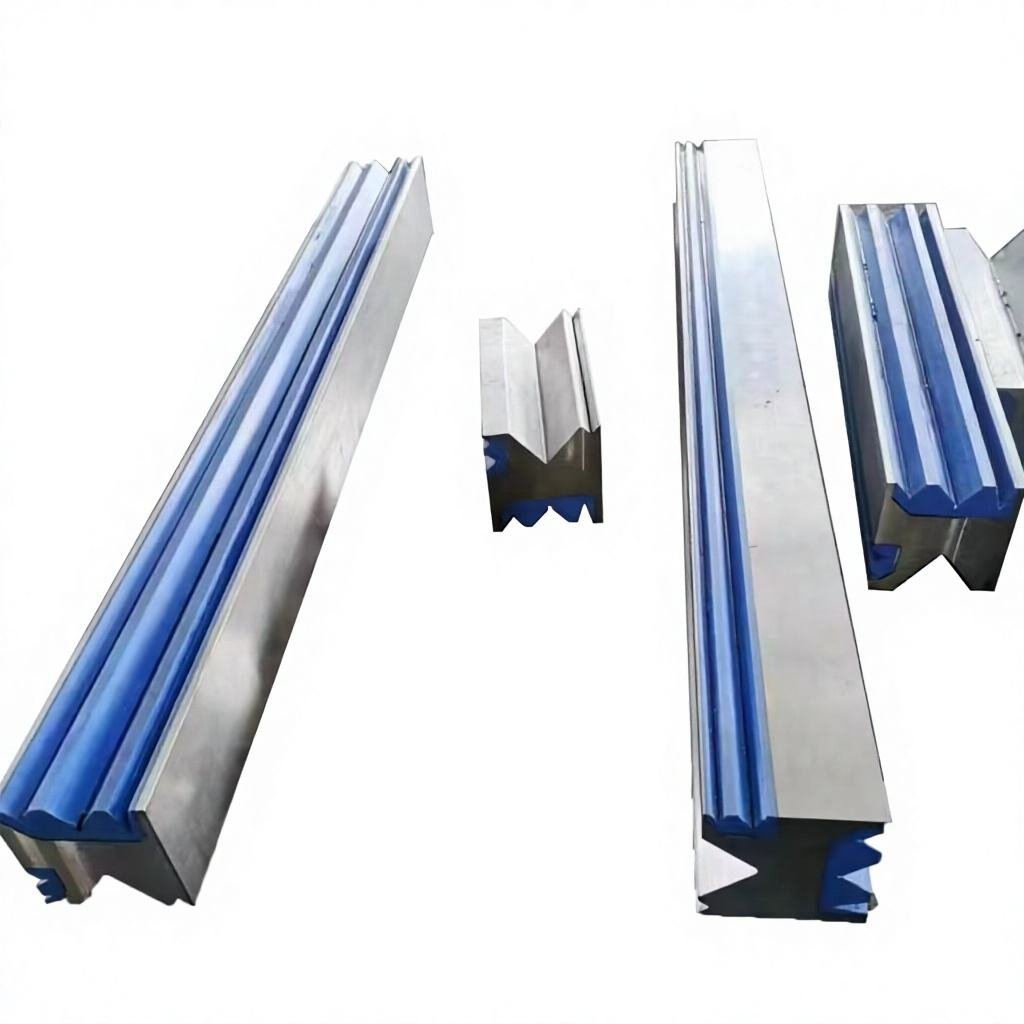
Formula details
Product Details
Overview
Polyurethane Custom Radius Tooling Technical Specifications
We engineer every custom radius forming pad and retainer assembly to maintain tight tolerances and withstand continuous high-tonnage production.
| Specification Parameter | Standard Technical Rating |
|---|---|
| Urethane Durometer Range | 80 Shore A (Soft), 90 Shore A (Standard), 95 Shore A, 75 Shore D (Heavy-Duty) |
| Dimensional Tolerance | Machined & ground to within ±0.01 mm |
| Backing Steel Grade | High-grade alloy tool steel (42CrMo / D2 equivalent) |
| Retainer Hardness | Overall HRC 47–50; Working Edges Induction Hardened to HRC 55–60 |
| Surface Roughness | Profilometer tested Ra < 0.8 µm |
| Sheet Thickness Capacity | 0.5 mm to 10.0 mm (dependent on durometer and pad volume) |
| Quality Verification | 100% CMM optical projection & spectrometer material validation |
Precision Quality Assurance
To guarantee maximum service life for our custom radius tooling pads and urethane v-dies, we enforce strict heat-treatment and manufacturing protocols:
- High-Grade Backing Steel: Retainers are machined from premium alloy steel; consult our press brake die material guide to compare how 42CrMo and D2 steel options perform under extreme bending pressure.
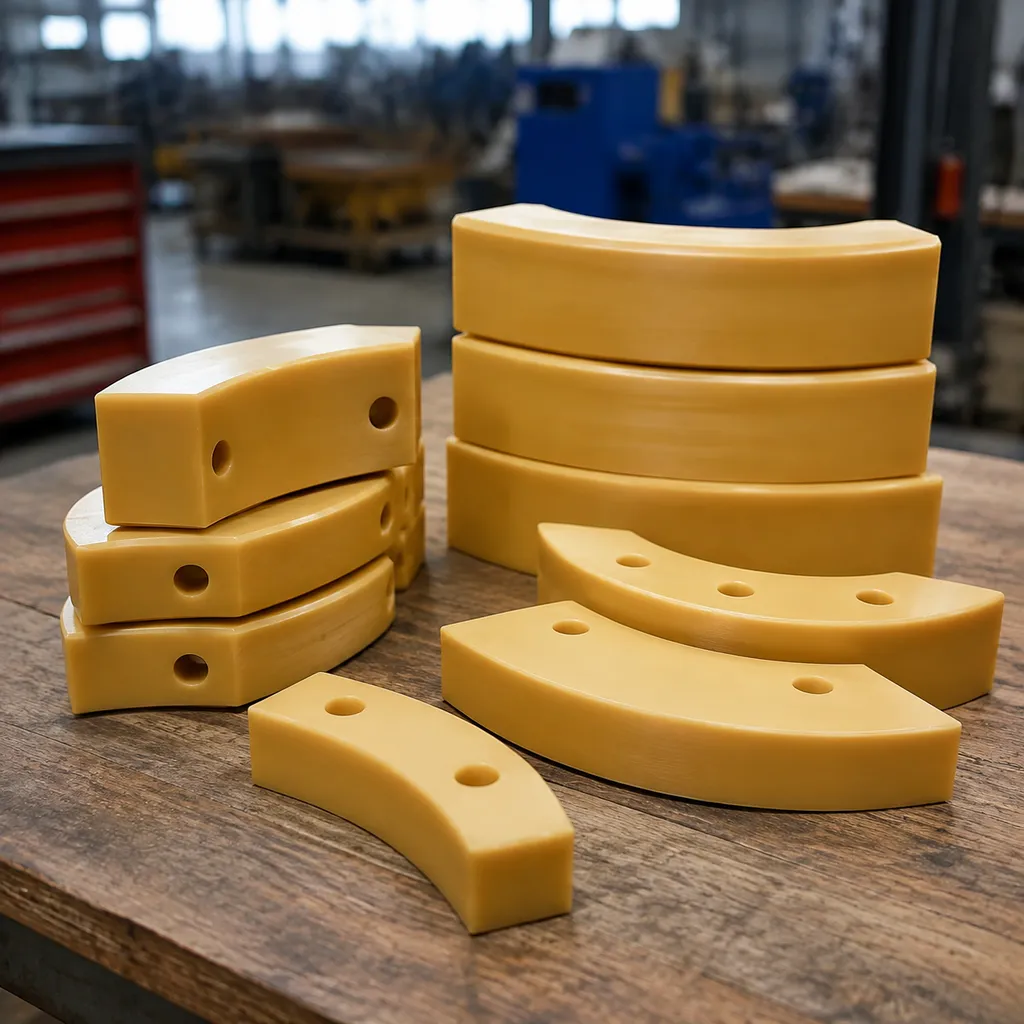
- Tailored Durometer Selection: We stock durometer urethane pads ranging from flexible 80A options for soft, finished alloys up to dense 75D blocks for heavy-tonnage radius forming.
- Superior Surface Finish: Profilometer-verified Ra < 0.8 µm surface finish guarantees smooth sheet flow without marring, galling, or scoring high-finish sheet metal.
Non-Marking Polyurethane Custom Radius Tooling
We engineer polyurethane custom radius tooling to solve surface marring and cycle-time bottlenecks in metal fabrication.
Engineering Differentiation & Performance Overview
| Bending Parameter | Standard Steel Tooling | Our Custom Urethane Tooling | Production Impact |
|---|---|---|---|
| Surface Protection | Scratches, galling, tool marks | 100% mark-free bending | Eliminates protective film & rework |
| Forming Method | 20+ hit bump forming cycles | 1-hit radius stroke | Increases throughput by up to 70% |
| Material Memory | Permanent die wear | High tear strength thermoset elastomer | Full geometric recovery over millions of cycles |
| Tooling Lifespan | Frequent die regrinding | Vacuum heat-treated steel + wear poly-dies | Delivers 3x tool life extension |
Core Operational Advantages
- 100% Mark-Free Bending: Our custom metal forming radius pads protect delicate materials—including mirror-finish stainless steel, pre-painted architectural panels, anodized aluminum, and polished brass—without applying protective tape or film.
- 1-Hit Radius Forming: Convert labor-intensive 20+ hit bump forming routines into a single press brake stroke, driving massive cycle-time reductions.
- Shape Memory & High Tear Strength: Advanced thermoset formulation maintains structural integrity and recovers original geometry even under severe, high-tonnage loads.
- 3x Tool Life Extension: Combining precision vacuum heat-treated alloy tool steel backing with wear-resistant urethane v-dies drastically reduces tooling replacement overhead.
Polyurethane Custom Radius Tooling Configurations
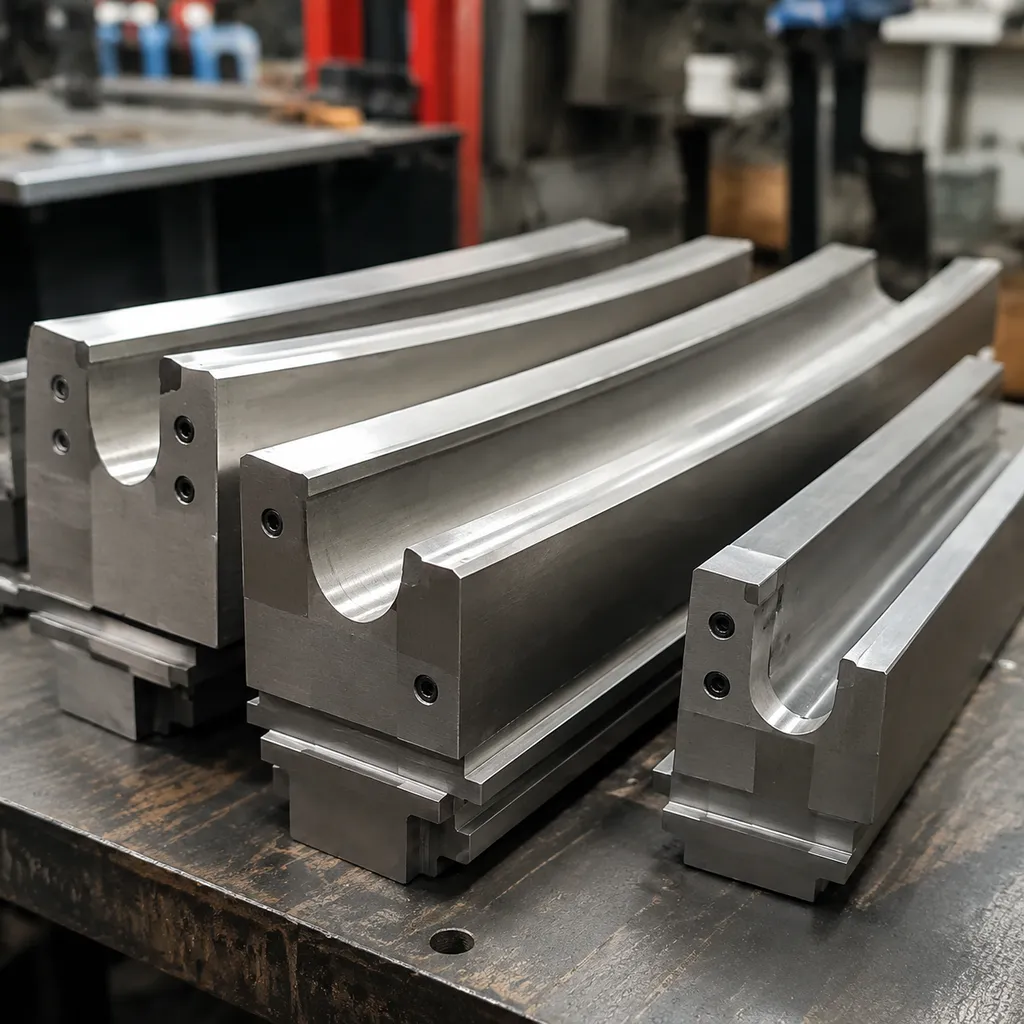
Core Product Categories
- Custom Radius Tooling Pads & Retainers: Machined alloy steel holders equipped with deflector bars and high-durometer custom radius tooling pads built for consistent large-diameter radius forming.
- Urethane V-Dies & Drop-In V-Pads: Precision triangular poly inserts engineered to fit directly into standard machine beds and steel bottom dies for tight-radius, scratch-free sheet metal bending.
- Hemming Urethane Press Brake Dies: Specialized two-stage systems that execute a 30° pre-bend and flat hem in a single setup without leaving surface score lines. For delicate material processing, explore our high-precision hemming dies.
Tooling Specification & Application Matrix
| Product Category | Primary Function | Key Design Features | Machine Integration |
|---|---|---|---|
| Custom Radius Tooling Pads | Large Radius Bending Tooling | Machined steel retainers with deflector control | Bed-mounted steel retainers |
| Urethane V-Dies | Non-Marking V-Bending | Drop-in poly inserts with high tear strength | Standard bed slots & rail systems |
| Hemming Urethane Dies | 2-Stage Hemming & Flattening | Zero-score dual-action forming profile | Standard press brake clamping |
Universal Machine Clamping Compatibility
We engineer custom tangs, holders, and adaptors to ensure direct, drop-in fitment with major global clamping standards:
- European & New Standard: Direct fitting for WILA and Trumpf machines.
- American Precision: Full compatibility with Cincinnati, Pacific, and traditional style holders.
- Global Press Brake Systems: Custom fitments available for Bystronic, Amada, LVD, and regional machines.
Discover our full range of production-ready metal forming press brake dies engineered for high-tonnage precision.
Custom Engineering Process for Polyurethane Radius Tooling
| Step | Stage | Engineering & Manufacturing Action |
|---|---|---|
| 1 | Drawing & Spec Submission | We evaluate 2D DXF/DWG or 3D STEP files, analyzing sheet thickness, bend radius, and tensile strength against our press brake die size chart and dimensions guide. |
| 2 | Tonnage & Springback Evaluation | We calculate pad volume displacement, deflector bar limits, and metal springback using our press brake die angles guide for springback selection. |
| 3 | 3D Simulation & Collision Testing | CAD modeling verifies punch clearance, clamp fitting, and stroke limits for custom radius forming pads and urethane v-dies prior to machining. |
| 4 | Precision Machining & Quality Inspection | We execute CNC profile grinding, vacuum heat treatment on steel retainers, and CMM optical validation to maintain strict tolerances. |
| 5 | Global Fast-Track Delivery | Complete export packaging with full material traceability certificates shipped directly to your shop floor. |
Precision Quality Controls
- CAD/CAM Integration: Direct translation from customer STEP models to CNC grinding paths guarantees complete geometric accuracy.
- Tonnage & Volume Calculations: Polyurethane pad volume displacement is matched to punch penetration depth to prevent premature pad rupture.
- 100% CMM Validation: Optical projection testing and spectrometer material verification ensure every die meets engineering specifications.
Target Applications for Polyurethane Custom Radius Tooling
Sector Breakdown & Performance Impact
- Architectural & Elevator Panels: We deploy our custom radius forming pads to handle mirror-finish stainless steel and brushed claddings. This setup delivers 100% scratch-free radius forming without protective film, making it essential for high-end elevator manufacturing applications.
- Electrical Cabinets & Enclosures: Fabricating pre-painted, powder-coated, or coated mild steel requires zero surface fracturing. Our custom metal forming radius pads distribute tonnage evenly across the bend, preventing edge cracking and protective coating shear.
- HVAC & Metal Furniture: Achieving tight-radius bends and flat seams on thin-gauge aluminum or galvanized sheet metal is seamless with our hemming urethane press brake dies. This process stream accelerates output for metal furniture production while ensuring smooth, burr-free edges.
- Automotive & Commercial Transportation: For high-volume cab components, structural trim, and specialized brackets, our non-marking press brake dies deliver repeatable, high-precision radius forms across millions of strokes.
Technical Selection Guide & FAQ
Selecting Urethane Durometer for Material Thickness
Choosing the right hardness for your custom radius tooling pads and polyurethane custom radius tooling depends directly on sheet thickness, material tensile strength, and forming tonnage. For precise setup guidelines, consult our detailed press brake die selection guide.
| Durometer | Sheet Thickness | Suitable Materials | Bending Characteristics |
|---|---|---|---|
| 80A / 90A Shore | 0.5 mm – 3.0 mm | Stainless steel, polished brass, anodized aluminum, pre-painted sheet | Low to medium tonnage; maximum surface protection without tooling marks |
| 95A Shore | 2.5 mm – 6.0 mm | Mild steel, architectural stainless, structural aluminum | Medium to high tonnage; balanced pad displacement and high wear resistance |
| 75D Shore | 5.0 mm – 10.0 mm | Heavy carbon steel, high-tensile plate, commercial vehicle panels | High-tonnage capacity; minimal pad deflection under extreme forming loads |
Urethane Pad Displacement Rule for Radius Bending
To prevent premature pad rupture and ensure consistent part radius geometry when using custom metal forming radius pads, follow the core volume displacement rules:
- 15% Penetration Limit: Limit the punch penetration depth to a maximum of 15% of the total urethane pad thickness per stroke.
- Side Relief Clearance: Provide sufficient lateral space or spring-loaded deflector bars within the steel retainer so the compressed poly pad can expand laterally under load.
- Volume Matching: Ensure the void volume inside the retainers matches the displaced volume of the punch penetration to avoid hyper-compressing the poly material.
Custom Retainers for Legacy Press Brakes
We engineer tailored adapters and retainers for non-standard, older, or custom press brake beds. Through our specialized custom press brake tooling division, we customize tang profiles, overall working heights, and side-clamping features to match American Precision, European, WILA, Trumpf, Bystronic, Amada, LVD, and Cincinnati mounting systems without modifying your existing machine bed.
Related Sources
- https://www.thefabricator.com/thefabricator/blog/bending/an-introduction-to-urethane-tooling-for-the-press-brake
- https://wilsontool.com/en-us/resources/mark-free-bending-solutions-brochure
- https://www.polyprod.com/urethane-press-brake-dies-%E2%80%93-precision-results-with-extended-tool-life/
- https://www.polyprod.com/urethane-press-brake-dies-%E2%80%93-precision-results-with-extended-
- https://www.thefabricator.com/thefabricator/blog/bending/how-to-use-urethane-tooling-at-the-press-brake



