

Formula details
Product Details
Overview
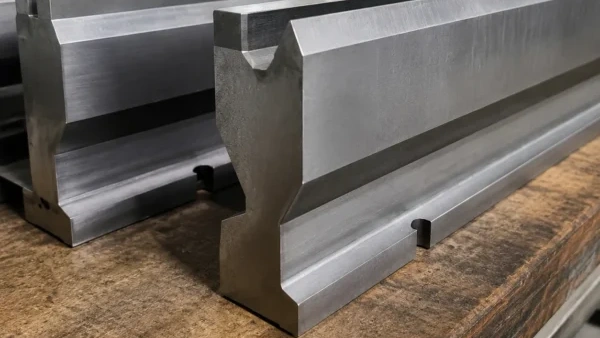
Detailed Technical Specifications: 3in American Style Press Brake Die
Mechanical Parameters & Specifications
| Parameter | Engineering Standard / Specification |
|---|---|
| Tooling Style | American Precision Style Tooling |
| Tang Geometry | Standard 0.50 in x 0.625 in (1/2" x 5/8") American Tang with optional safety pin/groove |
| V-Opening Width | 3.00 in (76.2 mm) V-Opening |
| Standard Die Angles | 85°, 86°, 90° (Custom 30° / 60° available) |
| Core Material | Heavy-duty AISI 4150 / 42CrMo Alloy Steel |
| Working Edge Hardness | 55–60 HRC (High-Frequency Deep Induction Hardened) |
| Core Hardness | 28–32 HRC (High shock absorption & fracture resistance) |
| Grinding Precision | ±0.01 mm (±0.0004 in) precision ground press brake lower die centerline |
| Surface Finish | Ra < 0.8 µm micro-finished V-groove |
| Standard Lengths | 415 mm, 835 mm, sectionalized sets, or single pieces up to 14 ft (4100 mm) |
Key Dimensional Cross-Section Features
Our exact press brake die opening dimensions ensure seamless installation into standard American bed slots while distributing high tonnage evenly across the press brake bed:
- V-Opening Width (3.0 in / 76.2 mm): Optimized shoulder geometry reduces friction and material drag during heavy plate displacement.
- Precision Shoulder Radius: CNC-ground entry radii minimize work-piece galling and sheet marking on pre-painted or stainless materials.
- Overall Height Consistency: Strict height tolerances eliminate center-sag issues and ensure uniform bend angles across extended bed lengths.
- Lower Tang Seating (0.50 in x 0.625 in): Engineered for american style press brake tooling 1/2 x 5/8 tang receivers with zero slop for accurate self-centering.
Engineering Superiority of the 3in American Style Press Brake Die
Micron-Level Alignment Accuracy
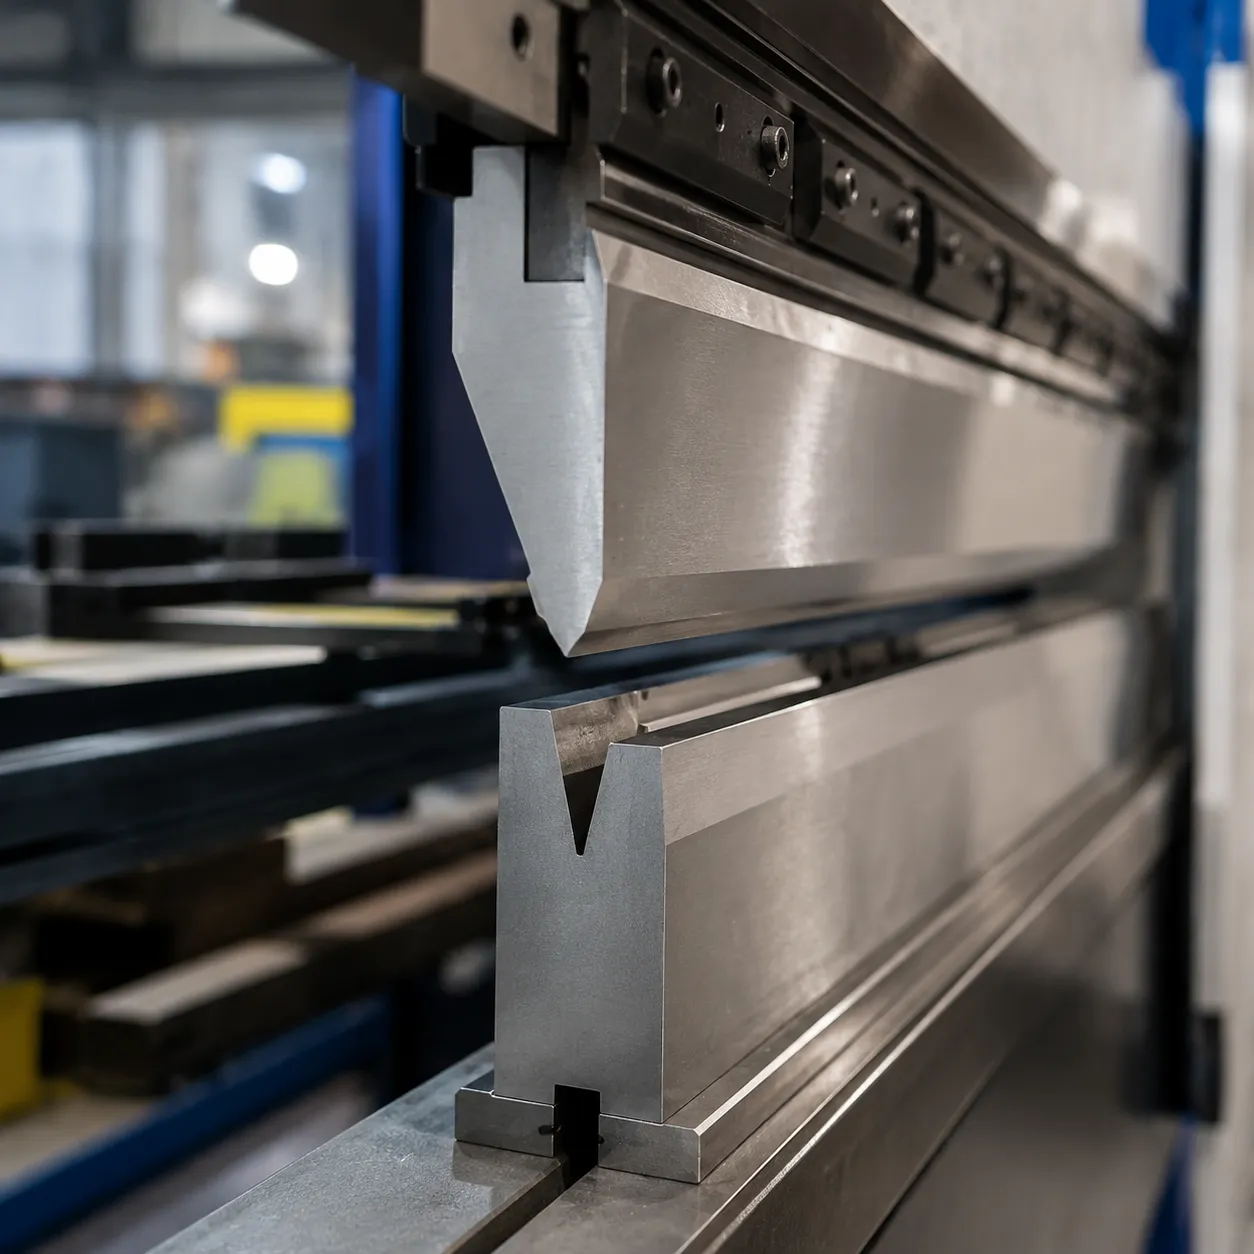
- Precision CNC Surface Grinding: Machined to a critical tolerance of ±0.01 mm along the entire tooling length.
- Uniform Centerline Accuracy: Perfectly centered V-grooves eliminate angular variations across long sheets, drastically reducing setup time and operator shimming.
- Repeatable Positioning: Precision-milled lower tangs drop directly into standard bed slots with instant seating alignment.
3x Extended Tool Life via Deep Induction Hardening
We combine controlled vacuum heat treatment with targeted high-frequency induction hardening on high-wear contact points.
- Ductile Shock-Absorbing Core: Premium grade steel cores maintain toughness to absorb heavy bending impacts without catastrophic failure.
- Hardened Wear Surfaces: V-opening shoulders reach 55–60 HRC surface hardness, providing three times the service life of standard unhardened tooling.
- High-Tonnage Endurance: Built for heavy plate processing; check out our press brake V-die lifespan guide to see how selective edge hardening maximizes total bend cycles.
Micro-Finished Surface Control (Ra < 0.8 µm)
- Reduced Sliding Friction: Micro-finished V-grooves under Ra 0.8 µm let sheet metal slide smoothly into the die opening during forming.
- Anti-Marring Performance: Low surface roughness prevents material galling and protective film tearing when bending stainless steel, aluminum, or pre-painted stock.
- Optimized Material Selection: To match hardness profiles with specific sheet alloys, refer to our comprehensive press brake tooling material guide.
| Performance Spec | CAMT Precision 3in Die | Standard Commercial Die |
|---|---|---|
| Grinding Precision | ±0.01 mm centerline accuracy | ±0.05 mm – ±0.10 mm variance |
| Working Edge Hardness | 55–60 HRC (Induction Hardened) | 28–35 HRC (Core Hardened only) |
| Surface Finish (V-Groove) | Ra < 0.8 µm micro-finish | Ra 1.6 µm – 3.2 µm standard mill finish |
| Setup & Shimming Time | Zero to minimal shimming | Frequent shimming required |
Material Gauge Selection & Bending Capacity
Recommended Material Thickness
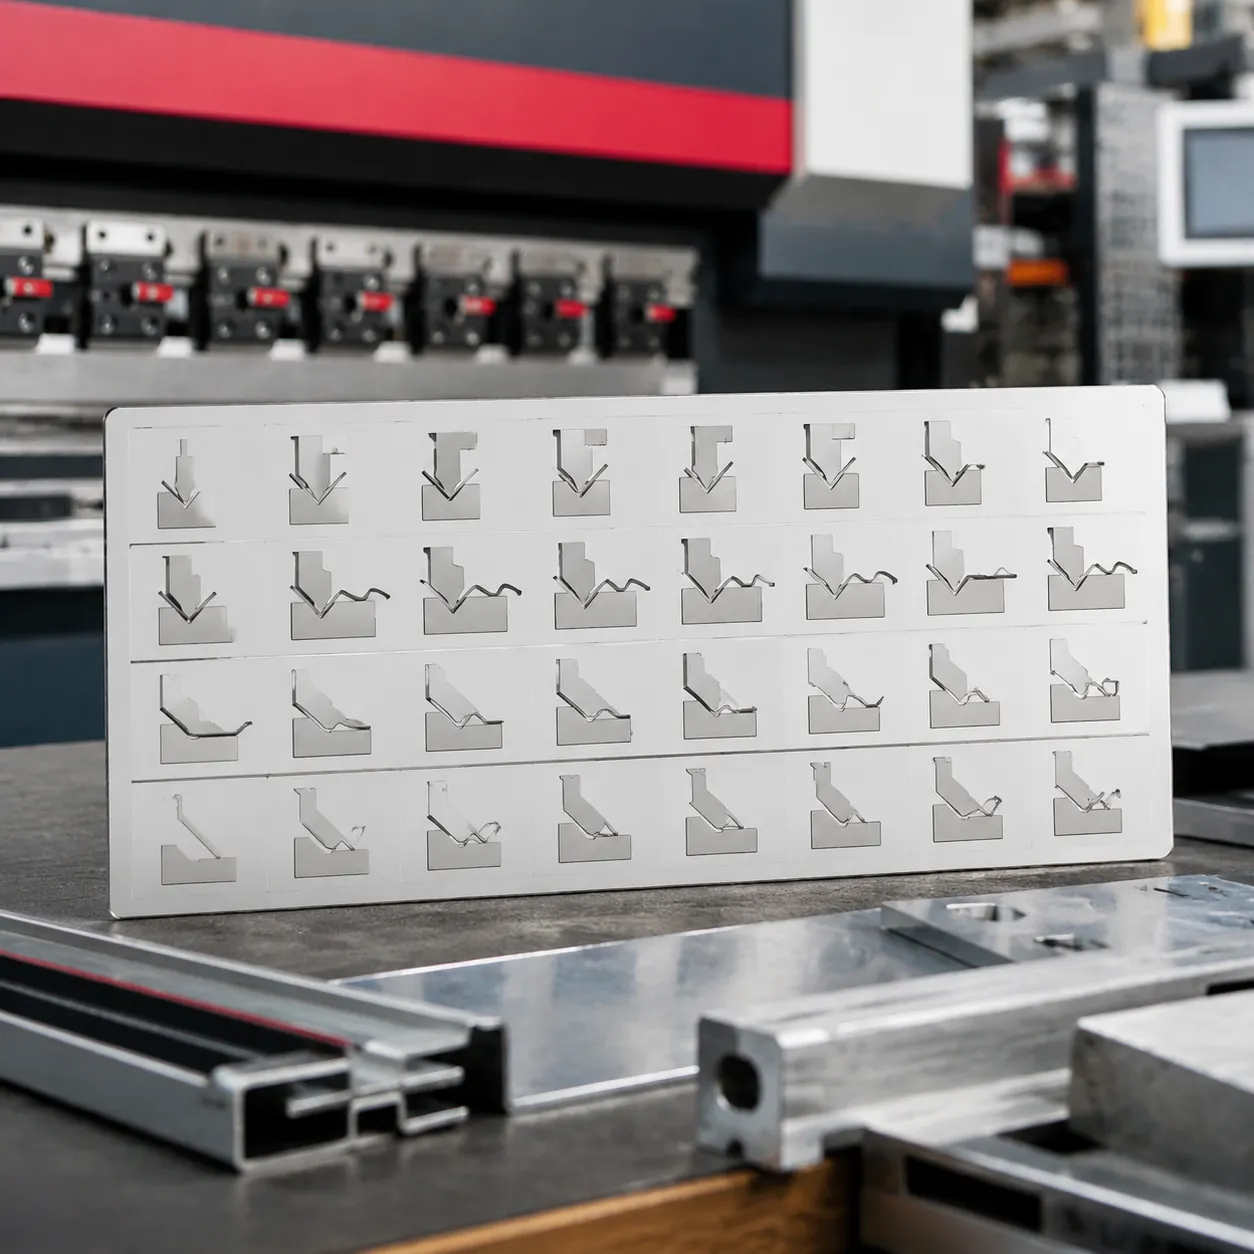
For optimal air bending, we follow the standard 8x Rule where the V-opening width equals 8 times the material thickness (V = 8 × T).
- 3/8 in (9.5 mm) Mild Steel Plate: The standard target thickness for a 3in american style press brake die. Provides precise 90-degree bends with standard tonnage load.
- 1/4 in (6.35 mm) Steel Plate: Running 1/4-inch plate in a 3-inch V-opening increases the inside bend radius, significantly reducing required force and providing maximum springback control.
- Heavy Plate Bending: Suitable for forming high-tensile plate up to 1/2 inch thick when running larger bend radii without over-stressing the die shoulders.
When running tough alloys or demanding stainless steel processing, matching material yield strength to the proper V-width is critical to prevent die shoulder wear and micro-fracturing.
Tonnage Limit & Load Allowance
Our heavy plate bending bottom die is engineered to handle heavy hydraulic loads safely. Operate within these maximum tonnage limits per foot and meter to maintain tooling precision:
| Material Type | Material Thickness | Die V-Opening | Max Load (Tons/Ft) | Max Load (kN/m) |
|---|---|---|---|---|
| Mild Steel (42,000 PSI) | 3/8 in (9.5 mm) | 3.0 in (76.2 mm) | 14.5 | 475 |
| Stainless Steel (60,000 PSI) | 3/8 in (9.5 mm) | 3.0 in (76.2 mm) | 21.0 | 690 |
| Structural Aluminum (30,000 PSI) | 3/8 in (9.5 mm) | 3.0 in (76.2 mm) | 7.5 | 245 |
| Mild Steel (42,000 PSI) | 1/2 in (12.7 mm) | 3.0 in (76.2 mm) | 28.0 | 920 |
For severe structural forming, pair this die with our high-capacity heavy metal bending tooling to ensure maximum bed load distribution and frame stability.
Press Brake Machine Compatibility & Fitment
Supported Press Brake Brands & Tang Configurations
Our tooling fits a wide range of leading OEM machinery equipped with standard American planed or precision-ground die holders. If you need help matching your machine's exact bed slot profile, review our press brake die selection guide to ensure flawless fitment across your shop floor.
| Press Brake Brand | Compatibility Status | Recommended Tang Configuration |
|---|---|---|
| Cincinnati | Fully Compatible | Standard 0.50 in x 0.625 in American Tang / T-Style |
| Accurpress | Fully Compatible | Standard 0.50 in x 0.625 in American Tang with Safety Pin |
| Amada (American Style) | Fully Compatible | Standard American Tang / Safety Groove |
| Pacific & LVD | Fully Compatible | Standard 0.50 in x 0.625 in American Tang |
| Niagara & Wysong | Fully Compatible | Standard American Tang |
| Chicago Dreis & Krump | Fully Compatible | Standard American Tang |
Secure Seating & Tang Options
To guarantee operator safety and lock in repeatable bending accuracy across high-tonnage runs, we offer multiple lower tang retention styles for our 3in V-opening lower die sets:
- Standard American Tang (0.50 in x 0.625 in / 12.7 mm x 15.875 mm): Drops directly into standard American bed rails and set-screw locking channels.
- Safety Pin Retainers: Machined cross-holes accept spring-loaded or mechanical safety pins to prevent lateral shifting during heavy plate load changes.
- Safety Groove Tangs: Precision-machined locking grooves engage with side-clamp systems for quick, secure vertical clamping and safety compliance.
For specialized setups requiring custom bed slot lockups, explore our Cincinnati-compatible press brake die sets engineered specifically for heavy-duty industrial applications.
CAMT Quality Guarantee & Manufacturing Process
We engineer every 3in american style press brake die to demanding industrial standards. By maintaining total control over our advanced tooling manufacturing process, we deliver hardened press brake tooling that eliminates springback variations and guarantees repeatable bending accuracy.
6-Step Precision Manufacturing Workflow
- Raw Material Inspection: We start with high-tensile AISI 4150 alloy steel billets, testing chemical composition and internal density before machining.
- Multi-Axis CNC Machining: Rough machining shapes the 3-inch V-opening, shoulder radii, and standard 0.50 in x 0.625 in tang geometry with tight tolerances.
- Vacuum Heat Treatment: Deep thermal processing relieves internal stress and establishes a ductile, high-strength core to withstand extreme tonnage.
- Induction Edge Hardening: High-frequency induction targets high-wear contact zones to achieve 55–60 HRC hardness, extending die life under continuous heavy plate bending.
- Precision Surface Grinding: CNC grinders finish every precision ground press brake lower die to a surface finish of Ra < 0.8 µm and ±0.01 mm centerline alignment.
- 100% Quality Inspection: Our strict quality control procedures utilize laser optical scanners and CMM equipment to verify all critical dimensions and angular tolerances before shipment.
Custom Geometry, Sectionalization & Engineering Support
Standard off-the-shelf tooling doesn't always match complex bending profiles or deep box-forming requirements. To handle non-standard bend allowances and high springback materials, we offer fully modified geometry built around the core design of our 3in american style press brake die.
Tailored Tooling Solutions
We engineer specialized bottom die modifications to solve tough clearance issues and severe springback challenges without compromising structural strength:
- Custom V-Angles: Precision-ground profiles available in acute 30°, 60°, and 75° V-grooves for high-strength steel and thick plate applications.
- Extended Heights & Deep Clearance: Modified overall heights that provide critical throat clearance for deep side flanges and channel bends.
- Precision Segmented Sets: Pre-cut, high-accuracy die segments designed for maximum flexibility during box, pan, and modular sheet metal forming.
For unique production requirements or non-standard press brake beds, explore our custom press brake tooling capabilities designed to fit your exact machine setup.
Fast CAD-to-Tooling Workflow
We keep project lead times short by integrating seamless design verification right into the ordering process:
- Direct File Upload: Submit 2D or 3D native files in DXF, DWG, or STEP formats.
- Engineering Review: Our team completes a full feasibility check, shoulder radius evaluation, and tonnage calculation within 24 hours.
- Rapid Manufacturing: Once validated, your custom lower dies transition straight into multi-axis grinding through our specialized custom tooling development pipeline.
Technical FAQ: 3in American Style Press Brake Die
Is this 3-inch die compatible with traditional American style press brake bed slots?
Yes. Our 3in American style press brake die features the standard 0.50 in x 0.625 in (1/2 in x 5/8 in) tang geometry. It fits directly into bed slots on Cincinnati, Accurpress, Wysong, Niagara, Chicago Dreis & Krump, LVD, and Pacific machines without modifications. If your setup requires non-standard seating, we supply custom safety pins and keyway modifications alongside our standard female press brake v-die tooling for precise sheet metal bending.
What material thickness is ideal for a 3in V-opening die?
Following the standard 8x rule (V-opening = 8 x material thickness), a 3in V-opening lower die performs best on 3/8 in (9.5 mm) mild steel plate.
| Sheet / Plate Thickness | Material Type | Bending Performance |
|---|---|---|
| 3/8 in (9.5 mm) | Mild Steel / Aluminum | Standard 8x rule ratio; optimal bend radius and balanced tonnage |
| 1/4 in (6.35 mm) | Stainless Steel / High-Yield | Over-sized V reduces springback and prevents outer flange marring |
| 1/2 in (12.7 mm) | Structural Steel | Bottoming/air bending under strict hydraulic tonnage limits |
How does CAMT ensure the die won't deform under high tonnage?
We build every single V press brake die 3 inch unit using forged AISI 4150 chromium-molybdenum alloy steel. To prevent deformation under heavy loads, we run a dual-stage heat treatment:
Deep Vacuum Treatment: Preserves core ductility to absorb continuous impact without cracking.
Induction Hardening: Hardens the critical shoulder wear radii to 55–60 HRC up to a 3 mm depth.
Can CAMT manufacture custom lengths or non-standard die angles?
Yes. Beyond standard solid rails and sectionalized sets, we custom-grind non-standard V-angles (30°, 60°, 75°, 85°) and specialized shoulder radii. For projects requiring different sizes, explore our 5/8 inch heavy-duty press brake dies or submit your 2D/3D CAD files directly to our engineering team for custom tooling.



