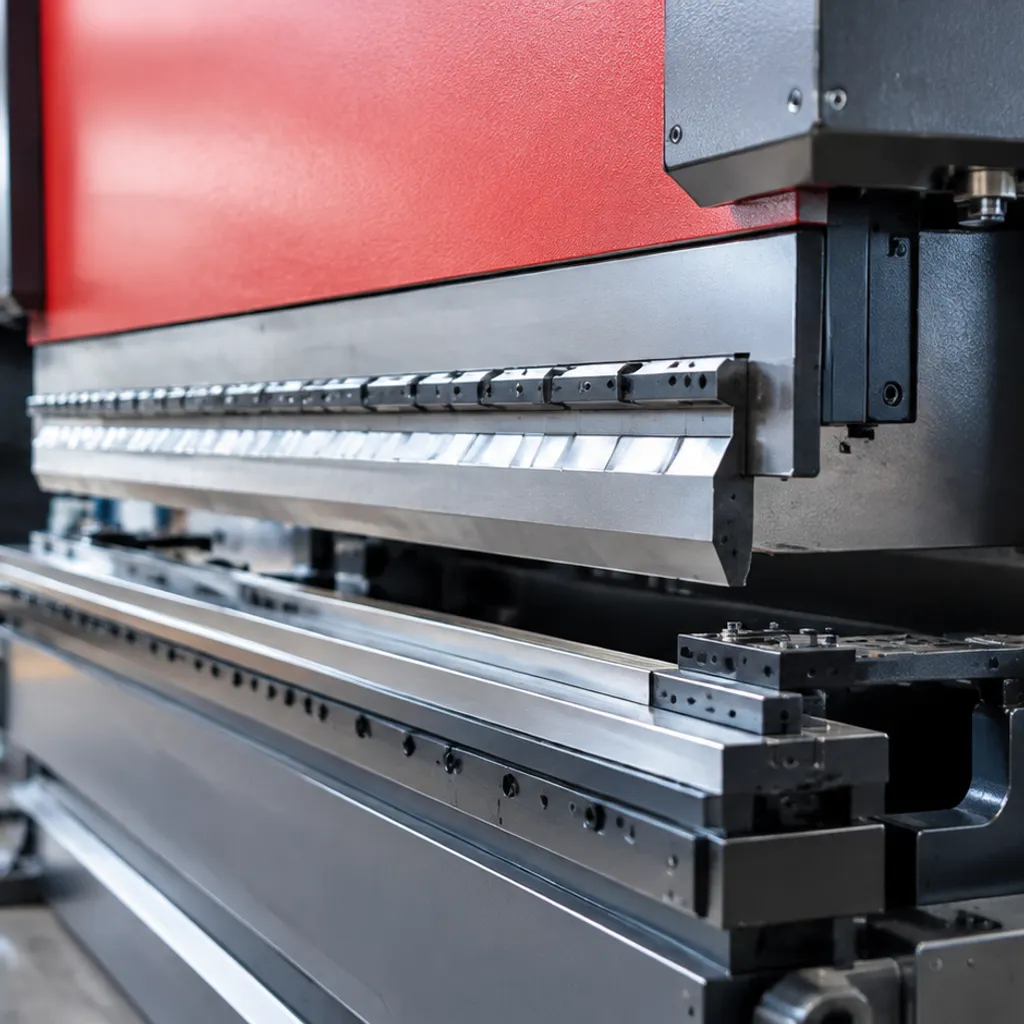
Formula details
Product Details
Overview
Bystronic Press Brake Punch Type R 30 Technical Specifications
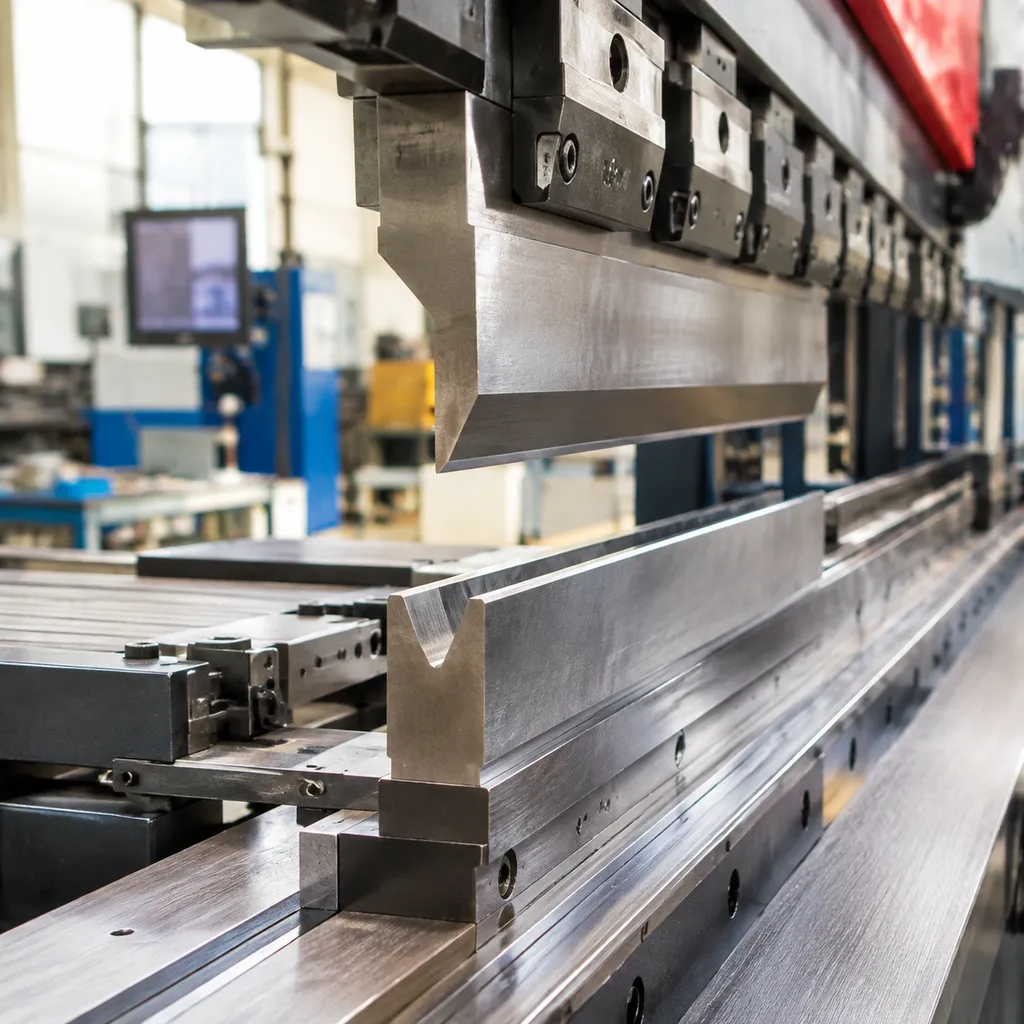
The precision bystronic press brake punch type r 30 delivers accurate large-radius bending across heavy plate and structural applications. Designed for direct compatibility with the Bystronic tooling system Type R.
| Technical Parameter | Specification Value |
|---|---|
| Punch Profile | Large radius punch (R30 mm) |
| Working Height Tolerance | ±0.01 mm for absolute line-to-line repeatability |
| Tip Radius Tolerance | ±0.02 mm CNC precision-ground profile |
| Base Material | 42CrMo / 1.7225 alloy steel |
| Core Hardness | 28–32 HRC (through-toughened core) |
| Bending Zone Hardness | 56–60 HRC via high-frequency induction hardening |
| Hardening Depth | 3–5 mm effective case depth on the working contact surface |
| Maximum Load Capacity | Up to 1000 kN/m (100 t/m) continuous operating limit |
Material Composition and Load Durability
- High-grade 42CrMo alloy: Provides outstanding tensile resilience to absorb deep-cycle bending loads without structural fatigue or body deflection.
- Deep induction treatment: Concentrated wear protection on the R30 tip prevents premature deformation when forming abrasive, high-strength structural sheets.
- Continuous tonnage limits: Engineered to handle severe air-bending forces while keeping continuous stress within safe operational margins.
Standard Tooling Lengths and Segmented Breakdown
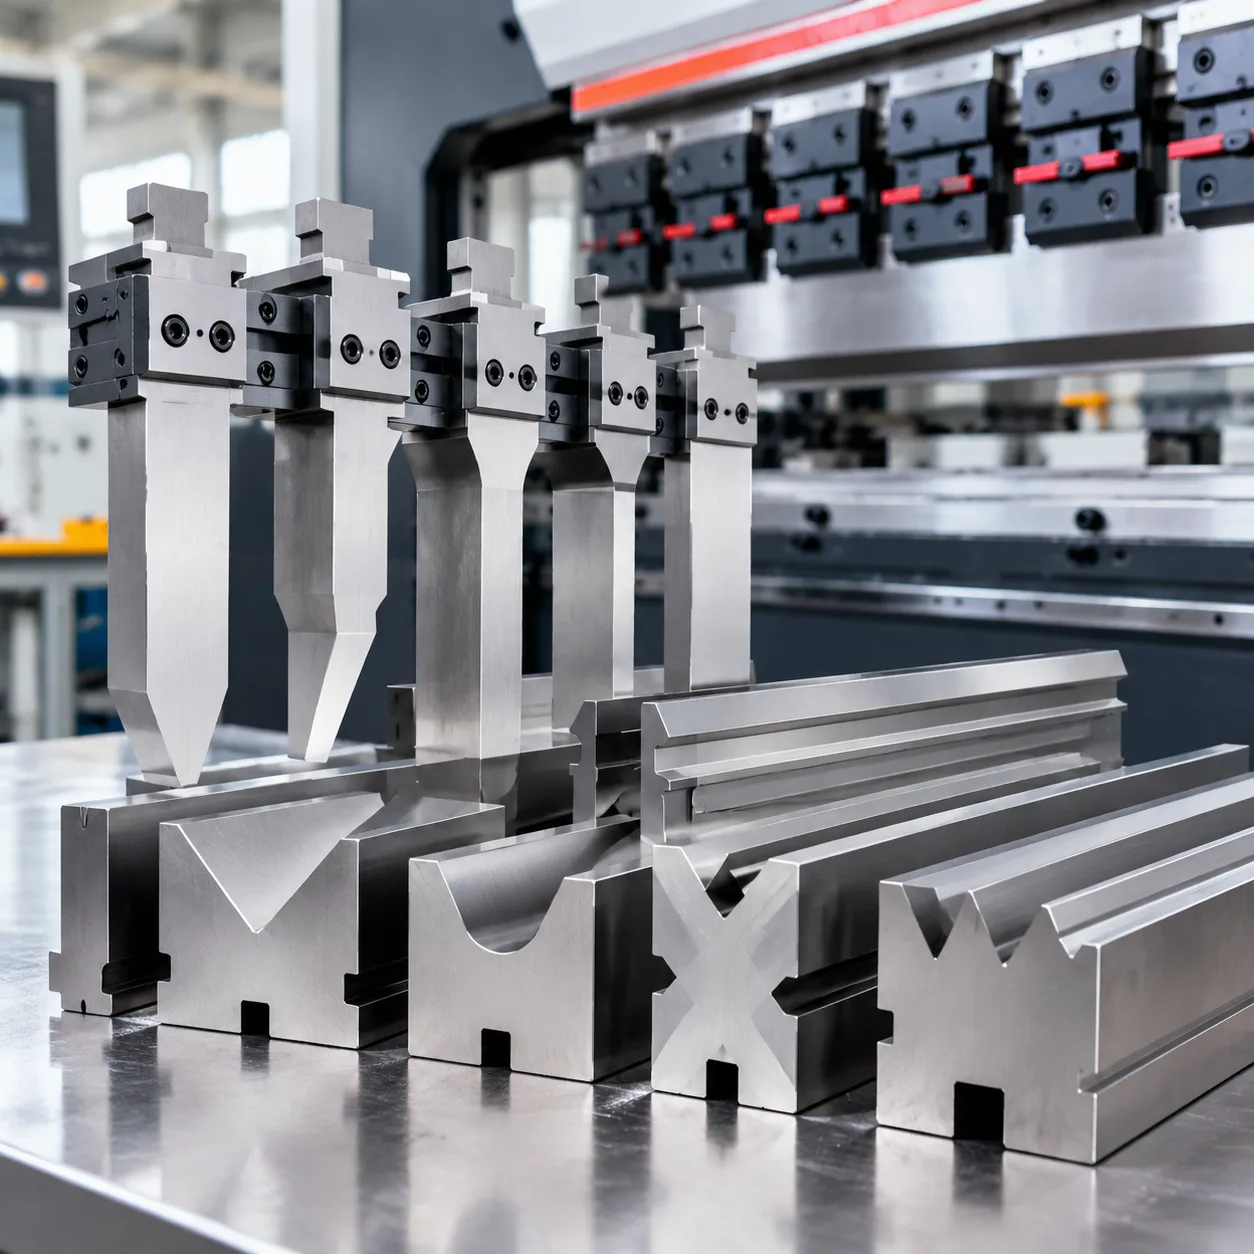
We supply the bystronic press brake punch type r 30 in both continuous single pieces and precision-matched segmented kits to support versatile job shop demands:
- Solid Stock Lengths:
- 1000 mm continuous: Ideal for full-length structural bending without segment lines.
- 500 mm solid: Excellent for mid-sized forming and standard bed configurations.
- Segmented Section Sets (550 mm Total Kit):
- Factory-matched sections: 100 mm, 50 mm, 40 mm, 25 mm, 20 mm, 15 mm, 10 mm.
- Horn sections: Left 100 mm horn and Right 100 mm horn for return flanges and deep side-relief bending.
- Every segmented piece is ground to identical height parameters, allowing tool reconfiguration across the beam with zero shimming.
Precision Bystronic Press Brake Punch Type R 30 Clamping & Fitment
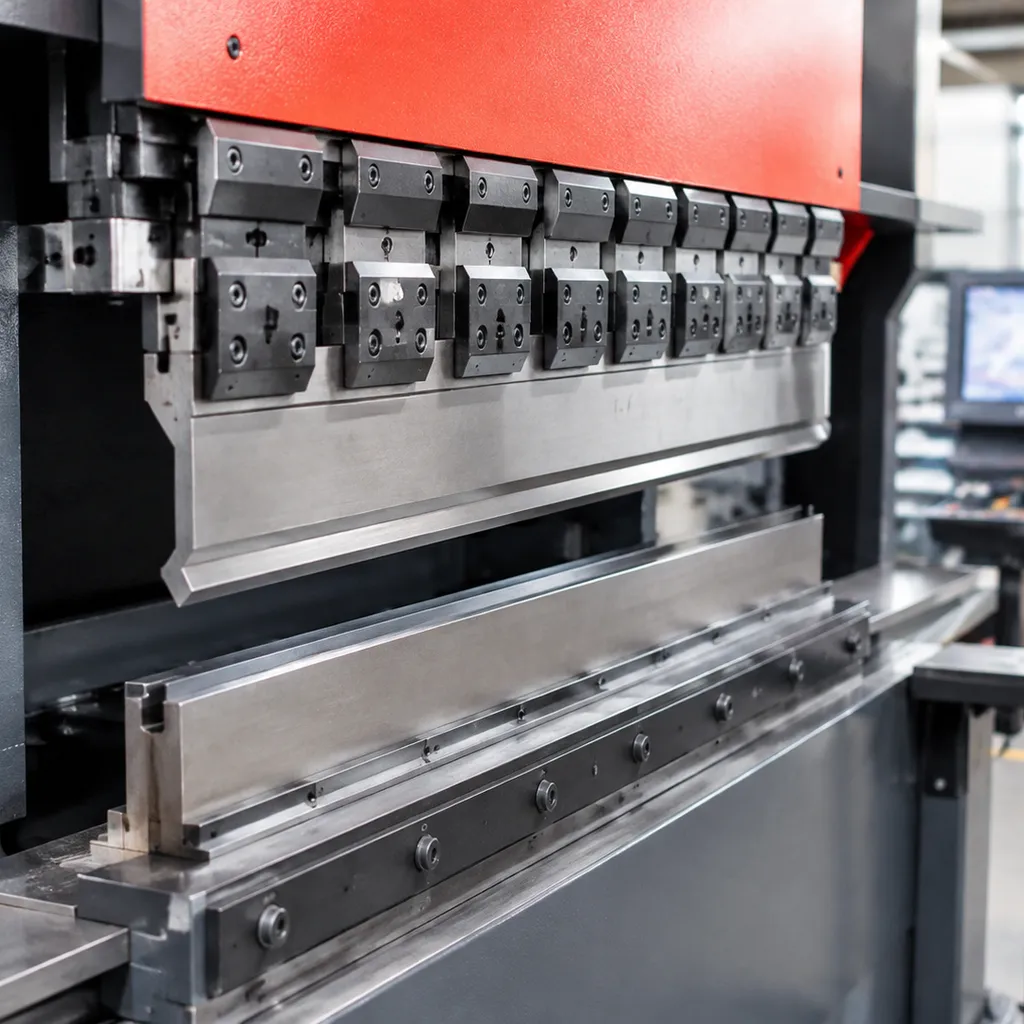
Anti-Drop Safety Tang Architecture
Tool changes need to be safe, repeatable, and fast. The bystronic press brake punch type r 30 integrates a positive-locking safety tang design:
- Self-Seating Alignment: The safety pin clicks directly into the clamping channel, allowing horizontal sliding for repositioning while preventing accidental dropouts before hydraulic pressure engages.
- Vertical Tool Loading: Segmented sections insert directly from the front into RF-A hydraulic clamps, eliminating the need to slide long tools in from the side of the machine.
- Zero Seating Drift: Under clamp pressure, the precision-ground shoulder pulls flush against the upper beam face for uniform seated height across multi-tool setups.
Machine Compatibility Matrix
Our Type R 30 radius punch functions across modern CNC platforms, older Beyeler machines, and standard Type R upper tooling configurations like our Bystronic Type R 86 compatible press brake punch.
| Machine Series | Clamping Style | Fitment Type | Setup Requirement |
|---|---|---|---|
| Bystronic Xpert | RF-A Hydraulic | Direct Drop-in | Push-button front load; instant auto-lock |
| Bystronic Xact | Mechanical / RF-A | Direct Drop-in | Direct shoulder seat via manual wedge or clamp |
| Beyeler PR / Euro | Beyeler Hydraulic | Direct Fit | Standard tang engagement; no modification |
| Non-Bystronic Rams | Euro / Amada Promecam | Retrofit Adapter | Standard Type R to European adapter rail |
Retrofit and Cross-Compatibility Options
For shops running mixed press brake fleets, we provide universal Type R adapters. These hardened conversion rails allow you to mount this heavy-duty radius punch onto standard European-style or Wila/Trumpf-style beams without sacrificing centerline accuracy or working height integrity.
Bending Capabilities of the Bystronic Press Brake Punch Type R 30
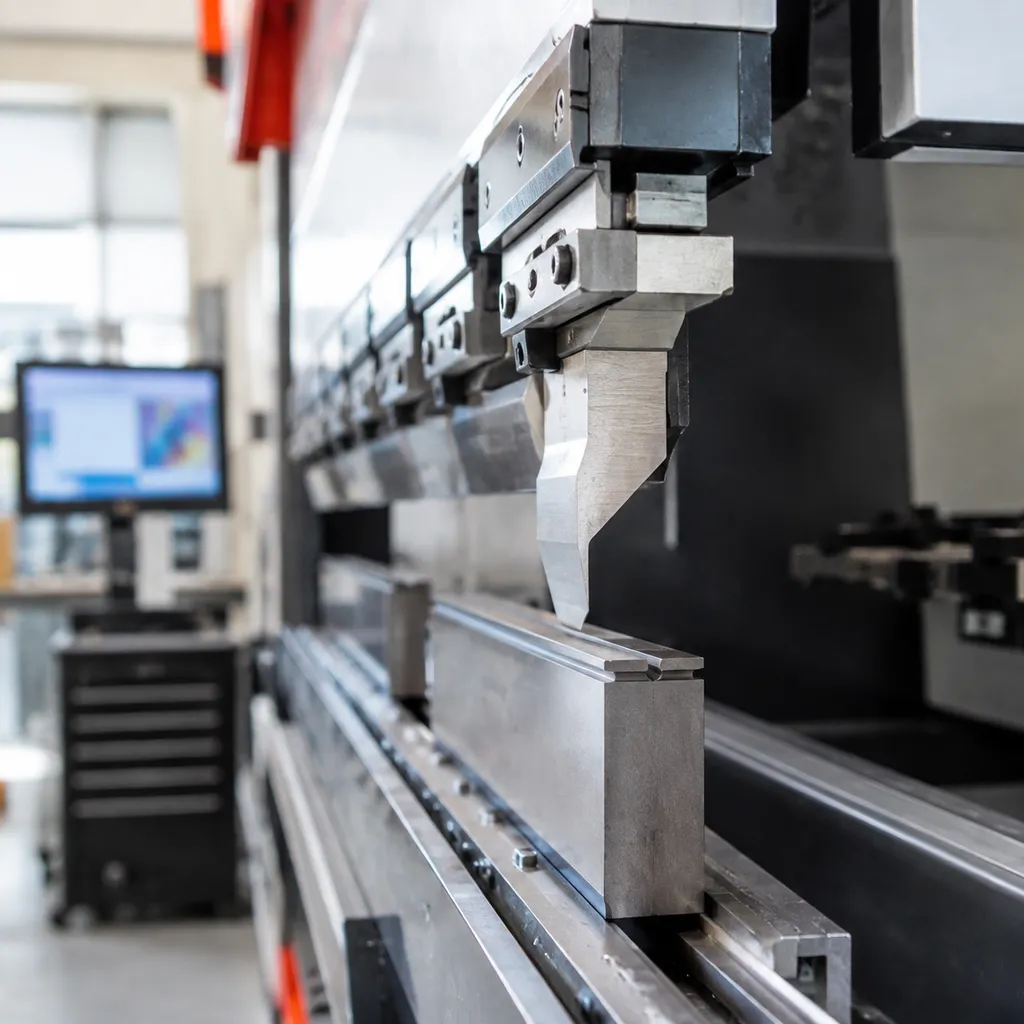
Large-Radius Forming for Structural Steel and Heavy Plate
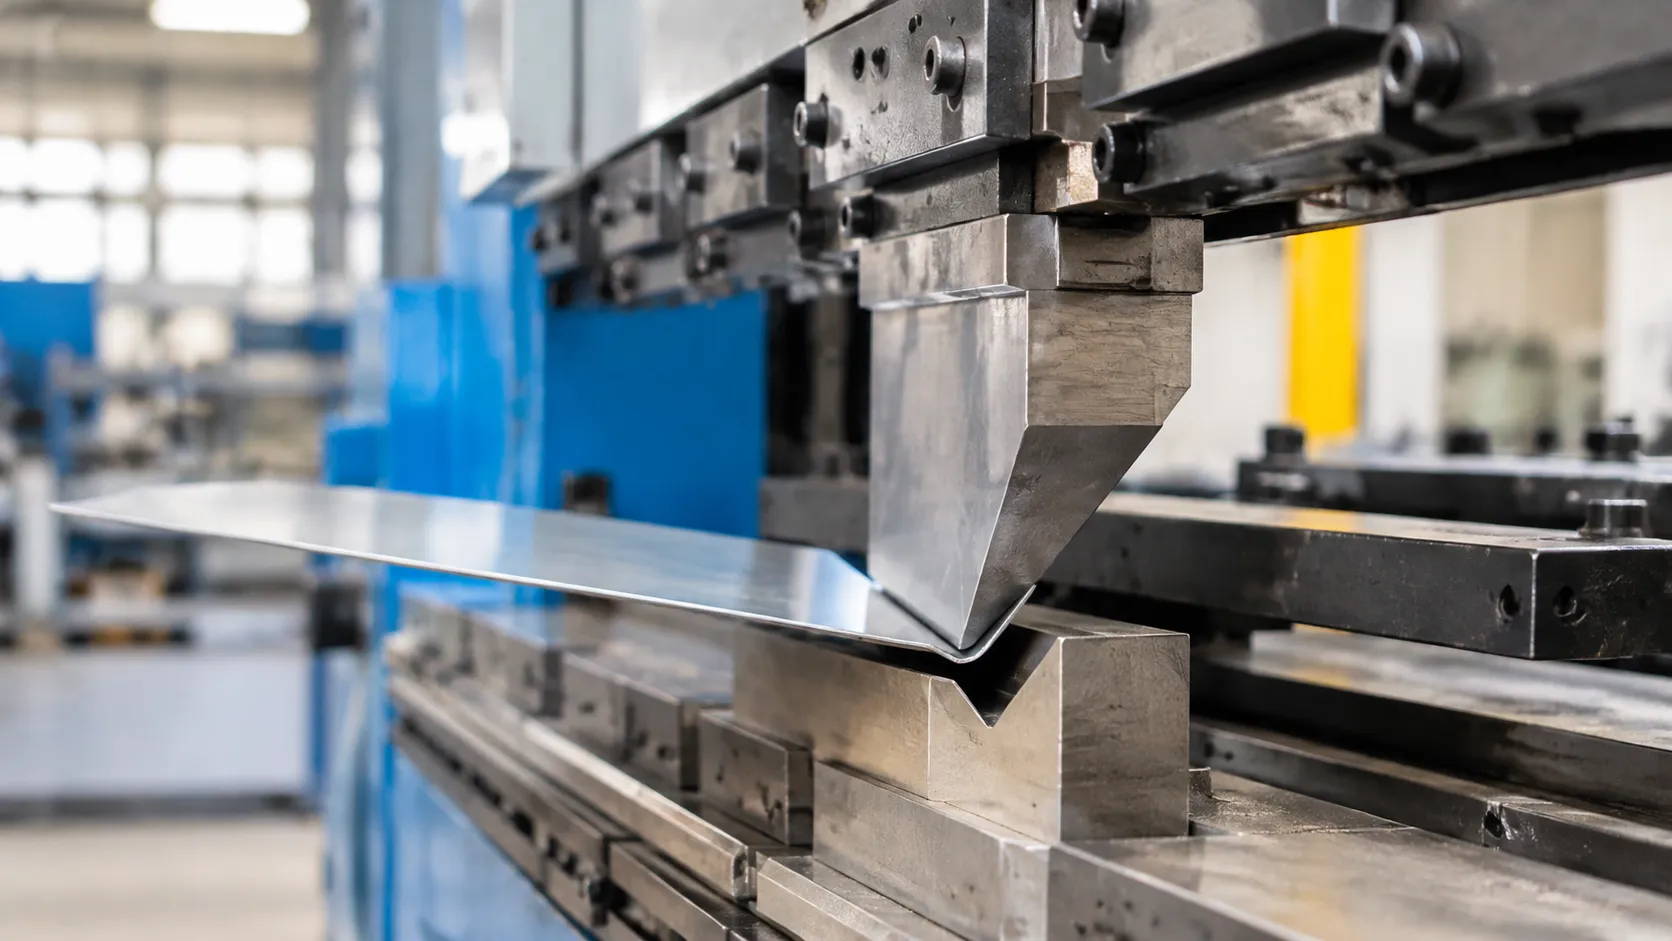
Forming high-yield plate requires generous nose radii to distribute forming pressure across a broader surface area. The Bystronic press brake punch type r 30 gives you the exact tip geometry needed for large cylindrical transitions, agricultural parts, and heavy structural brackets.
- Tonnage Spread: Distributes force along a true 30 mm radius, drastically reducing localized stress concentrations.
- Uniform Yielding: Eliminates sharp interior crease lines to keep structural plate true to print over long working lengths.
- Reduced Side Thrust: Centers downward load directly onto the machine ram for steady stroke tracking.
Cracking Prevention in High-Strength Alloys
Bending materials like Hardox, high-strength structural steel, or heavy aluminum along small bend radii routinely causes outer-fiber tearing. Using an R30 profile counters this failure mode directly:
- Expanded Neutral Axis: Relieves outer tensile stress during stroke descent, keeping high-tensile alloys below their rupture threshold.
- Grain Direction Reliability: Allows dependable bends both parallel and transverse to plate rolling grain without spiderweb fracturing.
- Elimination of Notch Stress: Keeps the inner apex rounded and smooth, preventing premature part failure in field service.
Recommended Bottom V-Die Ratios for Air Bending and Bottoming
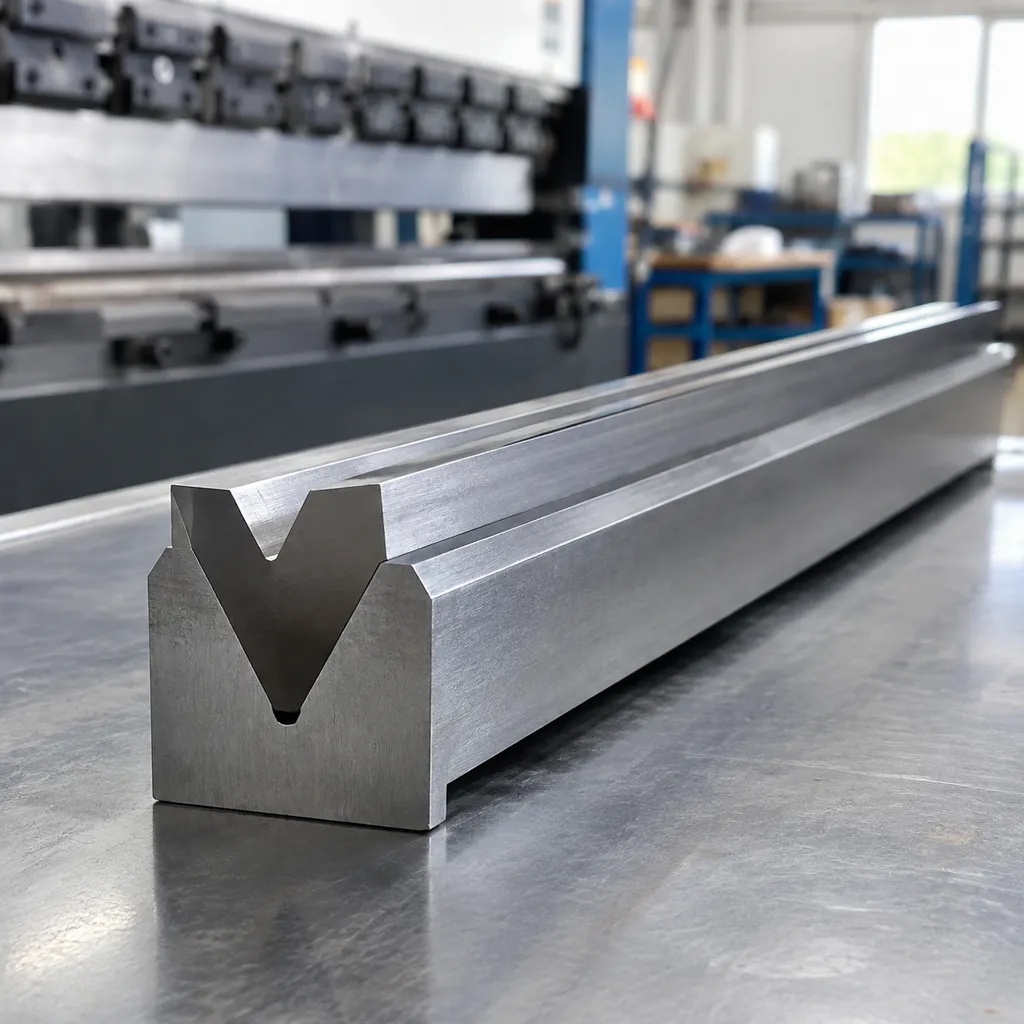
Pairing this upper punch with the right lower tooling ensures target angles without excessive tonnages. Check out our breakdown on press brake die types explained for better metal bending to select matching configurations.
- Air Bending Rule: Target a bottom V-die opening between 10× and 12× material thickness to balance punch penetration and required tonnage.
- Die Shoulder Clearance: Ensure the V-groove shoulders accommodate the sweeping R30 profile before bottom dead center.
- Bottoming Applications: Bottoming is not recommended on plate above 4 mm with this radius; air bending remains the standard practice to prevent over-tonnage trips.
Minimizing Tooling Marks Across Segmented Setups
Running segmented tool assemblies across long beds can sometimes leave step marks or cross-seam witness lines. We prevent surface marking through targeted shop-floor methods:
- Precision-Ground Shoulders: Every segment is ground to zero-clearance step tolerances, maintaining a dead-flat continuous contact arc.
- Protective Film Application: Add heavy-duty urethane tape directly across bottom die shoulders to isolate friction zones.
- Segment Clamping Sequence: Seat all upper segments loosely, lightly bottom them onto an alignment flat under low tonnage, and lock the clamps to ensure zero gap drift.
Quality Control and Precision Grinding for the Bystronic Press Brake Punch Type R 30
We hold every precision Bystronic press brake punch type r 30 to strict manufacturing tolerances so you never waste time shimming segmented setups. When you buy tools across different production batches, the working heights match seamlessly, keeping bend lines uniform from end to end.
Our workshop relies on a rigorous quality control process to guarantee that every piece of precision ground punch tooling performs straight out of the crate.
| Inspection Stage | Target Parameter | Measurement Standard |
|---|---|---|
| Working Height | Parallelism & Height Uniformity | ±0.01 mm across all segments |
| Profile Geometry | R30 Nose Radius & Centerline | Optical & Contact CMM Verification |
| Hardness Depth | Surface Hardness (56–60 HRC) | CNC induction hardened 3–4 mm depth |
| Clamping Tang | Type R Fitment Dimensions | Go/No-Go Gauge & Direct Tolerance Check |
CMM Dimensional Verification and Surface Hardening
- Profile Accuracy: We check every bystronic press brake punch type r 30 on high-precision coordinate measuring machines (CMM) to verify the radius curvature and clamping profile against factory drawings.
- Deep Case Hardening: Working tips receive controlled induction hardening to reach 56–60 HRC, providing long-term wear resistance under structural loads while keeping the core ductile to absorb shock.
- Interchangeability: Segmented tools align immediately across your ram without manual leveling or test-bend adjustments.
Corrosion Protection and Export Handling
Every finished punch undergoes ultrasonic cleaning to remove grinding residue before receiving an anti-corrosion oil barrier. We box our tools in custom heavy-duty packaging with reinforced edge shields, ensuring your tooling arrives dry, clean, and ready to lock into your machine.
Custom Profiles and CAD Simulation Support for Type R 30 Tooling
Programming complex bends without verified digital tooling models leads straight to collisions, damaged clamps, and wasted sheet metal. We supply every precision bystronic press brake punch type r 30 with exact CAD models so your programming office and brake operators work with matching data from day one.
Offline Programming Compatibility for BySoft and Delem Controllers
Offline simulation saves valuable press brake run time. We format our tooling libraries to drop right into modern CAM software without manual profile drawing:
- BySoft 7 and BySoft CAM: Native geometry profiles import smoothly, complete with verified tip centers, load-bearing shoulders, and safety tang dimensions for genuine BySoft offline simulation tooling setups.
- Delem Profile-T and DA-Touch: Full parameter integration for quick tool database entry, collision detection, and automated bend sequence calculations.
- Third-Party CAM Packages: Plug-and-play geometry files compatible with MetaCAM, Radan, and AutoPOL.
2D DXF and 3D STEP Engineering File Access
To eliminate collision risks and speed up your setup sheets, we provide complete digital datasets for every standard and segmented bystronic press brake punch type r 30:
- 3D STEP Models: Solid bodies with accurate neutral axis references and true R30 tip profiles for complete 3D machine envelope simulations.
- 2D DXF Cross-Sections: Clean, zero-gap 2D profile vectors mapped with precise working heights, load shoulders, and relief angles.
- Direct Tech Backing: If your engineering department needs custom tooling integration, check out our engineering technical support for CAD validation and simulation file packages.
Custom Horn Modifications, Relief Cutouts, and Radius Profiles
Standard upper tooling does not always clear deep return flanges or box profiles. We machine custom geometries on the Bystronic Type R platform to match your part drawings:
- Custom Left and Right Horns: Extended or undercut relief ears designed to handle deep-box side returns without punch interference.
- Window and Web Cutouts: Precision-machined clearance pockets built to clear pre-formed upright flanges and standing seams.
- Modified Tip Profiles: When special parts need unique forms outside standard R30 specs, our custom tooling development team designs, machines, and hardens bespoke Bystronic-style upper tools built to your exact specifications.
Direct RFQ Processing and Fast-Track Shipping Specs
Unplanned downtime stops production lines cold. We streamline tool ordering to keep your Bystronic presses running:
| Service Parameter | Standard Fast-Track Specification |
|---|---|
| RFQ Turnaround | Standard quote and approval prints sent within 2 to 4 business hours |
| CAD Model Dispatch | Instant access to 2D DXF and 3D STEP files upon order or RFQ confirmation |
| Stock Section Dispatch | Standard solid and segmented Type R 30 sections ship within 24 to 48 hours |
| Custom Modification Lead Time | Horn milling, custom windowing, and special radius grinds delivered in 2 to 3 weeks |
| Protective Export Crating | Heavy-duty wooden crating, anti-corrosion barrier oil, and individual segmented compartment packing |
Frequently Asked Questions About Bystronic Type R 30 Tooling
Can this punch drop directly into existing RF-A hydraulic clamps?
Yes. We grind each bystronic press brake punch type r 30 with standard Type R safety tangs engineered for direct seat engagement. Whether your machine runs standard RF-A mechanical retention bars or push-button hydraulic quick-clamping, the profile locks into the beam immediately without retrofit plates or secondary modifications.
What minimum die opening should I pair with an R30 tip?
Because an R30 profile produces large-radius forming, your bottom V-opening must clear the wide punch geometry without pinching the workpiece edges against the die shoulders.
Standard Air Bending: Maintain a V-width of at least V ge 2 × (R + T) plus safety clearance. In heavy plate, aim for a V-opening between 8 to 12 times material thickness.
Heavy Tonnage Plate: Avoid tight V-dies that cause premature bottoming or tonnage spikes. Operators running extreme plate cycles typically mate this punch with a dedicated 250-ton press brake die set for heavy metal bending to maintain proper relief angles and protect hydraulic cylinders.
How do segmented sections maintain alignment without shims?
We manufacture our precision bystronic press brake punch type r 30 segments under strict matched-height standards.
Critical contact planes, shoulders, and tip radiuses are precision CNC-ground within ±0.01 mm.
You can install segmented cuts side-by-side across the bed without step-marks, height mismatches, or manual shimming.
Routine cleaning and following basic press brake die maintenance tips for longer tool life will prevent particulate buildup between adjacent sections, ensuring perfect seams over years of tool changes.
Is 42CrMo durable enough for heavy structural plate bending?
42CrMo (AISI 4140 / 1.7225) provides the ideal balance of core resilience and surface toughness for this geometry:
High Core Toughness: The normalized, tempered core yields high tensile strength to handle intense shock loads without brittle fracture under maximum machine tonnages.
Hardened Wear Zones: We deep-harden the R30 contact radius to 56–60 HRC, stopping premature flat spots, galling, and radius flattening even when processing high-strength structural steels and heavy gauge plate.