Worn tooling, ruined bend angles, and unexpected scrap can turn a profitable shop into a money pit overnight.
If you want consistent bending precision and maximum tool lifespan, proactive press brake die maintenance isn't optional—it's essential.
In this complete guide, you're going to learn the exact step-by-step routines to protect your high-precision investment. We'll cover everything from daily cleaning protocols and precision wear inspections to proper lubrication techniques and safe tooling storage solutions.
Let's dive in and keep your dies running like brand new.
The Critical Role of Press Brake Die Maintenance
Shop floor operators and fabricators constantly struggle with unexpected angular variance, rising scrap rates, and premature tool failure. When bend accuracy drifts, the root cause is rarely the press brake itself—it is almost always inadequate press brake tooling maintenance. Running dirty, misaligned, or worn dies degrades part quality and places unnecessary strain on your machinery.
The High Cost of Tooling Neglect
Ignoring routine care creates a compounding financial drain on your metal fabrication operations:
- Scrap Parts & Material Waste: Embedded mill scale, metal dust, and micro-contaminants alter critical V-groove dimensions, creating erratic bend angles across the workpiece.
- Angular Variance: Worn die shoulders force operators to constantly recalibrate ram depth, ballooning setup times and ruining throughput consistency.
- Machine Ram Damage: Operating with damaged or unevenly worn dies creates asymmetrical load distribution, damaging press brake ram guides, crowning systems, and hydraulic cylinders.
Extending Service Life and Bending Accuracy
Systematic maintenance transforms your punches and dies from disposable consumables into long-term precision assets. Implementing structured daily and weekly maintenance protocols yields measurable productivity gains:
| Maintenance Strategy | Tooling Longevity | Bending Accuracy Alignment | Machine Ram Strain |
|---|---|---|---|
| Reactive / Neglected | Baseline Service Life | Frequent Angular Drift | High (Risk of Ram Tilt) |
| Proactive / Systematic | Up to 3x Tool Life | Consistently ±0.01 mm | Minimal & Evenly Distributed |
The CAMT Standard for Induction Hardened Tooling
High-performance tooling requires precision-level care. Under the CAMT Standard, our high-precision tooling is engineered from premium alloy steel featuring deep induction hardened die edges rated at 55–60 HRC working edge hardness.
While this extreme tool steel hardness provides exceptional resistance against structural deformation and shoulder wear under heavy tonnage, extreme hardness demands proactive maintenance. Hardened working edges must remain free of abrasive particulate, scale buildup, and misalignment stresses. Protecting these critical contact surfaces preserves precision geometry, guarantees repeatable bending accuracy alignment, and maximizes return on investment across every shift.
Daily & Pre-Shift Maintenance Protocols
A quick pre-shift routine protects high-precision tooling and prevents costly material scrap. Taking five minutes before each shift guarantees consistent bend accuracy and protects machine components.
Visual Edge and Clamp Channel Inspection
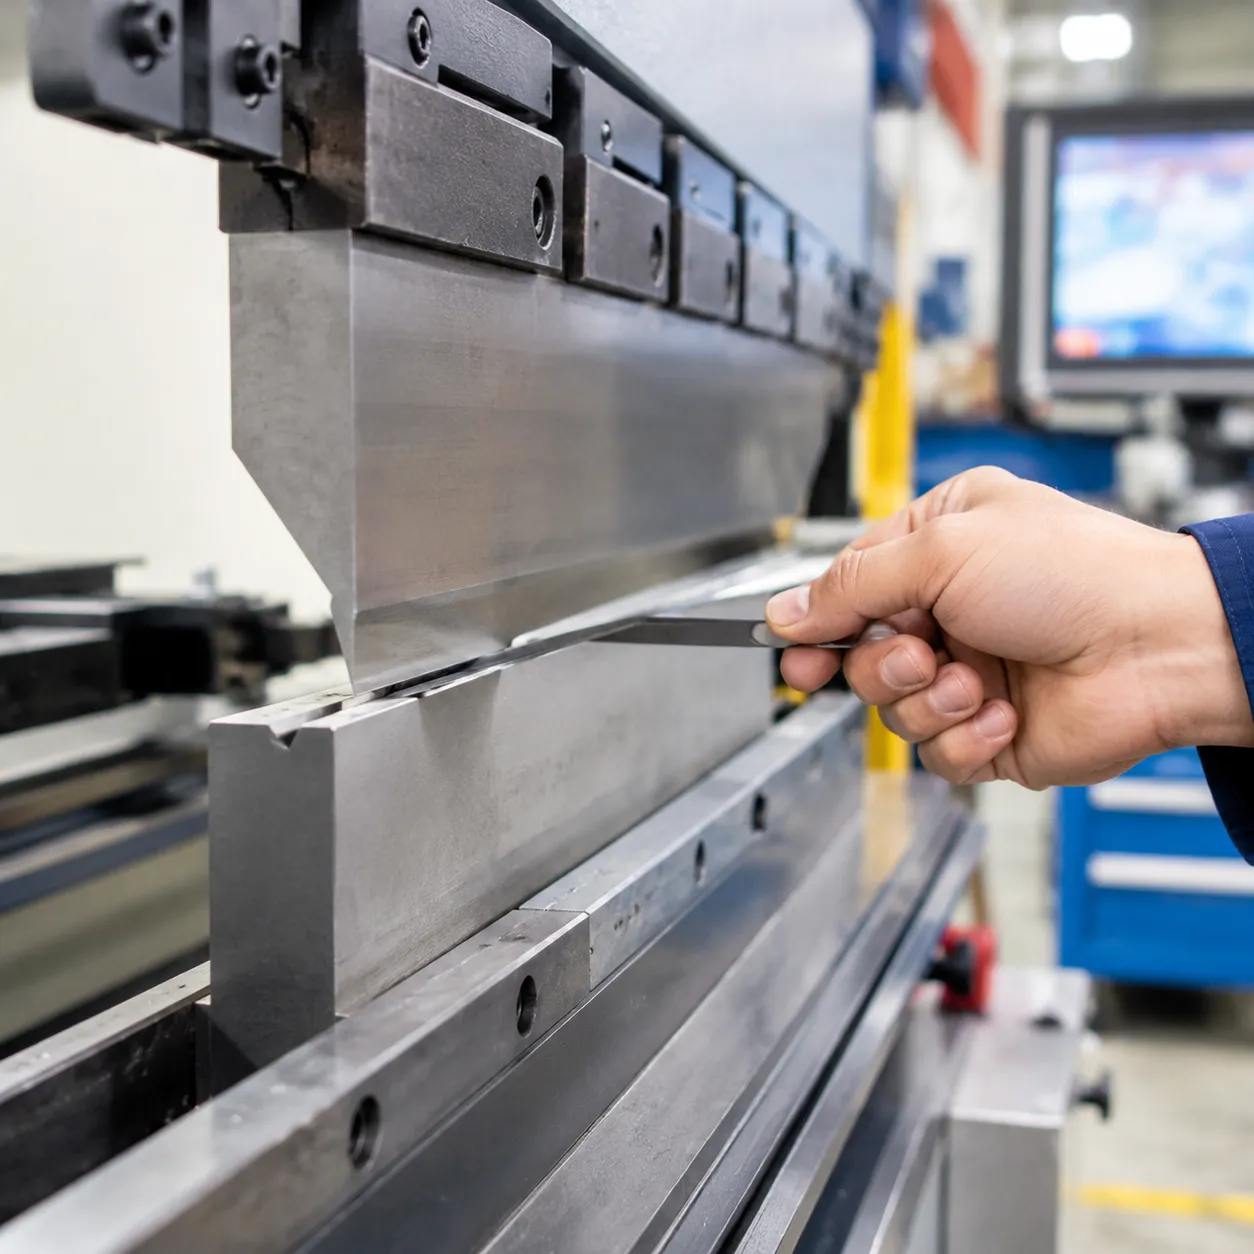
- Press brake punch inspection: Inspect tip radii under bright light for micro-cracks, edge chipping, or localized wear patterns before securing tools into the ram.
- Upper clamp channel cleaning: Wipe down upper seating channels to remove metal scale and burr buildup that prevent tooling from seating flush against the ram.
- Tooling integrity: Tag and remove any sectioned punch or die exhibiting stress fractures immediately.
V-Groove Surface Cleaning Procedures
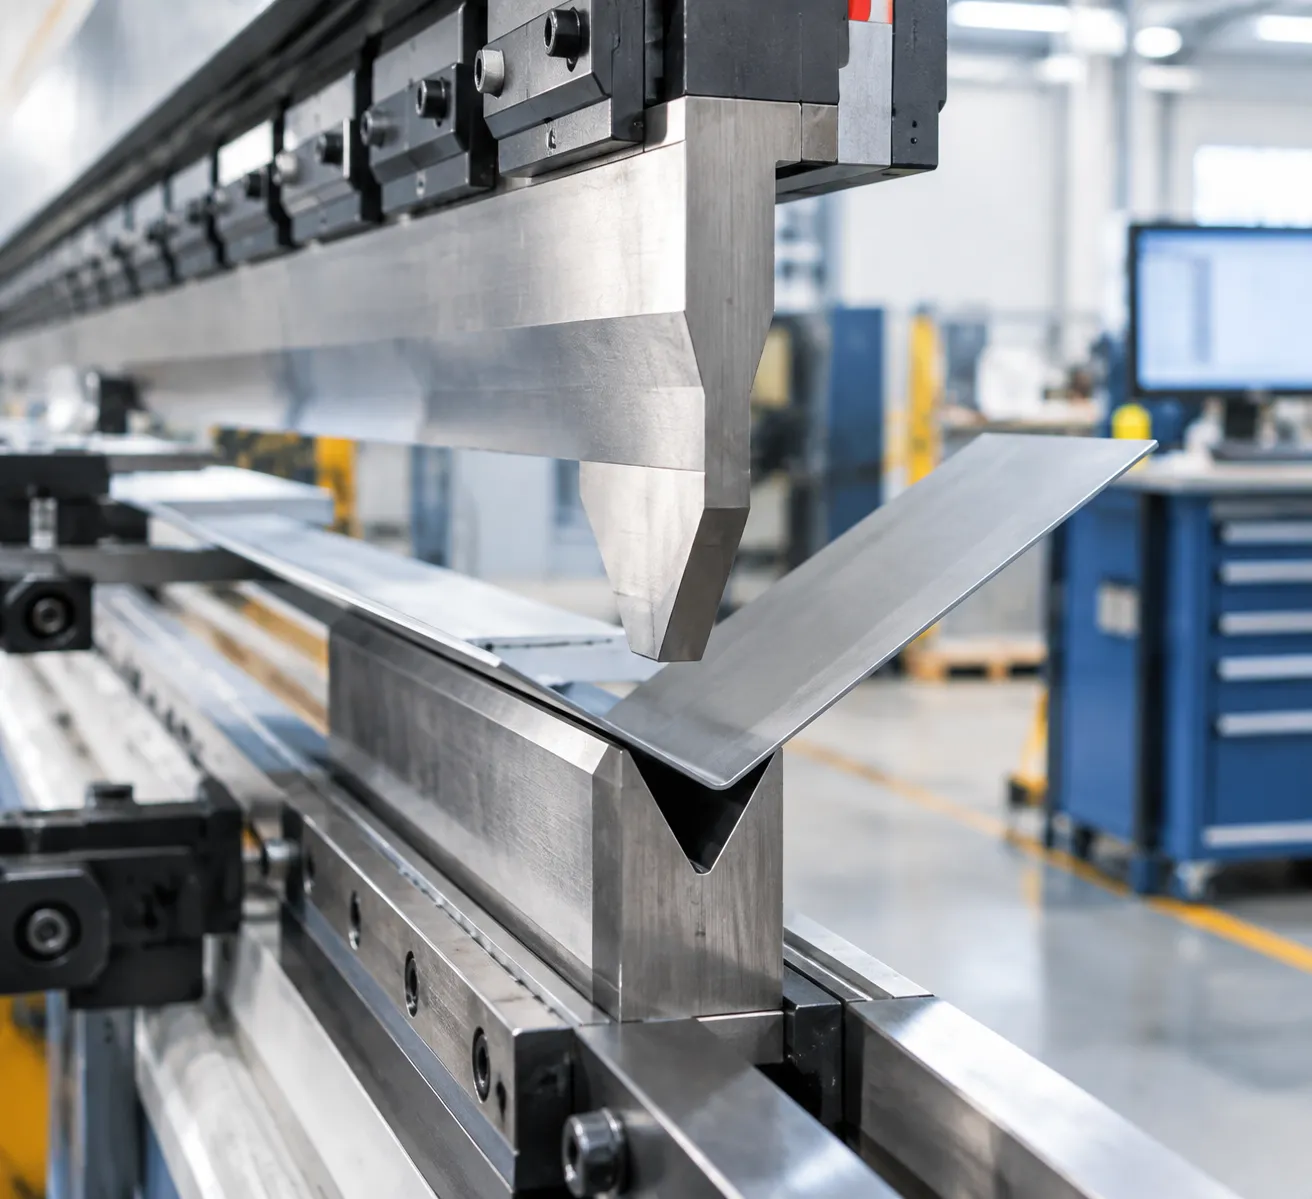
Accumulated debris inside V-grooves acts as an abrasive compound during the stroke. When preparing a female press brake V-die for precise sheet metal bending, we follow a strict cleaning standard to maintain low surface roughness:
| Cleaning Stage | Protocol | Standard / Target |
|---|---|---|
| Debris Removal | Clear away mill scale, metal dust, and shop grime | Wipe clean with lint-free shop towels |
| Degreasing | Remove oxidized oils and chemical contaminants | Apply solvent degreaser to working V-grooves |
| Surface Finish Verification | Ensure pristine contact surfaces to eliminate cosmetic part scratching | Maintain surface roughness Ra < 0.8 µm |
Pre-Operation Friction Reduction
Applying pre-operation protection lowers sliding friction during the stroke and keeps workpieces free of galling marks.
- Apply non-gumming lubricants: Coat lower die shoulders with a thin layer of non-gumming protective lubricant before starting air bending operations.
- Friction management: Lubricating contact points on specialized tooling, such as a 30-degree press brake die for air bending and hemming, smooths material flow into the V-opening and minimizes wear on shoulder radii.
- Targeted application: Avoid over-spraying lubricant onto upper clamping faces where hydraulic or mechanical grip requires maximum surface contact.
Operational Best Practices to Prevent Tooling Overload
Overloading tooling during air bending or bottoming is the fastest way to permanently deform lower dies, micro-fracture punch tips, and compromise machine ram alignment. We strictly enforce load management protocols to preserve precision tolerances and prevent structural tooling damage on the shop floor.
Bending Tonnage Limit Calculation
Never estimate bending force by eye. Always calculate maximum load limits per meter to ensure your operational pressure remains safely under the yield strength of the tool steel.
For standard air bending of mild steel (420 N/mm² tensile strength), apply the standard bending force formula:
P = (650 × S² × L) / V
- P: Bending force (kiloNewtons, kN)
- S: Sheet metal thickness (mm)
- L: Sheet length (meters)
- V: V-die opening width (mm)
For stainless steel, multiply the calculated tonnage P by 1.5. For high-tensile aluminum alloys, multiply by 0.5. Refer to our comprehensive European press brake die tonnage rating guide to verify load limits across different tool profiles before running high-tonnage jobs.
V-Opening Selection Standards
Matching sheet thickness to the correct V-opening ratio lowers required tonnage, minimizes shoulder friction, and prevents center-line load concentration.
- Standard Mild Steel: 8x Rule (V = 8 × S) provides the optimal balance between required force and bend radius.
- Thin Sheets (< 1.5 mm): 6x Rule (V = 6 × S) ensures tight bend radii without sheet slipping.
- High-Tensile & Heavy Plate: 10x–12x Rule (V = 10 to 12 × S) widens the load distribution area to prevent shoulder cracking and lower die seat crushing.
Stainless Steel Galling Prevention & Cosmetic Protection
Bending high-tensile alloys and stainless steel creates intense friction that forces metal pickup onto hardened die shoulders. Unchecked galling damages both the tool profile and subsequent workpieces.
- Clean Die Shoulders: Wipe down shoulder radii with solvent every shift to prevent micro-particulates from pressure-welding onto the working edge.
- Apply Protective Barriers: Use heavy-duty anti-galling lubricants or specialized films across the V-die opening.
- Integrate Non-Marking Inserts: Protect architectural stainless steel, aluminum, and pre-painted panels by equipping your press brake bed with custom polyurethane tooling pads, eliminating steel-on-steel contact and part scratches.
Periodic Inspection & Precision Verification
CMM Dimensional Verification & Profile Audits
Over thousands of cycles, localized wear subtly alters die geometry. We track these changes systematically using non-contact and tactile measurement tools:
- Tip Radii & Height Tolerances: We utilize optical projectors and Coordinate Measuring Machines (CMM) for precision punch inspection. Verifying profile deviations against a standard press brake die size chart and dimensions guide prevents angular variances across staged tooling setups.
- Profilometer Surface Testing: Quantitative profilometer testing monitors V-groove wear over time, ensuring shoulder roughness stays below Ra 0.8 µm to eliminate cosmetic scoring.
| Inspection Parameter | Target Metric | Verification Method | Action Trigger |
|---|---|---|---|
| Height & Radius Tolerance | ±0.01 mm | CMM / Optical Comparator | Schedule precision regrinding |
| Surface Finish | Ra < 0.8 µm | Digital Profilometer | Polish V-groove shoulders |
| Working Edge Hardness | 55–60 HRC | Portable Hardness Tester | Retire section if core soft spots appear |
| Bed-to-Ram Parallelism | < 0.02 mm full length | Dial Indicator / Laser System | Re-calibrate crowning hydraulic system |
Hardness Integrity & Bed Alignment
- Hardness Integrity Verification: We regularly audit critical working edges to confirm tool steel hardness remains at 55–60 HRC. Spikes in friction heat can soften working shoulders, accelerating material pickup and shoulder deformation.
- Bed & Ram Calibration: Uneven die wear is often a symptoms of machine mis-calibration. We audit ram parallelism and crowning system accuracy monthly to guarantee uniform tonnage distribution across the entire bed length.
Tooling Storage & Environmental Preservation
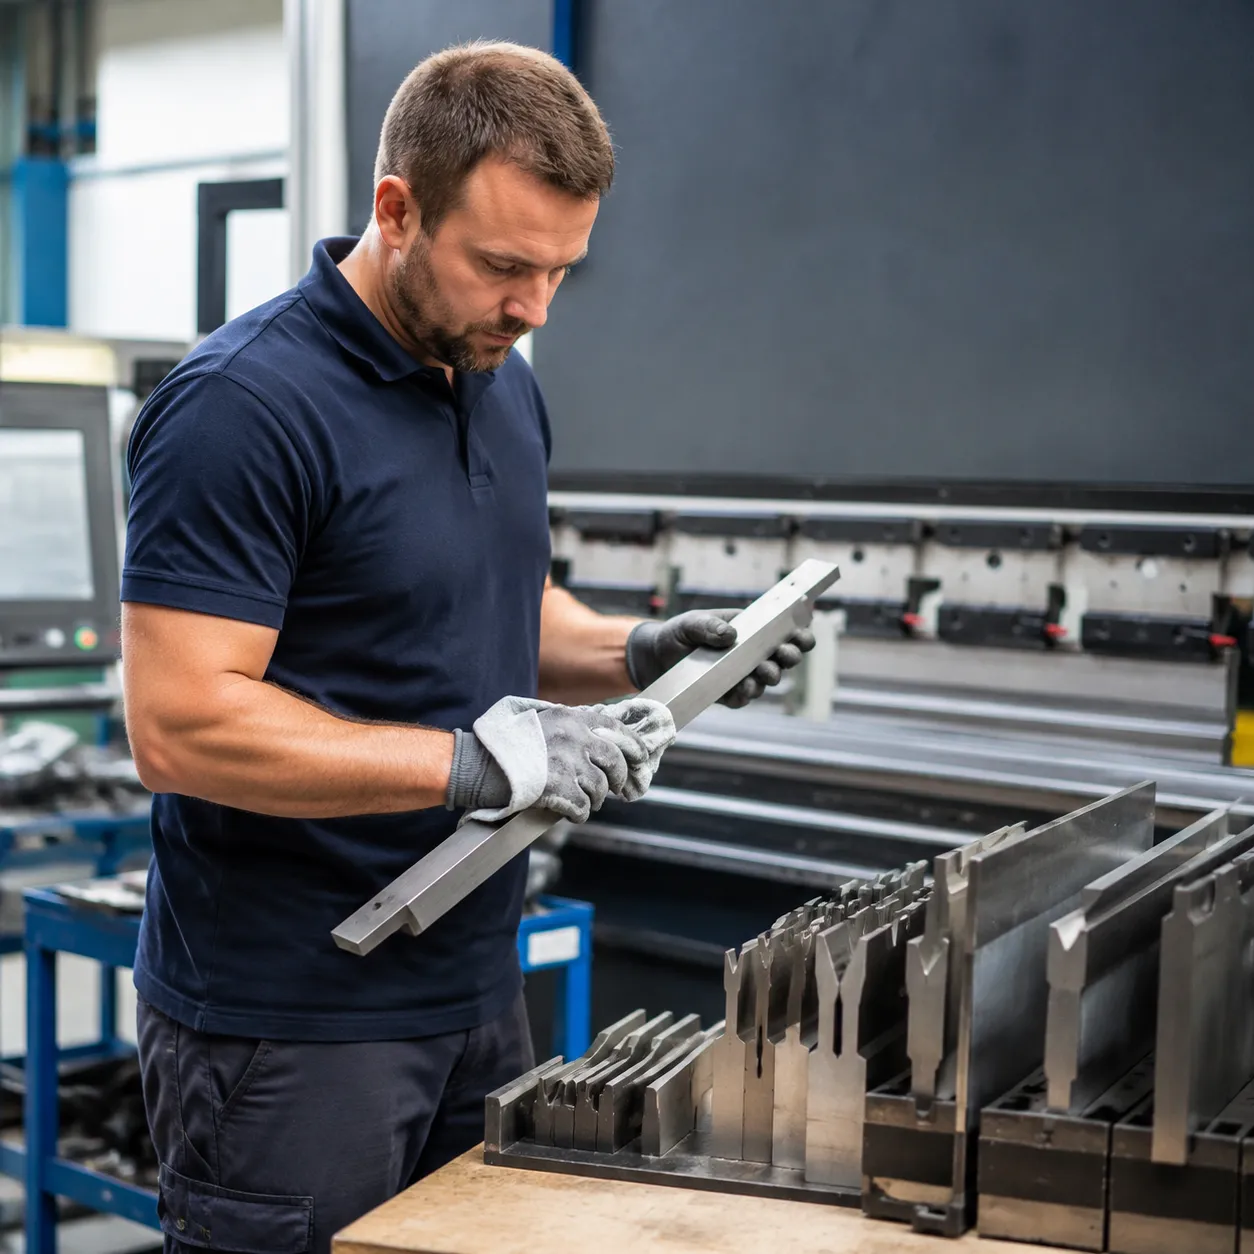
Moisture, concrete dust, and improper handling can ruin precision-ground surfaces faster than thousands of bend cycles.
Shop Floor Climate Control
- Target Humidity: Maintain shop floor and toolroom relative humidity between 40–60% with stable ambient temperatures to eliminate condensation risks.
- Isolate from Concrete Floors: Never place tooling directly on bare concrete. Concrete holds moisture and leaches raw humidity into high-carbon alloys; always store tools on wood, high-density polyethylene, or lined metal shelving.
Press Brake Die Storage Cabinets
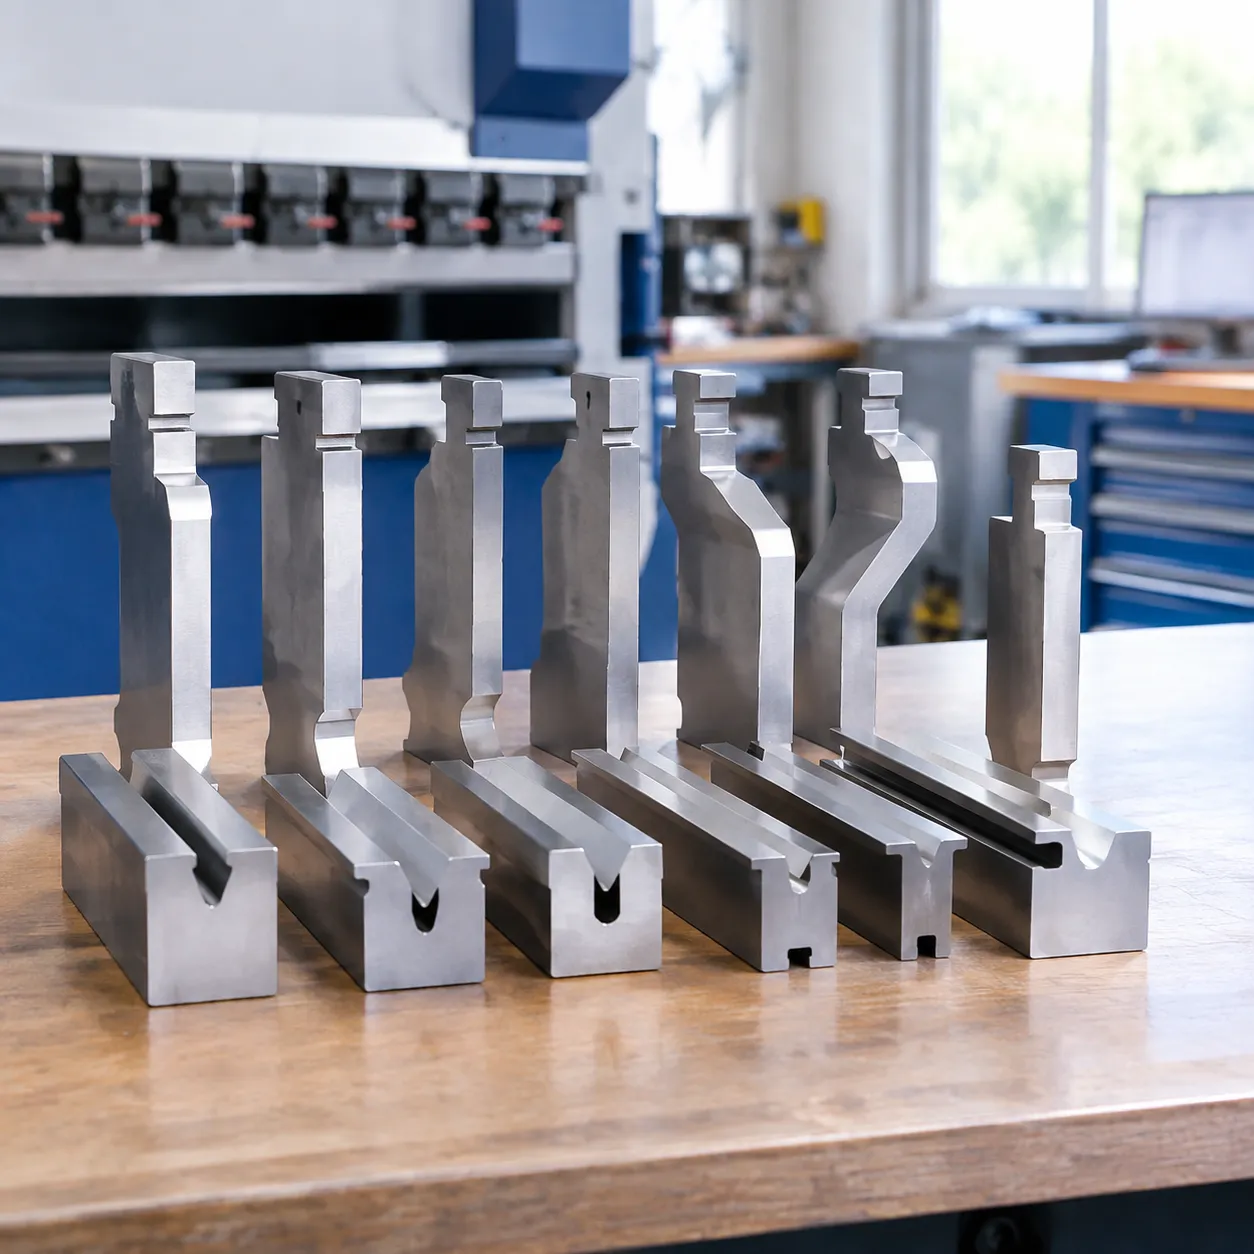
- Dedicated Racking System: Store sectioned punches vertically and dies horizontally inside industrial press brake die storage cabinets.
- Edge Separation: Use custom high-density foam or polyurethane dividers to keep tool segments separated. Preventing metal-to-metal contact protects the precision radii of premium press brake dies from nicking, chipping, or burr formation.
Anti-Rust Preservation & Transit Protection
- Anti-Rust Oil Treatment: Apply a dedicated solvent-based, non-gumming anti-rust oil treatment over clean V-grooves and seating surfaces before transferring tools to long-term storage or during seasonal downtime.
- Export-Grade Wrapping: For tooling transit and long-distance shipping, wrap both standard and custom dies in heavy-duty Vapor Corrosion Inhibitor (VCI) film and seal them inside vacuum-packed, moisture-resistant wooden crates.
Precision Die Regrinding Guidelines
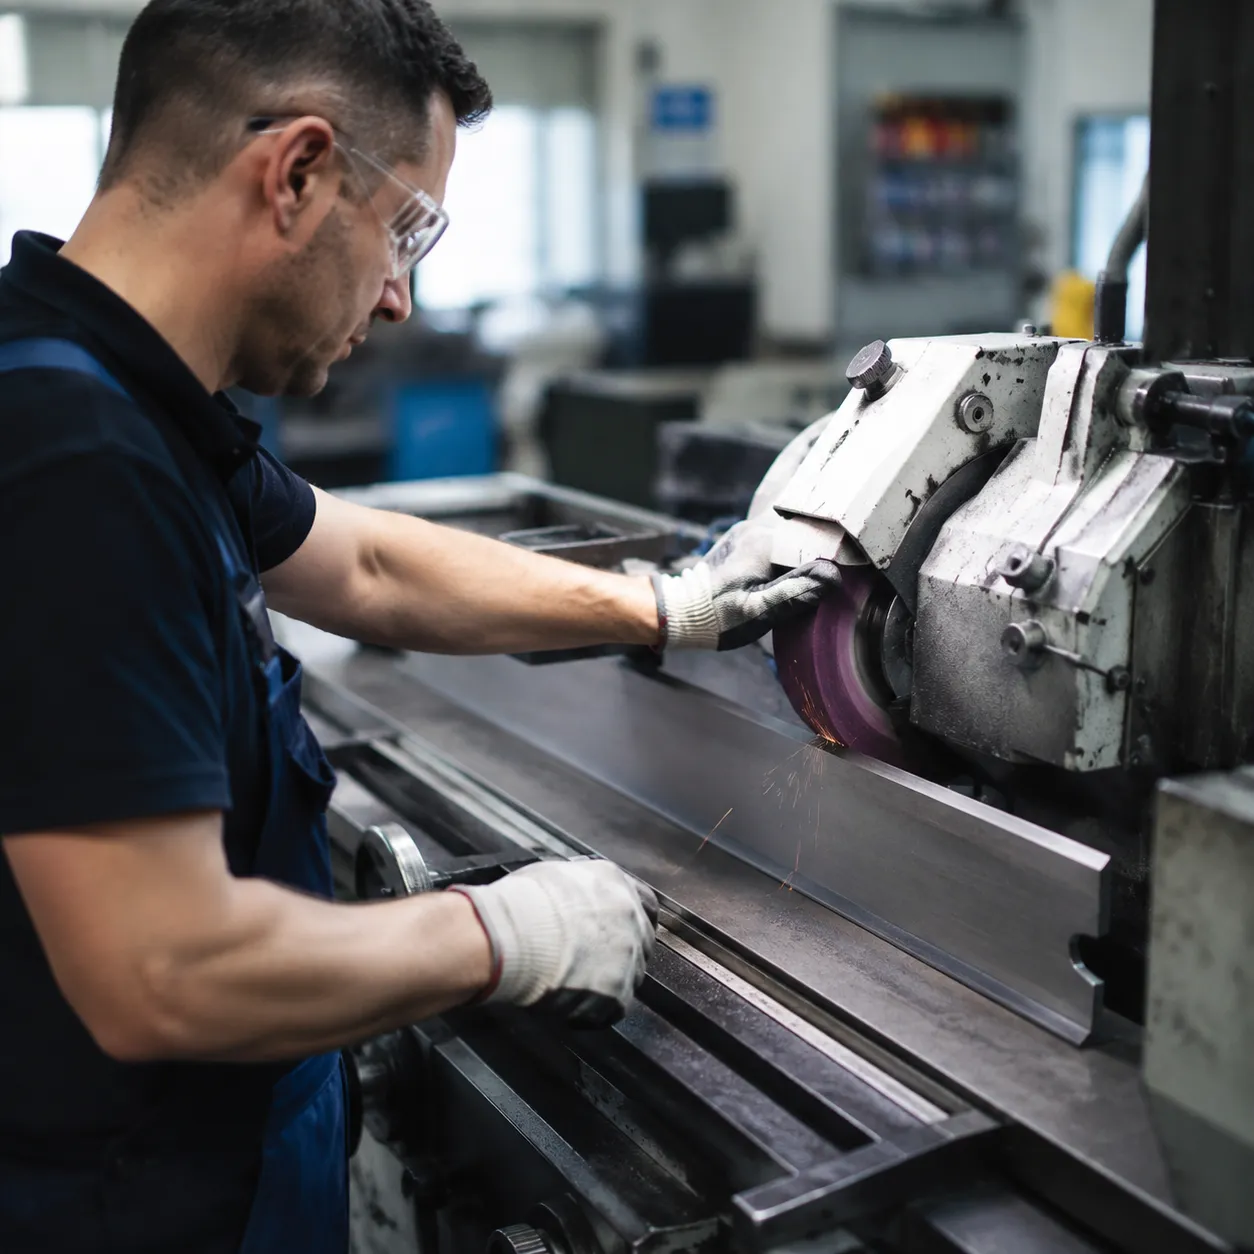
We use a strict decision framework to determine whether worn tooling can be restored through die sharpening and grinding or if full replacement is required.
- Regrind in Matched Sets: Always regrind matching punch and die sets simultaneously. Grinding a single component creates shut-height discrepancies along the ram, resulting in severe angular variations across the bend line.
- Preserve Hardened Case Depth: Limit grinding to surface wear depth. Grinding past the induction-hardened layer exposes soft core metal, causing rapid edge degradation.
- Maintain Full-Bed Parallelism: Process full-length tools on precision surface grinders to preserve height uniformity across the entire press brake bed.
Tooling Retirement Criteria
When structural integrity is compromised, press brake die maintenance can no longer guarantee safe or accurate production. Scrap tooling immediately if any of these conditions are met:
| Wear Parameter | Failure Threshold | Operational Impact |
|---|---|---|
| Hardness Loss | Surface hardness falls below 55 HRC | Accelerated shoulder wear and material galling |
| Micro-Fractures | Edge chipping or micro-cracks detected under inspection | Immediate risk of tool splitting under tonnage load |
| Tang Distortion | Permanent deformation on upper clamp seating surfaces | Uneven load distribution and potential ram damage |
| V-Groove Spacing | Shoulder wear expanding V-opening beyond ±0.02 mm | Uncontrollable angle variance and part scrapping |
Upgrading to Drop-In Precision Tooling
Once a tool crosses these retirement thresholds, further regrinding degrades bend quality. Upgrading to our high-precision American and European style press brake dies restores your machine to factory-level ±0.01 mm bend accuracy without time-consuming shimming or trial bends.
We manufacture drop-in precision dies for European, American, and New Standard press brake systems. Deep induction hardening across all primary contact surfaces ensures our replacement tooling stands up to high-tonnage production runs straight out of the box.
Frequently Asked Questions About Press Brake Die Maintenance
How often should press brake dies be cleaned and inspected?
We recommend cleaning working surfaces daily before shift startup. We perform a thorough press brake punch inspection and die check weekly, or immediately following any accidental over-tonnage event.
- Daily: Wipe down V-grooves and seating channels to remove mill scale, metal shavings, and shop debris.
- Weekly: Perform optical profile checks and inspect working edges for micro-cracks or shoulder burrs.
- Monthly: Verify working edge hardness (55–60 HRC) and overall dimensional alignment across the press bed.
What causes micro-cracking and edge chipping on V-dies?
Micro-cracks and edge chipping stem primarily from structural overload and improper tool setup:
- Exceeding Tonnage Limits: Concentrating high bending force over a short bed length deforms induction-hardened die edges.
- Incorrect V-Opening Selection: Forcing thick plate into an undersized V-groove severely spikes lateral force on die shoulders. Review our press brake die selection guide to ensure you match your material thickness to the correct V-opening.
- Debris Contamination: Metal scale trapped between the workpiece and die shoulder creates concentrated point loads.
How do you prevent rust and ambient oxidation on precision tooling?
Controlling the shop floor environment and applying surface protection prevents corrosion from ruining tight tolerances:
- Climate Control: Store sectioned punches and dies in dedicated press brake die storage cabinets with relative humidity maintained between 40–60%.
- Anti-Rust Application: Apply a light layer of protective anti-rust oil to ground working surfaces during downtime or long-term storage.
- Safe Handling: Wipe down tooling after handling to eliminate perspiration moisture and skin oil residues.
When should a press brake die be reground instead of replaced?
Precision die regrinding is ideal when localized surface wear affects bending accuracy alignment while core structural integrity remains intact.
- Regrind: When shoulder wear is uniform, micro-cracks are absent, and matching punch and die sets can be reground together to preserve shut-height consistency across the machine bed.
- Replace: Retire tooling immediately if you identify non-recoverable structural fractures, deep micro-cracks, or compromised hardness zones. When severe wear threatens production quality, upgrading to new heavy-duty press brake tooling ensures your press brake maintains precise tolerances.