

Formula details
Product Details
Overview
7 Inch Press Brake Tooling: Precision Profile Engineering
High-Tonnage Bottom V Die Manufacturing Standards
We manufacture every bottom V die and punch profile to strict metallurgical and dimensional tolerances:
- Dimensional Tolerance: Precision-ground to within ±0.01 mm across profile lengths to ensure flawless angle consistency along the entire bend line.
- Working Edge Hardness: Localized deep induction hardening delivers HRC 55–60 on primary contact points, while the core body maintains HRC 47–50 for optimal shock absorption and fatigue resistance.
- Surface Finish: Fine-ground profile finish achieving a surface roughness of Ra < 0.8 µm, significantly reducing die marks on aesthetic stainless steel and aluminum parts.
- Tooling Life: Delivers up to 3× extended wear life compared to conventional, unhardened carbon steel dies under continuous production.
Technical Specifications for Press Brake Die 7 Inches
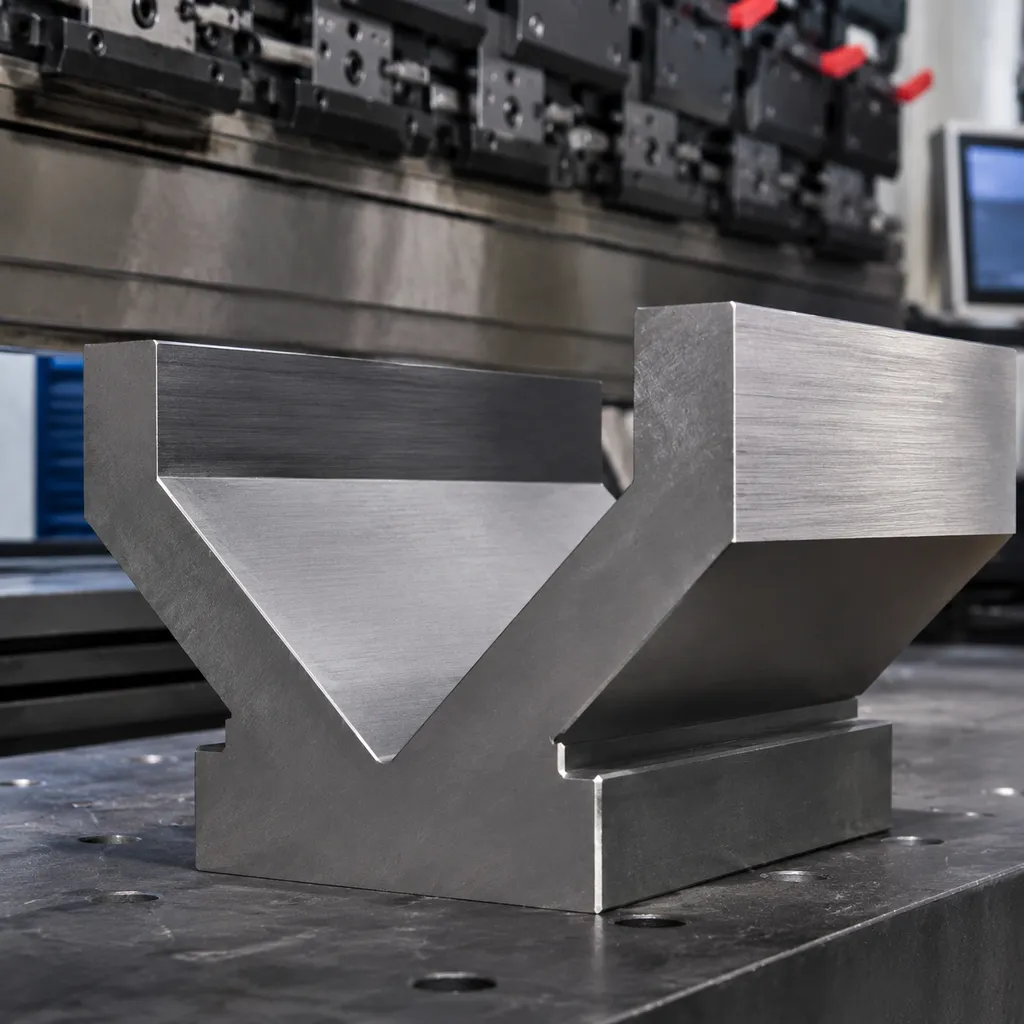
From full-length bars to american precision style tooling, our profile dimensions fit standard machine receiver slots without modification.
| Parameter | Specification |
|---|---|
| Profile Height / Working Height | 7.00" / 7.08" |
| V-Opening Options | 7/16", 7/8", 1-1/8", custom single-V, multi-V configurations |
| Material Options | Premium 42CrMo, 4140 steel, high-carbon alloy tool steel |
| Segmented Lengths | Standard 33.5", 16.3", 7" segmented sections, 7 ft full lengths |
Press Brake Machine Compatibility
Our 7-inch press brake dies align cleanly with major global clamping systems and machine configurations:
- American Precision Style: Works seamlessly with Cincinnati, Niagara, Chicago, Pacific, and Wysong press brakes. For classic T-groove machines, we also manufacture Cincinnati press brake die set compatible T-style dies.
- European / Promecam Style: Precision-engineered for rapid integration on Amada, Bystronic, LVD, and Trumpf machines.
- Wila / New Standard Style: Equipped with self-seating pin and button alignment for fast, accurate automatic tool clamping.
V-Opening Selection and Bending Guidelines
Choosing the right V-opening for your press brake die 7 inches profile directly affects bend accuracy, tonnage limits, and overall tool longevity. We rely on the standard 8× Rule for air bending tooling to establish the optimal V-width relative to sheet metal thickness:
V-Opening Formula: V = 8 × t (where V is the V-opening width and t is the sheet material thickness)
- 7/16" V-Opening: Best suited for 16-gauge sheet metal forming die setups where tight inside radii are needed.
- 7/8" V-Opening Die: Ideal for 11-gauge to 10-gauge mild steel, balancing formed part consistency and machine load.
When matching profile height requirements with our high-precision female press brake V-die for precise sheet metal bending, selecting the correct V-opening prevents edge deformation and minimizes strain on your press brake ram.
Tonnage and Bend Radius Reference
Air bending requires significantly lower tonnage compared to bottoming, while allowing greater flexibility across various material types. For acute angles or specialized profiles, utilizing a dedicated 30-degree press brake die for air bending reduces localized stress during forming.
| Bending Method | Tonnage Requirement | Recommended Tip Radius | Ideal Material Application |
|---|---|---|---|
| Air Bending | Baseline (1× required load/ft) | Equal to material thickness (t) | Eliminates cracking in high-strength aluminum and stainless alloys |
| Bottoming | 3× to 5× Air Bending load/ft | Slightly less than inside radius | Ensures strict dimensional consistency in standard carbon steels |
Primary Industry Applications
We engineer our 7 inch press brake tooling to deliver repeatable performance across demanding sheet metal fabrication sectors:
- Heavy-Duty Structural Enclosures: Industrial control housings, electrical cabinets, and operator consoles.
- Architectural Metal & Elevator Paneling: Decorative stainless cladding, entrance frames, and custom trim.
- HVAC & Commercial Chassis: Large ducting transitions, commercial truck frame components, and trailer sub-assemblies.
- Agricultural & Automotive Stamping: Heavy machinery guards, mounting brackets, and structural stamping prototypes.
CAMT Quality Assurance & Manufacturing Process
We build every press brake die 7 inches tooling profile using an uncompromised, quality-controlled workflow. This guarantees exact profile repeatability, structural longevity, and tight bend tolerances across every batch.
6-Stage Precision Production Workflow
- Certified Alloy Inspection: We thoroughly audit raw material heat numbers and chemical compositions based on our press brake die material guide to guarantee high-tensile core integrity.
- Rough CNC Machining: High-speed milling removes excess stock and shapes basic V-die geometries before heat treating.
- Vacuum Heat Treatment & Deep Induction Hardening: Advanced thermal processing creates a deep HRC 55–60 wear surface on critical contact edges, preserving a resilient HRC 47–50 core shock resistance.
- Multi-Axis CNC Profile Grinding: Precision profile grinders bring working surfaces down to Ra < 0.8 µm roughness and critical profile tolerances to within ±0.01 mm.
- Full QA Optical CMM Inspection: Automated optical measuring systems check full profile dimensions, working heights, and V-angles against engineering drawings.
- Protective Export Packaging: Anti-rust coating and custom reinforced packaging ensure your 7 inch press brake tooling arrives defect-free.
Our focus remains on delivering reliable accuracy and extended wear life—see why CAMT is trusted worldwide for high-tonnage sheet metal forming tooling.
Custom Press Brake Die 7 Inches: Tailored OEM & ODM Solutions
Standard off-the-shelf tooling doesn't always fit specialized forming jobs. When off-the-shelf profiles fall short, we build engineered custom press brake tooling designed specifically for your press brake die 7 inches requirements and complex production setups.
Specialized Tooling Capabilities
We manufacture customized 7 inch press brake tooling configurations engineered to solve demanding geometry and clearance challenges:
- Custom Acute Angles: Dedicated 30°, 45°, and 60° acute angle bending die profiles built to handle severe springback and overbending needs.
- Deep Gooseneck Offsets: Custom gooseneck punch 7 inch height profiles engineered to clear deep returns, U-channels, and box flanges without tooling collision.
- Adjustable V-Widths: Modular bottom V die blocks designed to accommodate multiple sheet metal thicknesses on a single press set.
- Non-Marking Urethane Holders: Specialized non-marking press brake die insert holders to eliminate tooling marks on architectural aluminum, brass, and polished stainless steel.
Streamlined Engineering Collaboration Workflow
Through our end-to-end custom tooling development workflow, we move your concept from CAD model to full production without delay:
- CAD File Submission: Send us your CAD geometries in 2D (DXF/DWG) or 3D (STEP/IGES) formats along with material yield strengths and thickness tolerances.
- CAMT Simulation & Analysis: We perform computer-assisted tonnage calculations and 3D collision simulations to verify tool clearance and load limits.
- Design Approval: You review and approve complete manufacturing drawings featuring precise tip radii, V-openings, and profile dimensions.
- Precision Production: We execute CNC machining, vacuum heat treatment, and multi-axis profile grinding to deliver production-ready tooling.
Frequently Asked Questions
What sheet metal gauges work best with a 7/8-inch V-opening die?
A 7/8-inch V-opening is ideal for forming 11-gauge to 10-gauge mild steel (approximately 0.120" to 0.135" or 3 mm thickness) under standard air bending conditions. Following the 8× rule (V = 8 × t), this opening delivers smooth bends, balanced tonnage demands, and optimal inside bend radii without stressing your press brake system.
How does localized induction hardening stop die wear on stainless steel?
Forming stainless steel rapidly degrades unhardened tooling due to high tensile resistance and galling. We engineer our press brake die 7 inches profiles with targeted deep induction hardening, achieving HRC 55–60 surface hardness at critical contact points while preserving a tough HRC 47–50 core. This localized treatment prevents galling and resists premature wear during continuous high-tonnage production runs. Explore our full line of high-strength press brake die sets engineered for abrasive forming applications.
Can CAMT 7-inch dies adapt to older American-style manual clamping systems?
Yes. We manufacture these 7-inch profile dies with standard precision tangs and modular retrofitting adapters. Whether running vintage manual mechanical brakes or updated hydraulic setups, our tooling retrofits easily without requiring modifications to your existing clamping rails. Review our complete line of American and European tooling options for cross-platform machine compatibility.
How do I eliminate die marks on painted or aesthetic sheet metal?
To prevent visible contact lines and scratch marks on pre-painted, aluminum, or mirror-finish stainless panels, apply these quick shop practices:
- Use protective urethane tape: Place heavy-duty polyurethane protective tape directly over the die shoulders to cushion contact points.
- Rely on high-precision ground profiles: Utilize our fine-ground V-die contact surfaces rated at Ra < 0.8 µm to reduce friction during sheet drawdown.
- Implement non-marking die inserts: Retrofit your setup with composite urethane holders for sensitive architectural or decorative fabrications.



