Formula details
Product Details
Overview
Engineering Advantages: Why Upgrade to CAMT Air Bending Tooling?
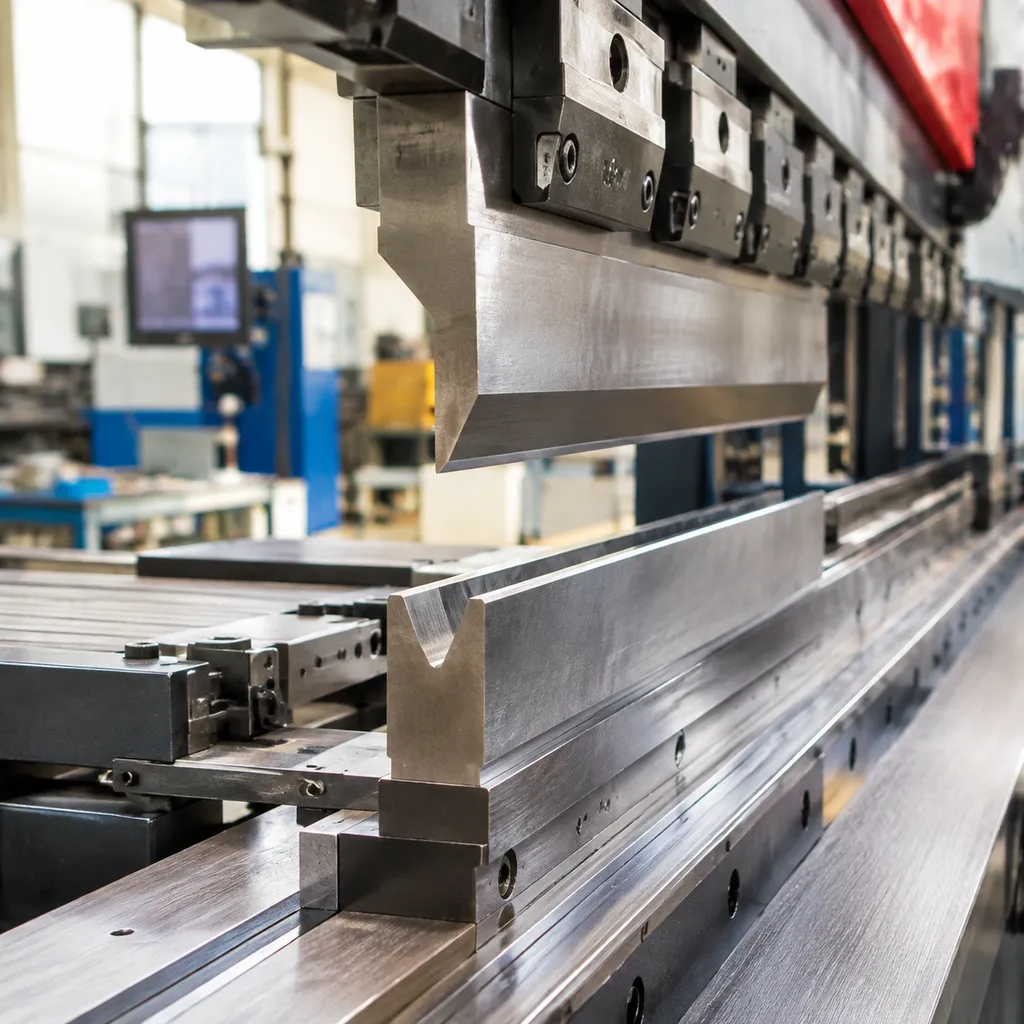
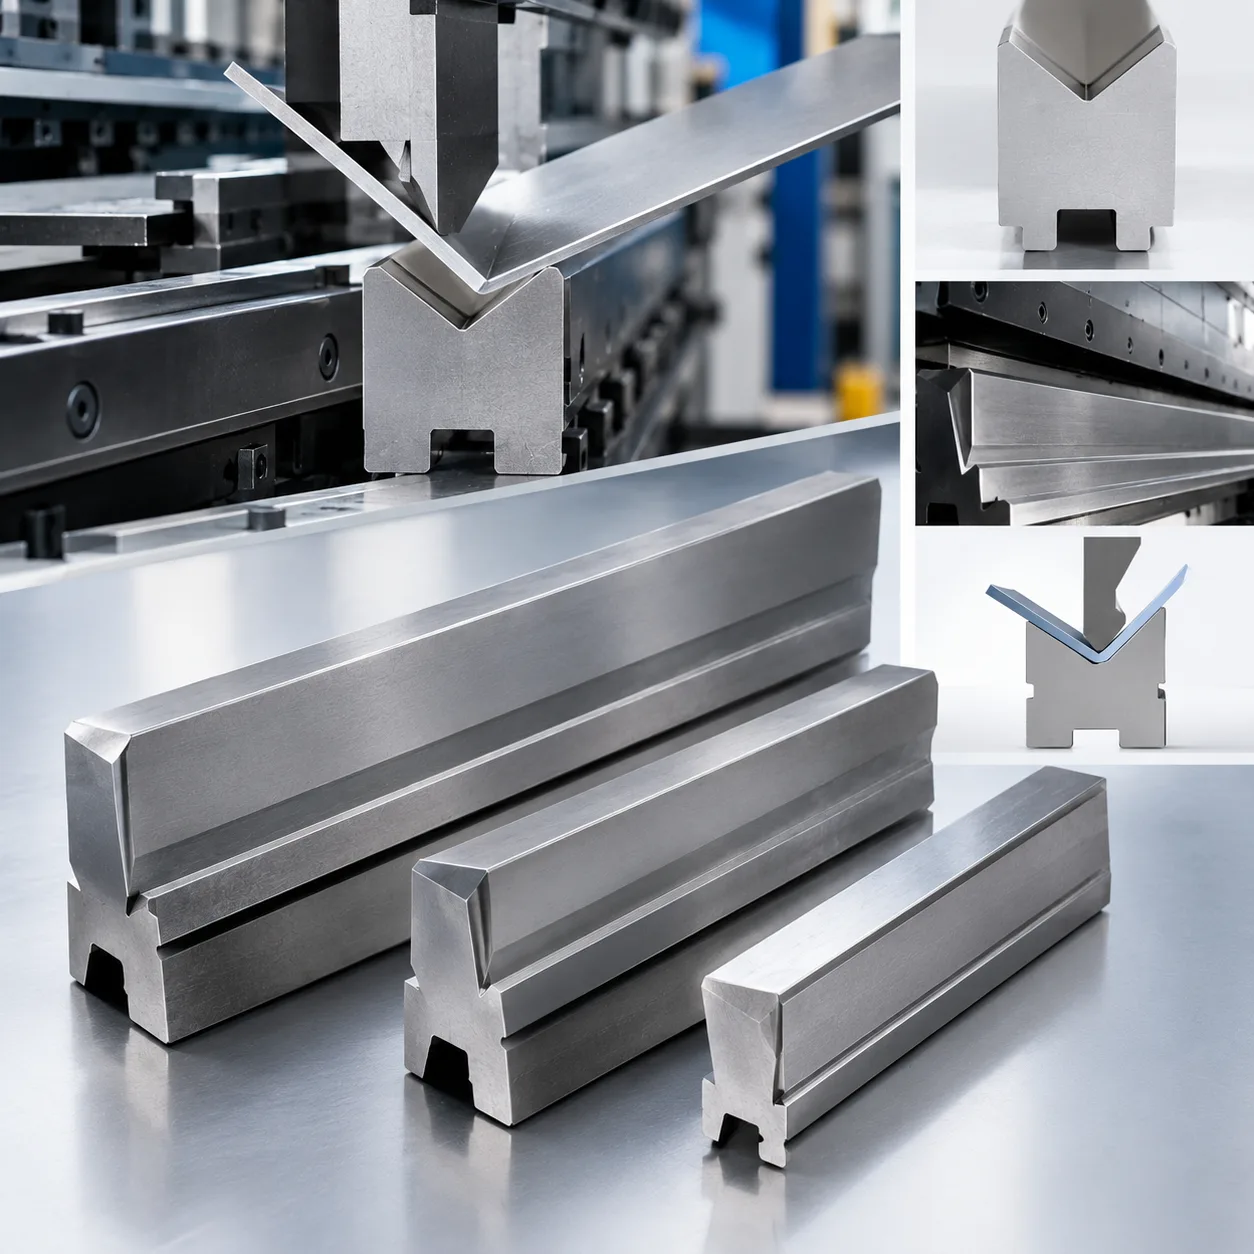
Standard shop press setups often rely on bottoming dies that force your 20-ton hydraulic ram to work at its absolute limit, resulting in severe plate marring, inconsistent springback, and excessive frame flex.We engineered this SWAG-Compatible Air Bending Bottom Die as an alternative tooling solution designed to match compatible SWAG air bending dies, delivering reliable bending performance for industrial press brake applications.By shifting the workload to precision three-point contact geometry, you gain complete angle versatility while protecting both your workpiece and your hydraulic press.
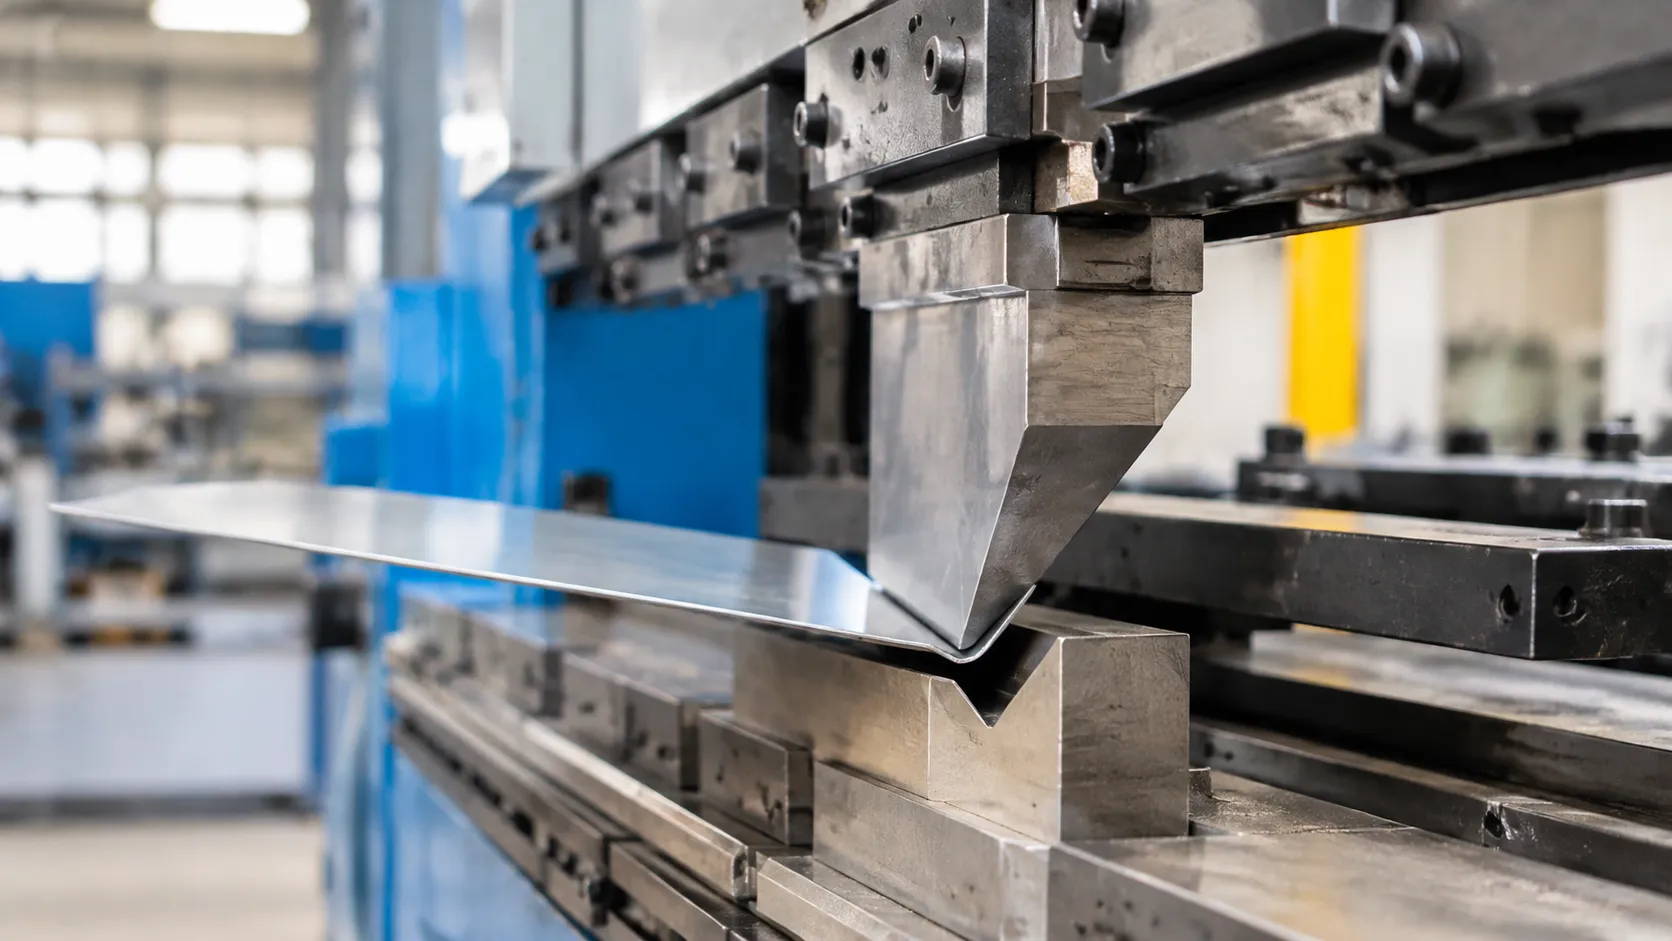
- True Air Bending Geometry: The plate contacts only the two precision-ground die shoulders and the top punch tip. Because you never bottom out or coin the material against the root of the die, required forming tonnage drops significantly, keeping your shop press operating well inside its safe working envelope.
- Variable Bend Angles from 170° Down to 85°: A single swag air bending bottom die covers your entire bending spectrum. By simply adjusting your stroke depth, you can form open obtuse profiles down to a clean 90° bend or an acute 85° fold to cancel out high springback in high-tensile sheet metal.
- Precision Shoulder Radii: Factory punch-and-die sets often drag rough cut edges across the plate, gouging raw stock. Our bottom dies feature precision-machined, polished shoulder radii that eliminate die marking, scoring, and surface galling on sensitive 5052 aluminum and 304 stainless steel.
- Pre-Hardened 4140 Alloy Construction: Fabricated from high-grade 4140 chromoly alloy steel, the contact edges are heat-treated to resist grooving, edge deformation, and wear under continuous 20-ton press brake loads.
- Drop-In Footprint: The lower tang and base profile are machined specifically to slip straight into standard SWAG lower retaining channels. There is zero machining, drilling, or shimming required—drop the tooling into place, run your alignment pass, and start bending.
Technical Specifications & Model Sizing Matrix
Standard shop press attachments struggle with tool deflection and inconsistent bottoming grooves. We solve this by milling our dies from solid billet with deep relief geometry, giving your hydraulic shop press true air-forming precision.
For exact tooling footprints and profiles across our lineup, check our comprehensive press brake die size chart and dimensions guide.
Core Tooling Dimensions
- Available Working Lengths: 19.25 in (standard SWAG kit fitment), 25.0 in, and 39.5 in for wide-bed conversion frames.
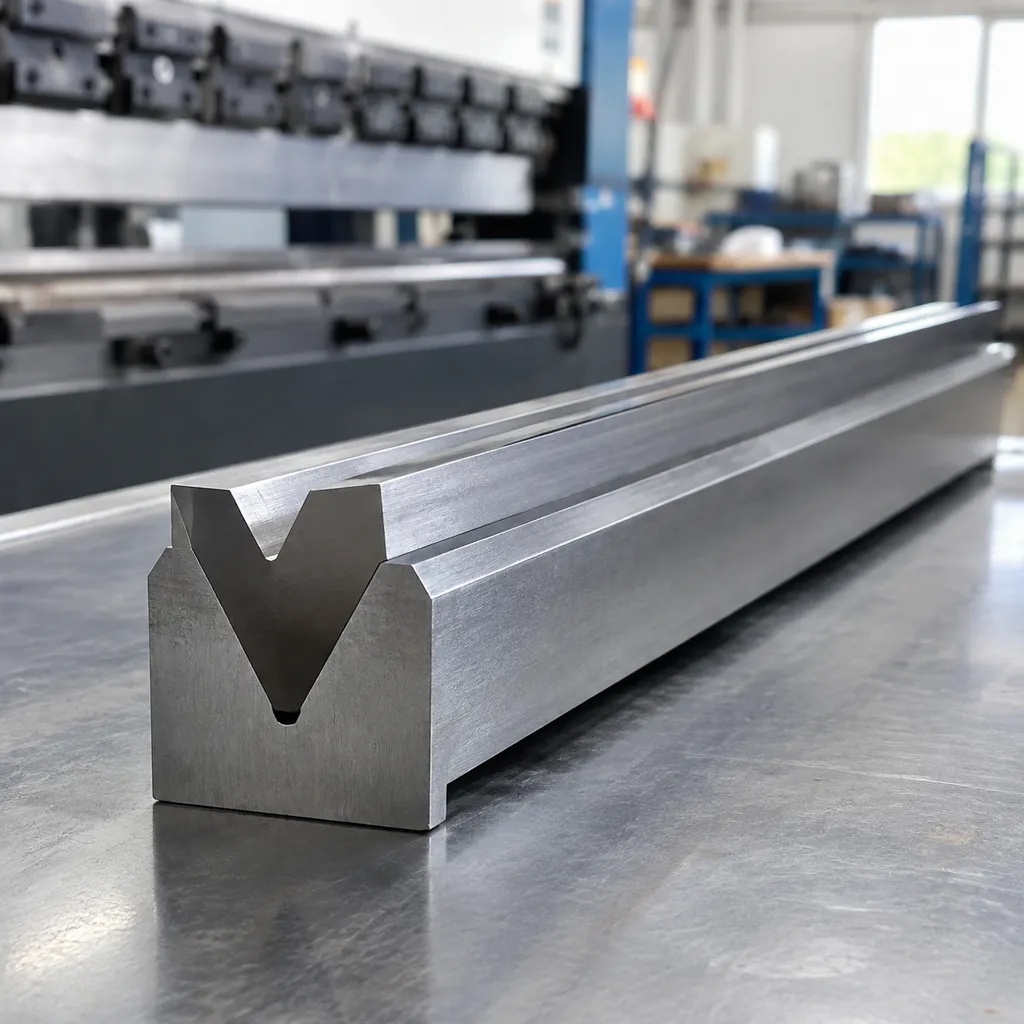
- Die Included Angle: 85° acute profile (delivers full springback clearance down to 90° and beyond).
- Base Profile: 0.500 in tang width with precision parallel base flats to sit flush inside OEM bottom channels.
- Material & Hardness: Pre-hardened 4140 alloy steel, precision CNC ground contact shoulders (HRC 28–32 core, induction-hardened wear shoulders).
| Die Model / Base Code | Working Length | V-Opening Width | Die Angle | Shoulder Radius | Base Tang Width |
|---|---|---|---|---|---|
| CAMT-SAB-085-050 | 19.25 in / 25 in | 0.500 in (1/2") | 85° | 0.062 in (1/16") | 0.500 in |
| CAMT-SAB-085-075 | 19.25 in / 25 in | 0.750 in (3/4") | 85° | 0.093 in (3/32") | 0.500 in |
| CAMT-SAB-085-125 | 19.25 in / 25 in | 1.250 in (1-1/4") | 85° | 0.125 in (1/8") | 0.500 in |
| CAMT-SAB-085-200 | 19.25 in / 25 in | 2.000 in (2") | 85° | 0.187 in (3/16") | 0.500 in |
V-Opening Selection Guide
Matching your swag air bending bottom die opening width to your material stock thickness keeps tonnage within safe limits and eliminates cracking along the outer bend radius. We follow the proven 8x rule for mild steel, expanding to 10x–12x for harder alloys or heavier plate.
- Sheet gauge (18 Ga to 14 Ga): Run a 0.500 in V-opening for tight inside radii on thin sheet metal.
- Medium plate (1/8 in / 11 Ga to 10 Ga): Step up to a 0.750 in to 1.000 in V-opening to balance tonnage and edge control.
- Heavy plate (3/16 in to 1/4 in): Shift to a 1.250 in to 2.000 in V-opening to keep your hydraulic bottle jack below pressure relief limits.
Before setting up your bend sequences, consult our practical press brake V-die opening guide to dial in punch tip clearances and minimum flange lengths.
Safe Tonnage Capacity Limits (Tons per Foot)
Air bending does not require bottoming or coining pressure. You can form accurate angles with significantly less force. The ratings below reflect maximum safe loading per linear foot across mild steel, 5052-H32 aluminum, and 304 stainless steel.
| Material Thickness | Recommended V-Opening | Mild Steel (A36 / 60k PSI) | 5052-H32 Aluminum (31k PSI) | 304 Stainless (85k PSI) |
|---|---|---|---|---|
| 16 Gauge (0.060") | 0.500 in | 1.2 Tons / ft | 0.7 Tons / ft | 1.7 Tons / ft |
| 14 Gauge (0.075") | 0.625 in | 2.1 Tons / ft | 1.2 Tons / ft | 2.9 Tons / ft |
| 11 Gauge (0.120") | 1.000 in | 3.8 Tons / ft | 2.1 Tons / ft | 5.3 Tons / ft |
| 3/16 in (0.188") | 1.500 in | 6.2 Tons / ft | 3.5 Tons / ft | 8.7 Tons / ft |
| 1/4 in (0.250") | 2.000 in | 8.5 Tons / ft | 4.8 Tons / ft | 11.9 Tons / ft |
Never exceed the 20-ton structural limit of your shop press frame when working across full-width plate.
SWAG Press Brake Model Compatibility
We engineered this Compatible Air Bending Bottom Die for SWAG Press Brakes to eliminate the guesswork of retrofitting shop press tooling. If you run a hydraulic shop press brake attachment from SWAG Off Road, this lower die drops directly into the lower receiver channel without requiring machining, milling, or welding.
Direct Fit Kit Matrix
Our swag air bending bottom die matches the exact cradle width and throat clearance specifications across popular DIY and pre-welded SWAG-style setups:
| SWAG Model Platform | Lower Receiver Fitment | Recommended Tooling Length | Application Target |
|---|---|---|---|
| SWAG 20-Ton Standard | Direct drop-in into lower channel | 19.25" | General sheet metal fabrication & light plate |
| SWAG 20-Ton Heavy Duty (HD) | Full seating inside HD lower cradle | 19.25" | Structural brackets, heavy tabs & high-tonnage plate |
| SWAG 20-Ton Finger Brake | Flush alignment with finger beds | 19.25" / segmented sections | Box and pan forming, deep enclosures & chassis components |
Whether you run an original welded kit or a heavy-duty bolt-together build, the base profile locks squarely between the lower upright guides. There is no play or lateral twisting when the ram begins building pressure.
Top Punch Interoperability
Because our tooling relies on true air bending geometry, the lower die profile is not tied to a single punch shape. The angle of your bend is governed purely by ram depth rather than punch-to-die matching. We built this finger brake bottom die replacement to interface seamlessly with:
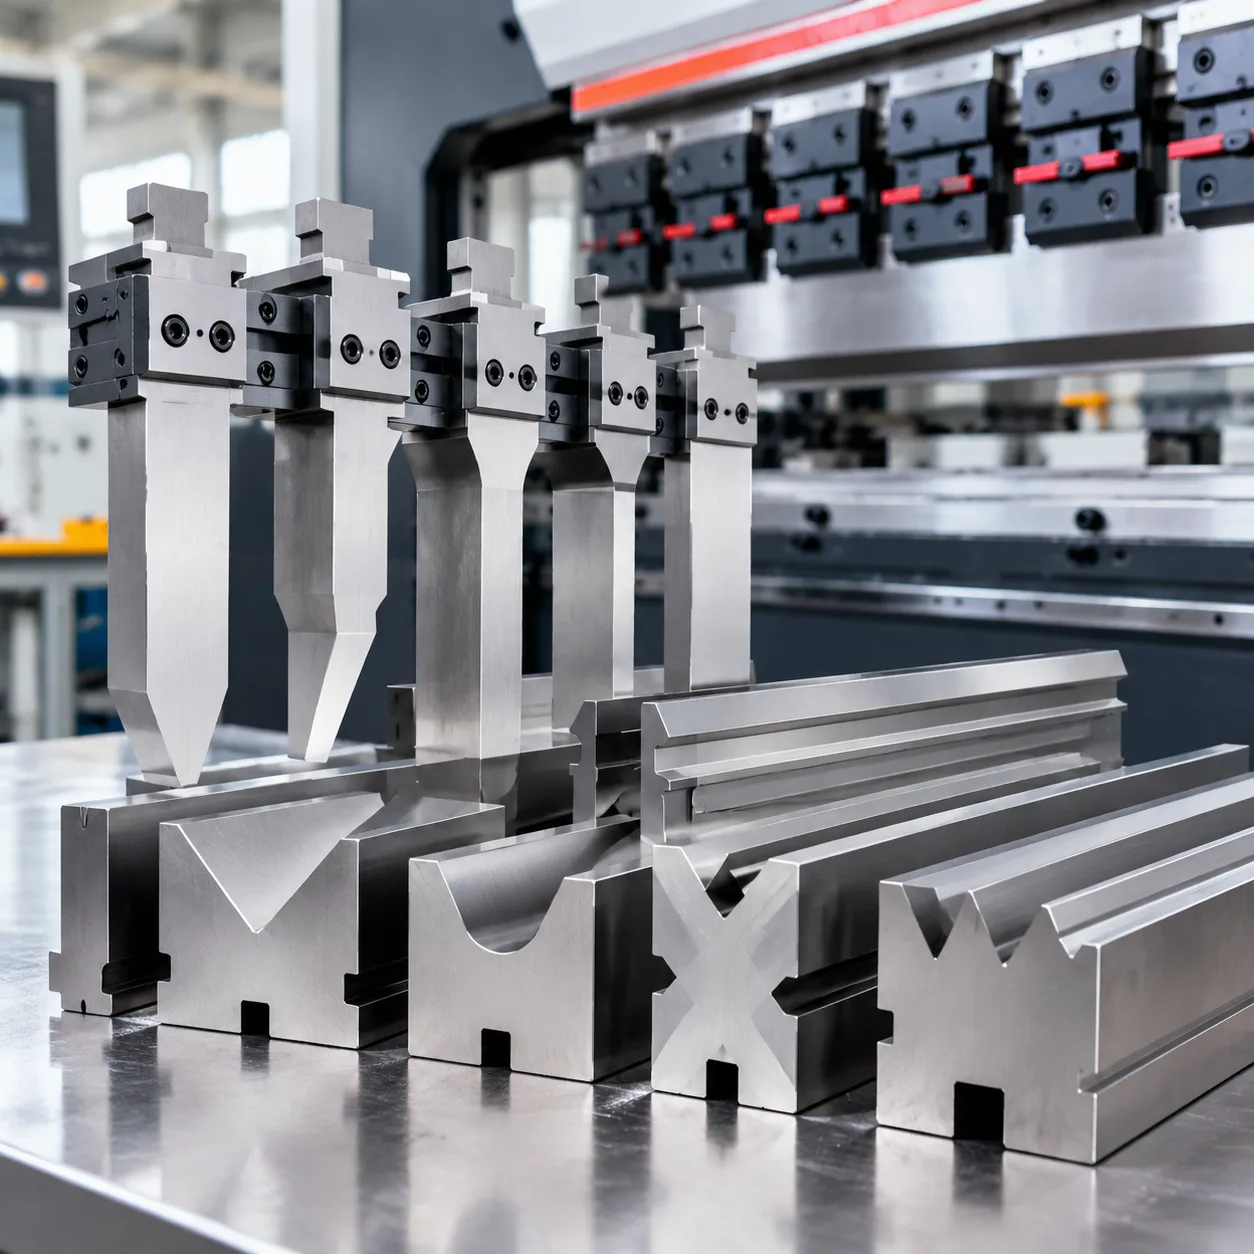
- OEM Straight & Knife-Edge Punches: Run your standard factory top bar for basic structural brackets, angle iron fabrication, and 90° bends down to an 85° acute profile.
- Radius Bars & Punches: When forming 5052-H32 aluminum, 4130 chromoly, or hard structural steel where small punch tips cause cracking along the bend line, drop our die beneath heavy-duty radius punches to maintain a uniform outer bend without galling.
- Segmented & Acute Finger Tooling: Box-and-pan jobs demand clearance for returned flanges. Our die accommodates narrow acute punches without shoulder interference, letting you work tight four-sided enclosures cleanly on a shop press footprint.
By running this lower die in your swag off road press brake tooling setup, you convert a rigid, single-angle bottle jack press into a versatile forming station that handles varied punch profiles and variable angle requirements without re-rigging your machine.
Air Bending vs. Standard Bottoming Dies: Real Shop Performance Differences
When we switched our setups to a dedicated swag air bending bottom die, the physical load on our 20-ton hydraulic jacks dropped immediately. Bottoming requires forcing the punch completely into the die root to coin the material, whereas true sheet metal air bending tooling supports the workpiece at three distinct contact points.
Using an air bending profile lets you bypass brute force entirely. For fabricators working with high-tensile alloys or tight bend profiles, utilizing specialized acute press brake dies for precision metal bending provides the exact clearance needed to reach deep bend angles without jamming the tooling.
| Operational Factor | Standard Bottoming Die | Compatible Air Bending Bottom Die for SWAG Press Brakes |
|---|---|---|
| Tonnage Demand | Full yield + high coining pressure | Up to 70% lower hydraulic force |
| Springback Control | Fixed angle only; cannot overbend | Variable stroke depth compensates instantly |
| Ram & Frame Deflection | Severe flex near maximum jack limits | Minimal stress; keeps frame parallel |
| Material Flexibility | One tool per thickness/angle | Multiple gauges and angles in one V-opening |
Tonnage Reduction: Cut Jack Pressure by Up to 70%
Bottoming out 3/16" or 1/4" plate demands massive hydraulic force because the tool must crush the metal into the bottom of the V-groove. A proper press brake v die designed for air bending needs only enough force to yield the material at the apex. By eliminating bottom contact, we cut required operating pressure by up to 70%, keeping a 20-ton press brake die well within its safe working limits.
Springback Control Without Tooling Swaps
Every metal batch fights back differently:
Mild Steel: 0.5° to 1.5° springback
5052 Aluminum: 1.5° to 3° springback
304 Stainless: 3° to 5° springback
Standard bottoming dies leave zero room for adjustment—if your die is cut to 90°, springback gives you a sloppy 93° part. With our hydraulic shop press brake die, the deep relief allows you to slightly overstroke to 88° or 86°, letting the material settle into a dead-on 90° bend every single stroke.
Machine Longevity: Save Your Shop Press Frame
Pushing a 20-ton bottle jack to its absolute stall point bends your side uprights, tweaks the ram beam, and wears out guide bushings. Air bending keeps operational loads low, eliminating machine flex and ensuring every bend stays uniform across the entire length of the bed.
Setup, Centering, and Alignment for SWAG Air Bending Bottom Dies
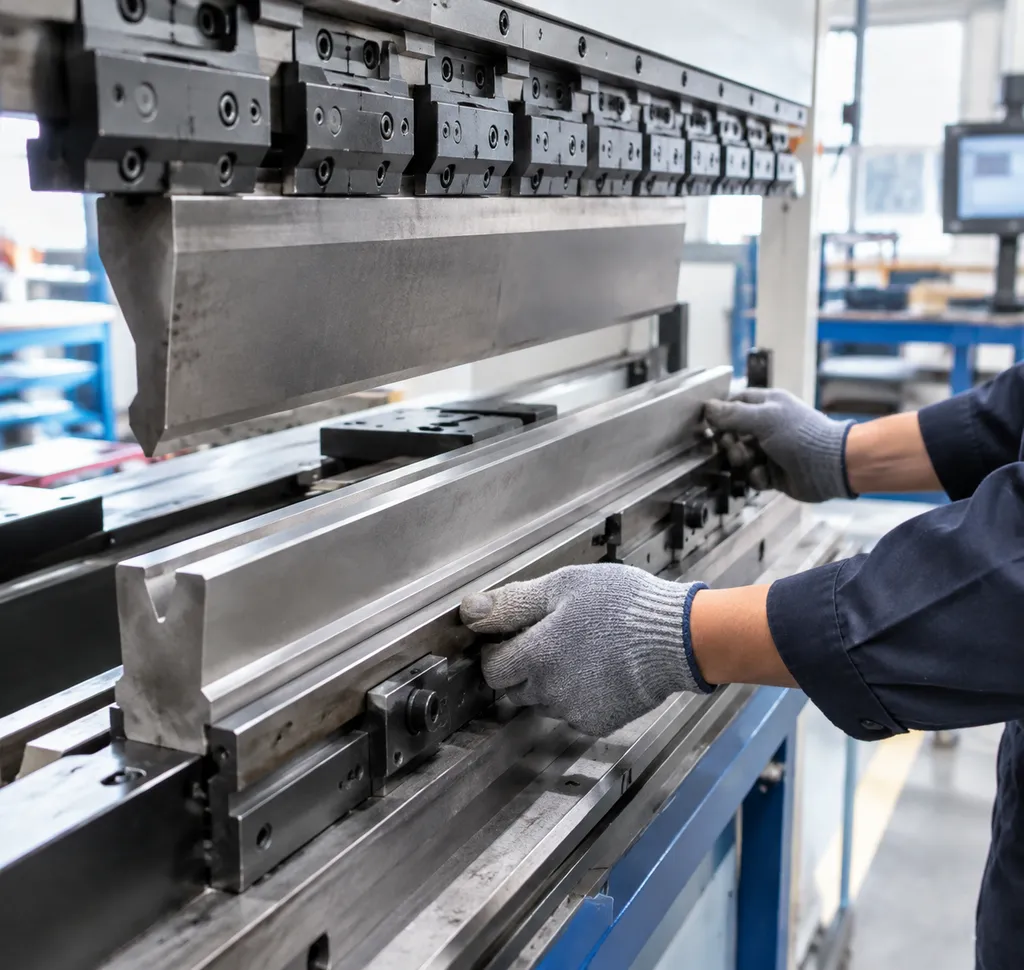
Because air bending forms sheet metal by controlling stroke depth rather than bottoming out, the alignment between your upper punch and the lower V-die must be dead true before you pump the cylinder.
Step-by-Step Seating: Locking into the Receiver Channel
We design our compatible air bending bottom die for SWAG press brakes to drop directly into the lower frame channel without machining modifications.
- Clean the bed: Scrape away slag, mill scale, and debris from the SWAG lower frame receiver. Any grit trapped beneath the die base will telegraph through the workpiece as an angle variance across the length of the bend.
- Seat the die: Place the hydraulic shop press brake die flat into the lower retaining channel. Verify that the bottom ground surface sits flush against the bottom plate.
- Snug the side fasteners: Lightly tighten the side alignment bolts or set screws on the SWAG frame. Leave just enough float so the die can self-center during the alignment stroke.
Precision Centering Procedure Under Low Hydraulic Pressure
Never eyeball punch-to-die alignment. An off-center punch exerts side-load forces on your press uprights, produces inconsistent bend radii, and can chip hardened tooling edges under heavy tonnage.
- Lower the punch manually: Bring the top punch down slowly into the center of the V-groove using feather-light hydraulic pressure on your bottle jack or hand pump.
- Nest punch tip in the V-opening: Allow the tip of the upper blade to locate the bottom apex of the die groove. Knowing how to select the right press brake punch radius is critical here to ensure the punch nose mates smoothly with the die shoulders without binding or galling.
- Lock the bottom tooling: With the punch fully nested under low hydraulic pressure, tighten all retaining bolts along the SWAG receiver channel evenly.
- Zero-load clearance check: Retract the cylinder fully, then cycle the ram down a second time without material. Verify that the punch enters and leaves the die groove with equal clearance on both shoulders.
Stroke Depth Repeatability: Stop Collars and Dial Indicators
In air bending, the bend angle is dictated entirely by how deep the punch enters the V-opening. Because you are not coining or bottoming out against the die flats, mechanical depth control is essential.
- Threaded Stop Collars: Run heavy-duty split clamping collars on the guide rods of your shop press. Once you hit your target angle, lock the collar hard against the guide bushings to halt ram travel at the exact same depth on every stroke.
- Magnetic Dial Indicators: Mount a 1-inch travel dial indicator on the press frame with the contact point resting directly on the moving upper punch bar. Reading ram travel down to 0.001" (0.025 mm) lets you compensate precisely for batch-to-batch material springback without scrap pieces.
- Log Bend Depths: Keep a physical log next to your press brake detailing plate thickness, material grade (such as 1018 steel or 5052-H32 aluminum), and the dial indicator stroke reading required to hit 90° or 45°.
Frequently Asked Questions: SWAG Air Bending Bottom Die
Can I bend a clean 90° angle if the bottom die is cut at 85°?
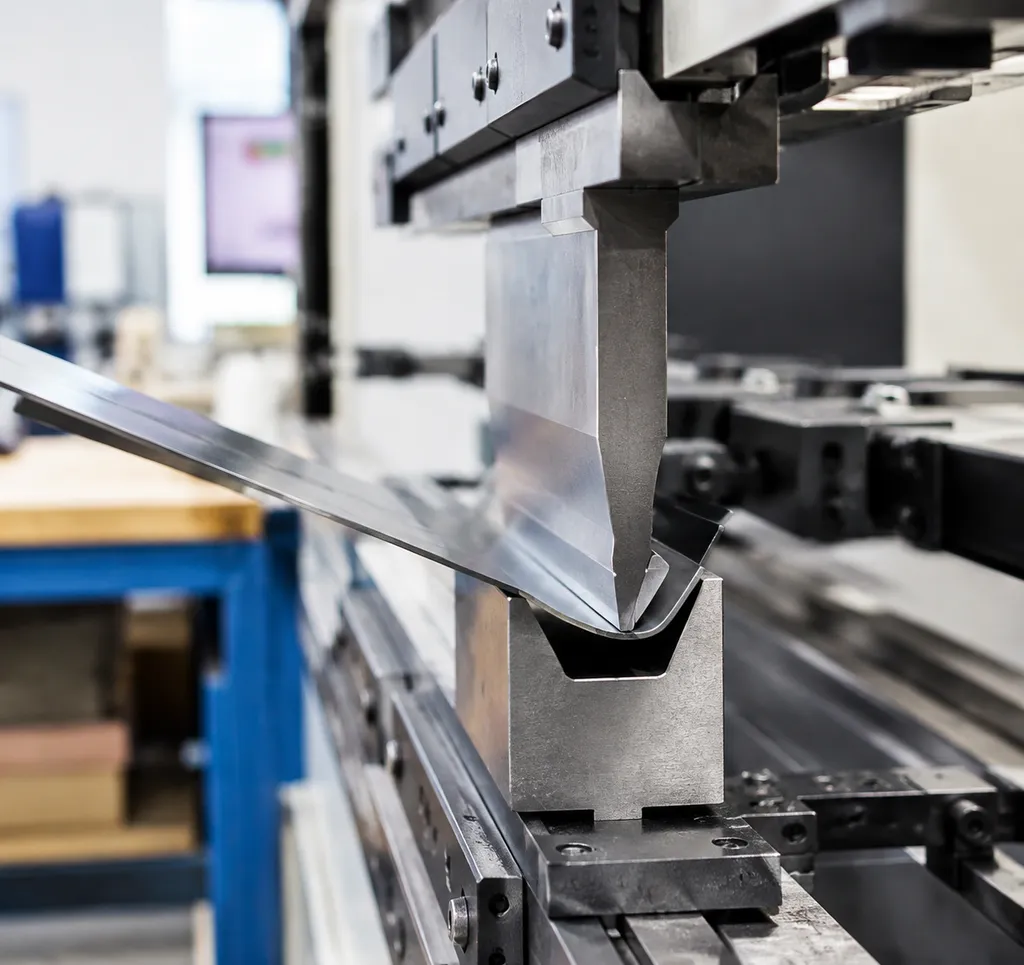
Yes. That is the core advantage of an acute angle bottom die. In an air bending setup, you never bottom out or coin the plate. We drive the top punch down until the workpiece over-bends slightly past 90° (typically between 87° and 89°), allowing the sheet to spring back to a dead-true 90° bend once hydraulic pressure releases.
What is the thickest plate recommended for a 20-ton SWAG setup?
On a standard 20-ton hydraulic shop press brake die setup, the realistic capacity is 1/4-inch (6.35 mm) mild steel across short spans using a 2-inch or wider opening. Attempting to bend 1/4-inch across a narrow V-groove will overload your 20-ton bottle jack and risk structural frame deflection. Review our press brake die selection guide for precise bending to verify required tonnage per foot against your target plate thickness and material yield strength.
Does this lower die require machining or welding to fit my press brake?
No machining, shimming, or welding is needed. We engineer each compatible air bending bottom die for SWAG press brakes as a direct drop-in replacement. The base profile seats firmly inside standard OEM lower retaining channels and centers quickly between the side guide plates.
Should I choose an 85-degree or an 88-degree die profile?
Your choice comes down to the springback characteristics of your typical stock:
| Material Type | Typical Springback | Recommended Profile | Purpose |
|---|---|---|---|
| Mild Steel (A36, 1018) | 1° – 2° | 88° or 85° | General fab work and consistent square corners |
| 5052 / 6061 Aluminum | 2° – 4° | 85° | Overcomes elastic memory without bottoming out |
| 304 / 316 Stainless & AR Plate | 3° – 6° | 85° | Provides needed relief to strike crisp 90° returns |
For multi-material fabrication shops, our 85° profile offers the greatest operational versatility without locking you into a single alloy.
Can I run this air bending bottom die with segmented finger punches?
Yes. Our swag air bending bottom die works with standard straight punches, radius bars, and segmented finger setups. Simply verify that your finger punch tip angle is 85° or sharper (such as a 75° or 60° acute punch) to prevent premature contact with the die shoulder walls before reaching your desired bend depth.
Ordering, Shipping, and Tooling Guarantee
Standard Lengths, Custom Cuts, and Packaging
We stock every Compatible Air Bending Bottom Die for SWAG Press Brakes in standard lengths matched precisely to 19-inch, 25-inch, and 40-inch shop press frames. If your setup requires unique segmentation or non-standard widths for tight box work, we also supply custom press brake tooling machined to your exact project specs.
- Stock Sizes: Direct drop-in lengths for standard SWAG lower receiver channels.
- Custom Sizing: Precision cut-to-length service with de-burred, clean-squared edges ready for ganging.
- Corrosion Protection: Dipped in heavy rust-preventative oil and sealed in vapor-corrosion inhibitor (VCI) wrap.
- Transit Casing: Packed in heavy-wall rigid tubing with end-cap shock protection to prevent shoulder dings during transit.
CAMT Hardness and Dimensional Accuracy Guarantee
Every swag air bending bottom die leaves our floor true, flat, and inspected. We machine our dies from certified 4140 alloy steel, maintaining strict dimensional tolerances so your bends stay repeatable from one end of the press bed to the other.
- Shoulder Uniformity: Parallel shoulder radii held within +/-0.001" along the entire working length to prevent uneven drag and sheet twisting.
- Surface Hardness: Precision induction-hardened contact zones hit 48–52 HRC to eliminate galling when forming high-yield plate.
- Camber and Bow Verification: 100% straightness-checked under dial indicators to ensure a completely flat seat in your hydraulic shop press brake die receiver.