Formula details
Product Details
Overview
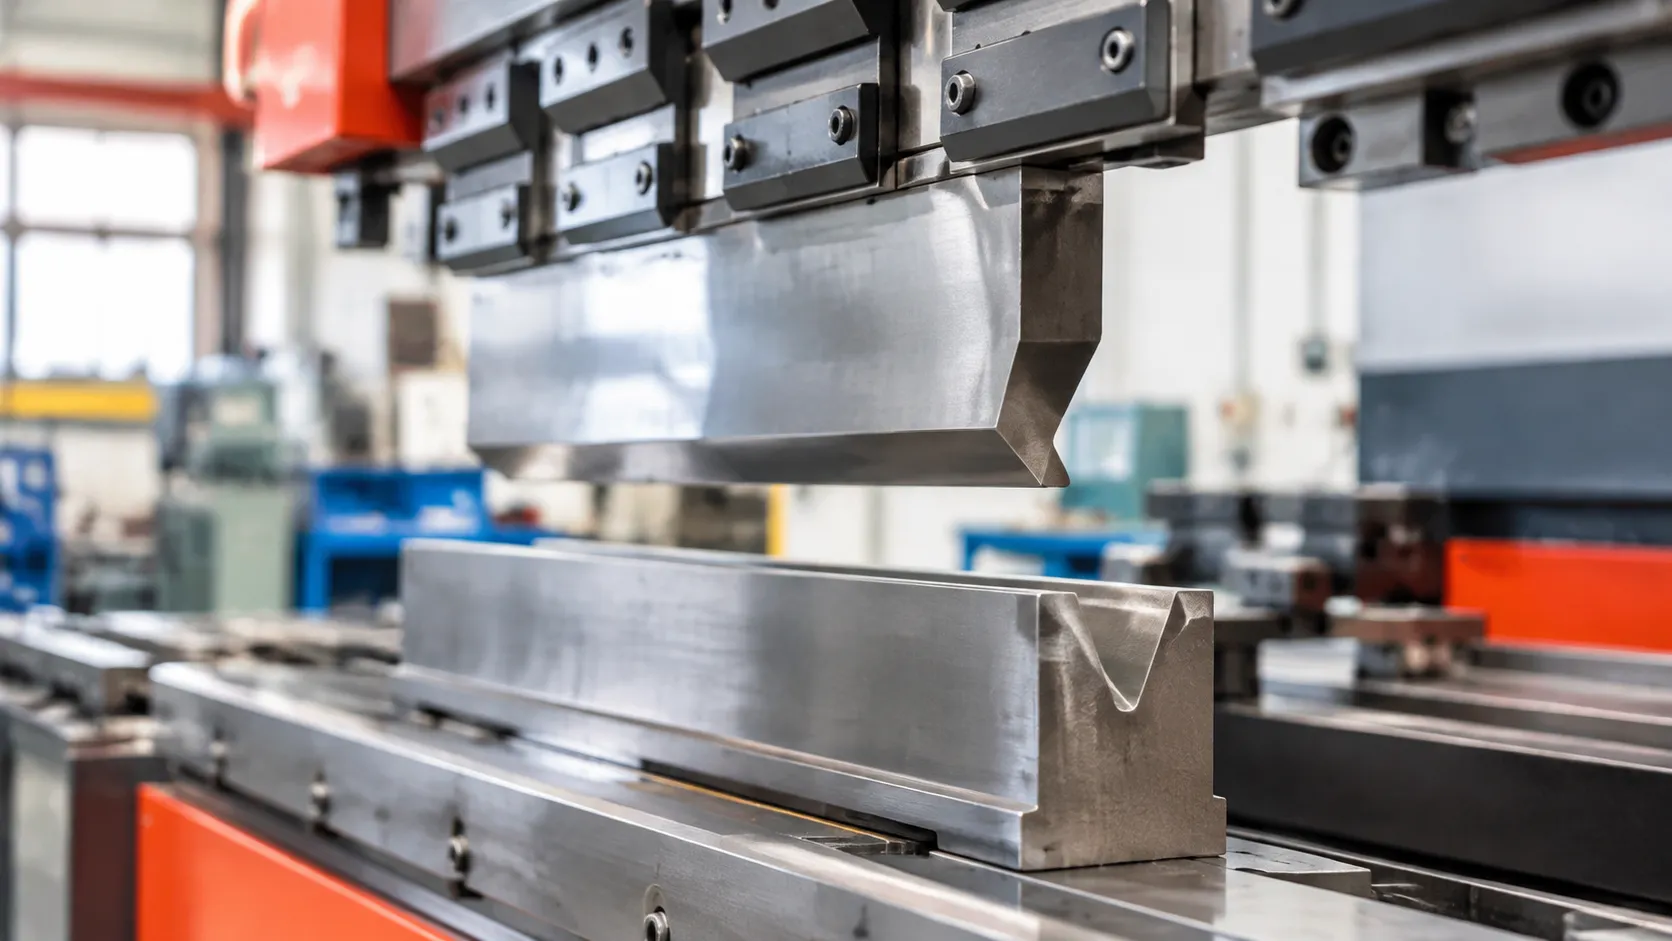
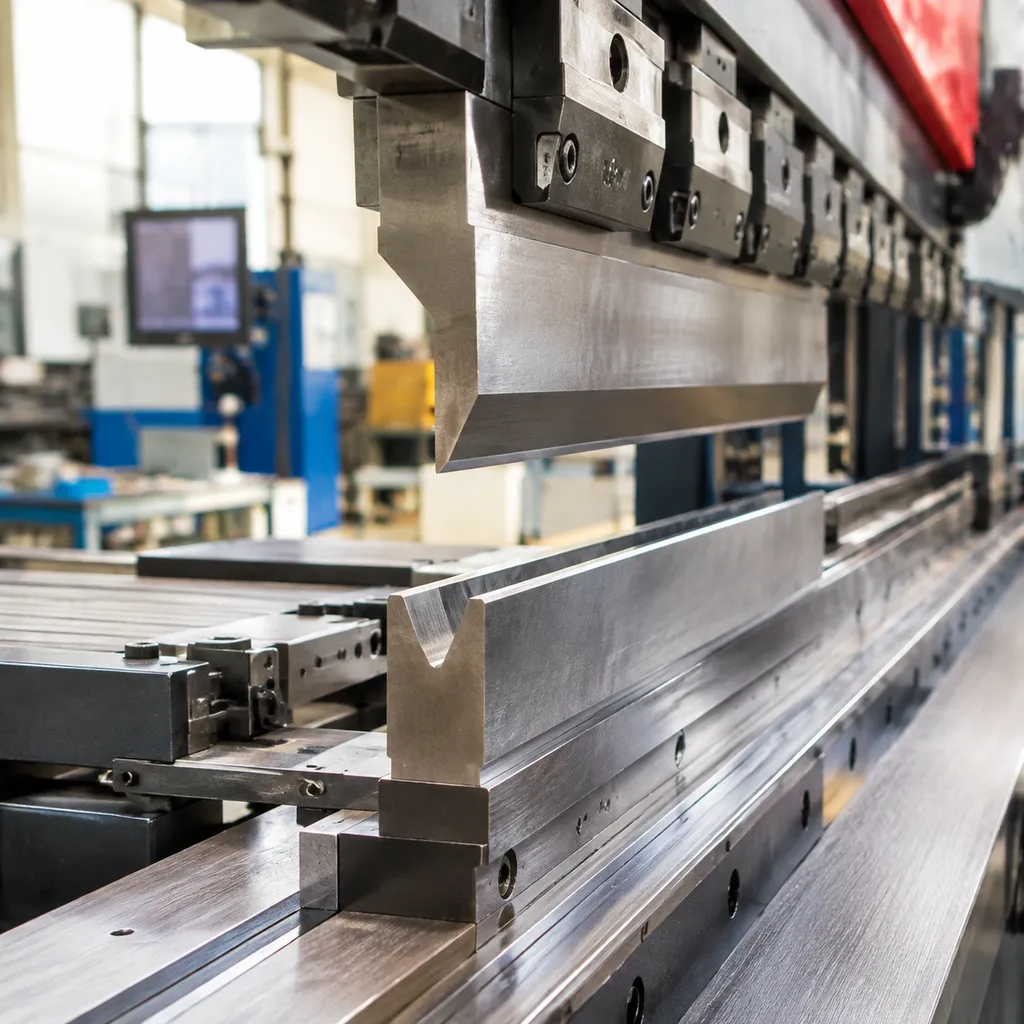
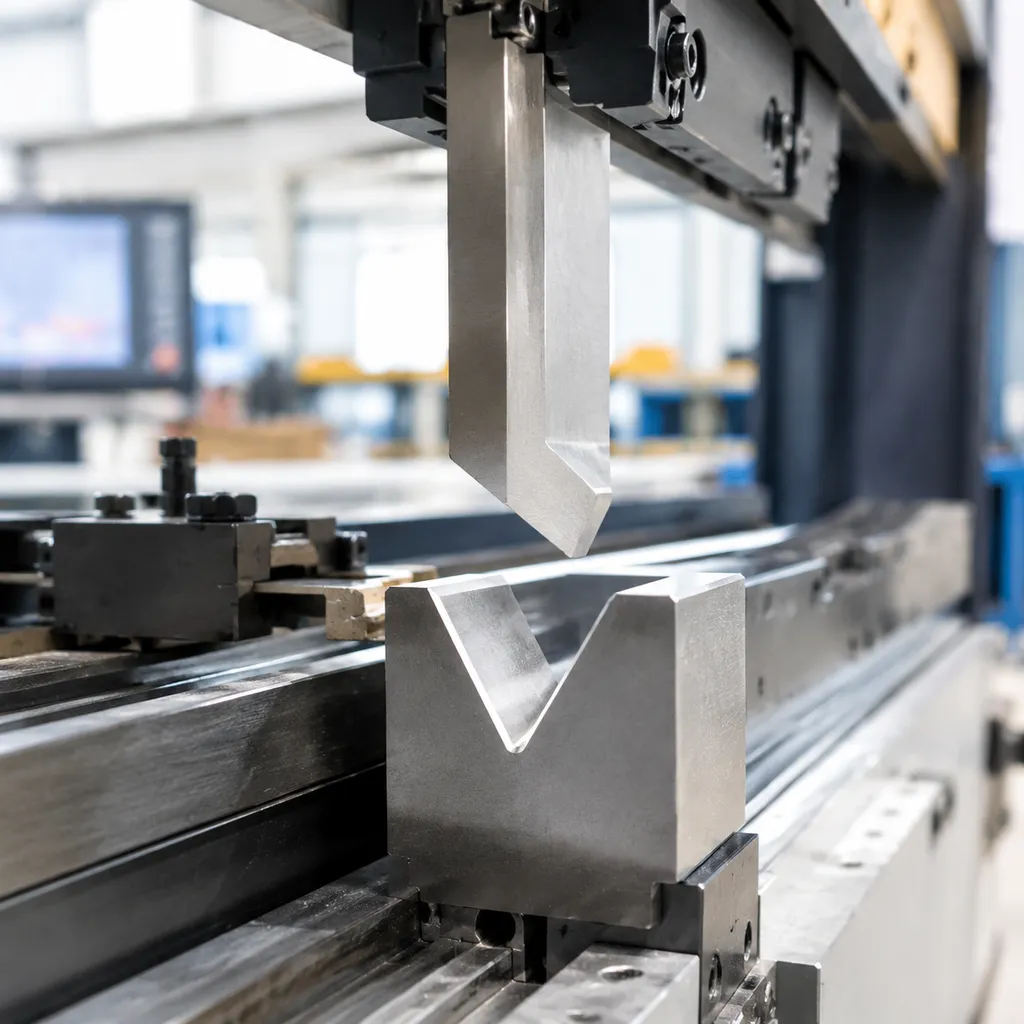
CAMT 90 Degree Punch and Die Tooling for Press Brakes
Right-Angle Bending Working Principles
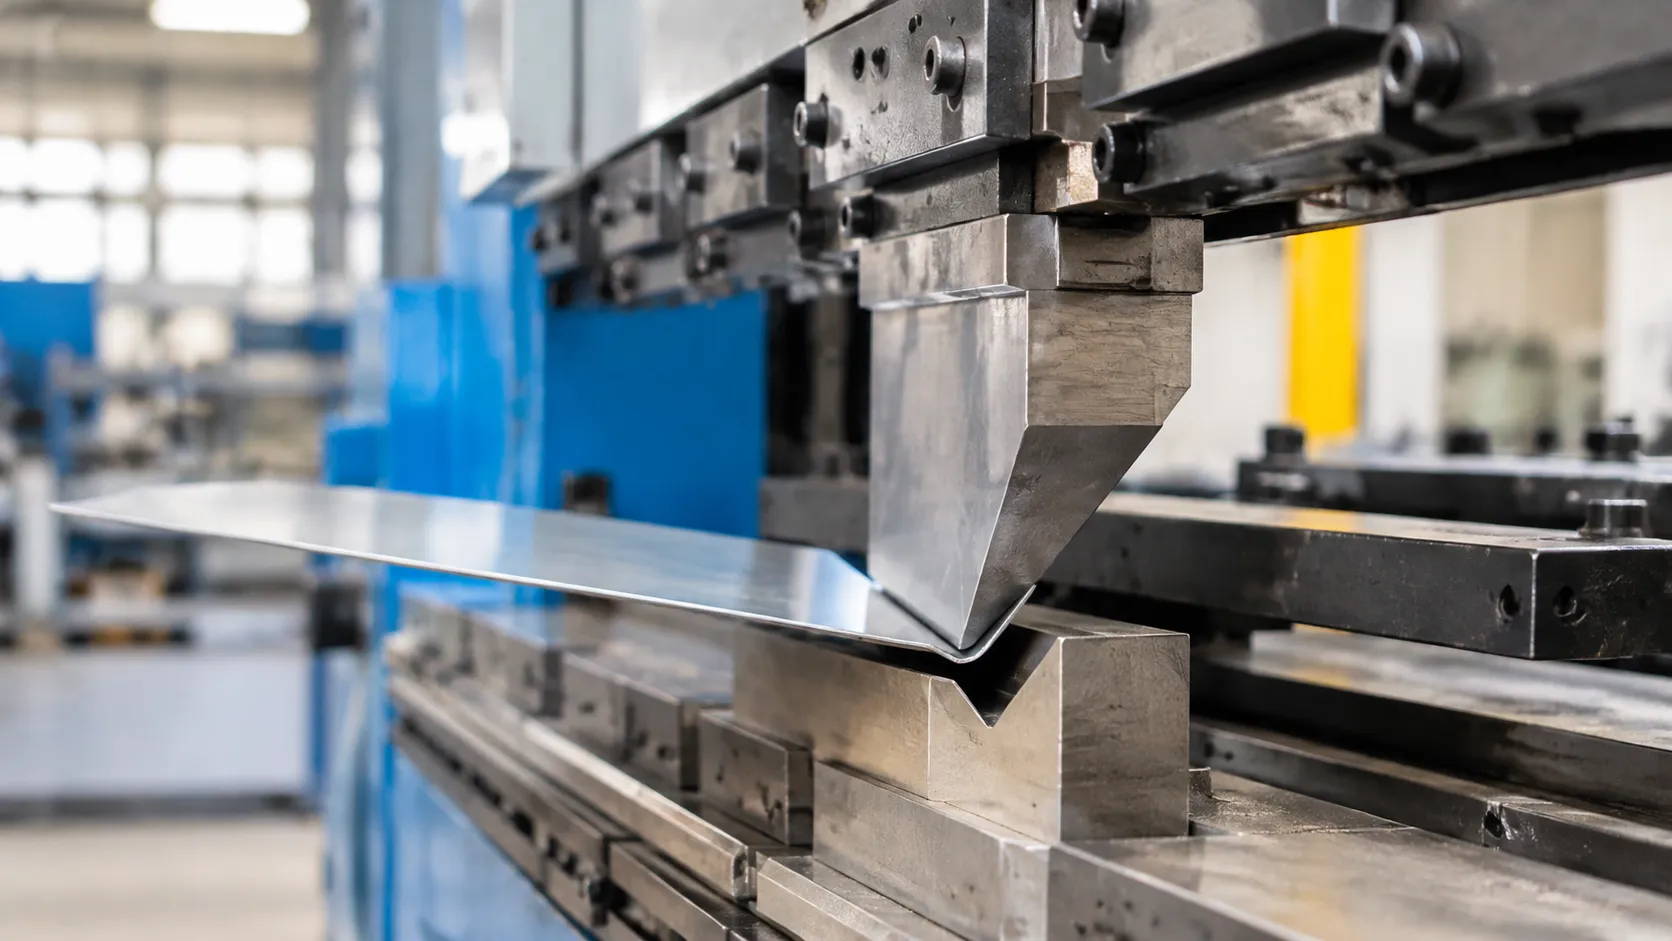
Our 90-degree punch and die systems create precise right angles through controlled three-point contact and concentrated tonnage distribution:
- Air Bending: The punch tip forces the material into the press brake V die until reaching the target 90° profile without touching the die bottom, offering flexibility across varying material thicknesses.
- Bottoming & Coining: The sheet metal is driven firmly into the 90° V-die cavity, locking in the angular tolerance and significantly reducing material springback.
- Precision Centerline Alignment: Symmetrical punch profiles and matched V-grooves maintain exact centerline accuracy, preventing part drift and side-load stress on your press brake ram.
Compatible Sheet Metals
CAMT right angle press brake tooling is hardened and profiled to handle a wide range of raw materials without galling, premature edge wear, or surface fracture:
| Material Type | Typical Thickness Range | Tooling Characteristics |
|---|---|---|
| Mild Steel | 0.5 mm – 12.0 mm | Standard hardened V-die profiles for high-cycle production |
| Stainless Steel (304/316) | 0.5 mm – 8.0 mm | Deep-hardened punch tips to resist high yield strength and abrasive wear |
| Aluminum Alloys | 0.8 mm – 10.0 mm | Polished contact radii to eliminate cosmetic marking and cracking |
| Galvanized Sheet | 0.6 mm – 6.0 mm | Optimized shoulder radii to reduce zinc pickup and coating flaking |
Available Tooling Configurations
To match your specific fabrication requirements and machine setups, we supply versatile precision press brake tooling configurations:
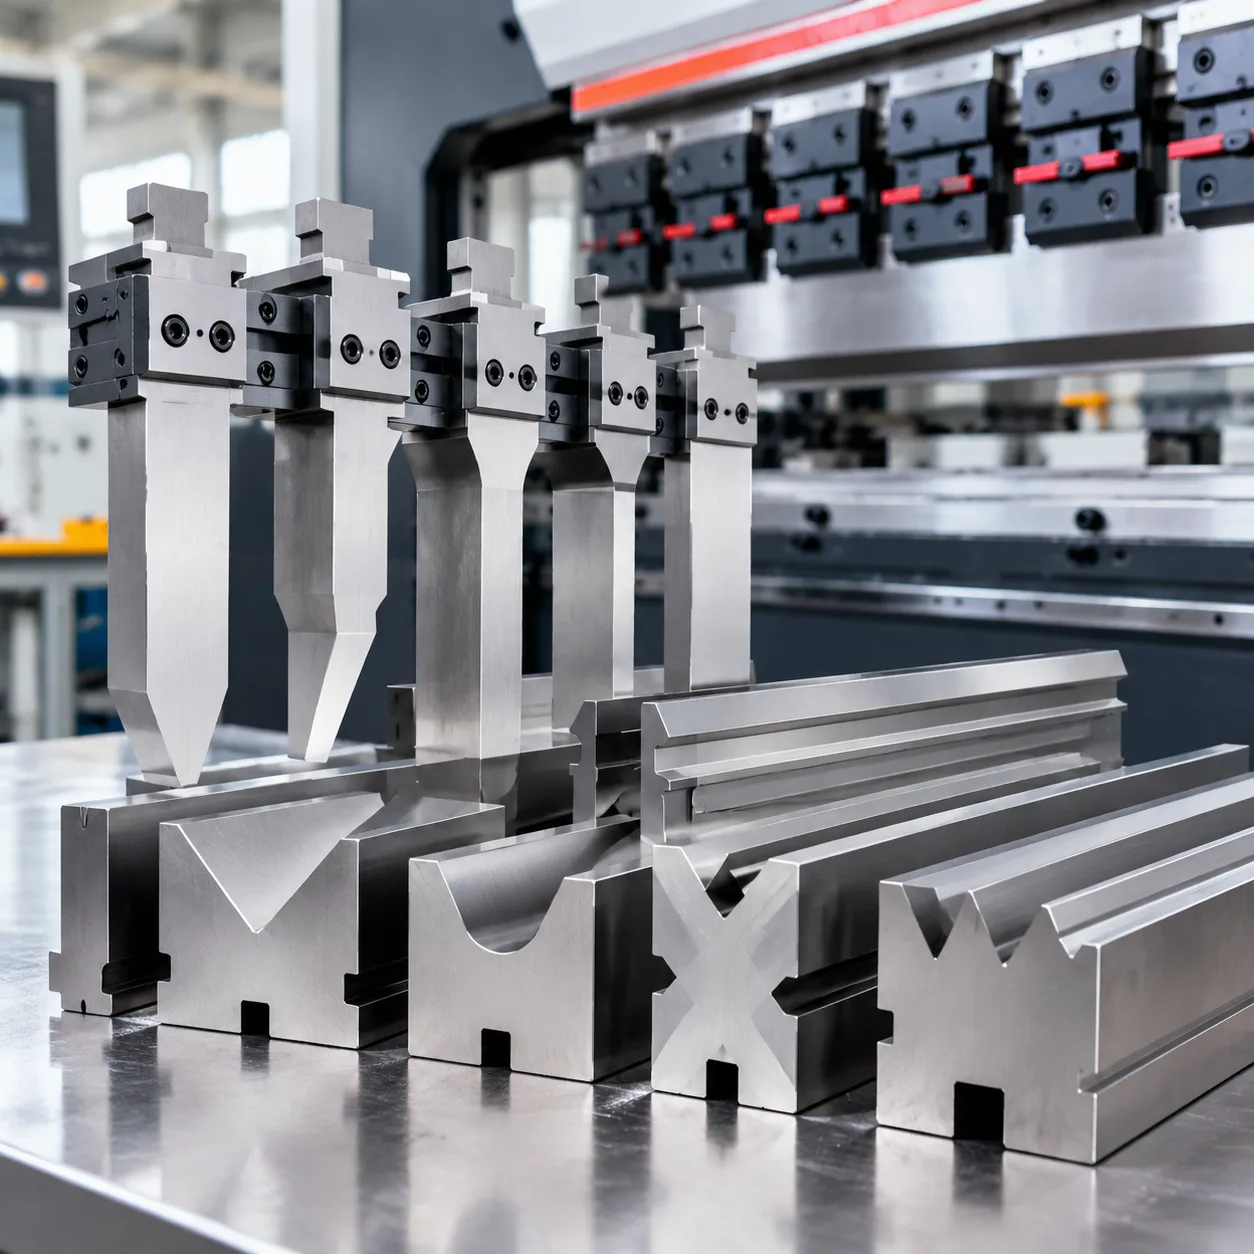
- Individual 90-Degree Punches: Straight punches, goosenecks, radius profiles, and sash tools for standard and deep return-flange bending.
- Single and Multi-V Dies: Precision-ground single V-blocks, 2-way dies, and 4-way multi-V dies tailored to different material gauges.
- Matched Punch and Die Sets: Pre-aligned tooling pairs engineered for rapid changeover and drop-in accuracy.
- Custom Profiles & Special Radii: Custom-engineered tip radii, extra-deep V-cavities, and custom tang styles manufactured directly from customer part drawings.
Features of CAMT 90 Degree Press Brake Tooling
Key Engineering Features
- Precision CNC Ground Surfaces: Every working edge, tang, and bending radius is precision-ground to tight tolerances (±0.01 mm). This eliminates angle variation and ensures straight, uniform bends over the entire sheet length.
- Premium Alloy Tool Steel Construction: We forge our punches and dies from high-grade structural alloys, including 42CrMo and Cr12MoV, ensuring high tensile strength and resilience under heavy tonnage.
- Advanced Induction Hardening: Critical contact zones undergo targeted heat treatment and vacuum tempering to achieve a surface hardness of 47–53 HRC. Following proper press brake die maintenance tips for longer tool life keeps these hardened edges sharp and free of galling.
- Multi-Standard Clamping Compatibility: We manufacture tooling to fit standard machine interfaces, including European precision, Promecam, Wila-Trumpf, and American style press brake tooling for precision bending.
- Full-Length and Segmented Configurations: Available in continuous lengths up to 4150 mm or pre-cut segmented sets for quick setups on box, pan, and deep-flange parts.
- Customizable Tooling Geometry: We tailor V-die openings, shoulder radii, and punch tip profiles to match specific material types and prevent sheet marking.
Technical Feature Summary
| Feature | Engineering Standard | Fabrication Benefit |
|---|---|---|
| Material Quality | 42CrMo / Cr12MoV Forged Steel | Resists high bending loads and prevents tool breakage |
| Surface Hardness | 47 – 53 HRC (Induction Hardened) | Long wear life and resistance to abrasive materials |
| Grinding Tolerance | ±0.01 mm | Perfect interchangeability and straight bend lines |
| System Styles | European, American, Wila, Promecam | Direct integration with standard CNC press brakes |
| Length Options | Solid lengths & sectional sets | Versatile forming for flat sheets, boxes, and trays |
Available 90 Degree Press Brake Tooling Configurations
90-Degree Punch Profiles
Selecting the correct punch profile is critical to clearing previous bends while maintaining structural stiffness. We offer several dedicated punch geometries:
- Standard Straight Punches: The workhorse for everyday right-angle bends, offering high tonnage capacity and minimal tool deflection.
- Gooseneck Punches: Engineered with a deep relief pocket to provide clearance for return flanges and U-profile channels.
- Acute Angle Punches: Cut to angles such as 85°, 88°, or acute profiles to allow air bending compensation for material springback before resting at a finished 90°.
- Radius Punches: Ground with larger nose radii to prevent cracking in high-strength materials and thick-gauge plate.
- Narrow / Sash Punches: Slender profiles designed for tight, compact bends where standard punch bodies would collide with the workpiece.
Common Press Brake Punch Profiles
Straight Punch
→ Standard straight-profile bending
→ General-purpose 90° and air bending
Gooseneck Punch
→ Recessed profile provides return-flange clearance
→ Suitable for box forming and deep-channel bending
Narrow Punch
→ Slim tool body for restricted spaces
→ Suitable for narrow channels and close-flange bending
90-Degree Dies and Bottom Tooling
Our bottom die selection covers both high-mix job shops and dedicated manufacturing cells. We supply:
- Single V-Dies: Dedicated single-groove dies machined for high-tonnage stability and standard bottoming or air bending operations.
- Multi-V & 4-Way Dies: Versatile multi-opening blocks, such as our standard multi-V dies and specialized 4-way 90-degree tooling, allowing operators to quickly rotate between different V-openings to bend varying material thicknesses without tool changes.
- Adjustable V-Dies: Mechanically or CNC-adjusted bottom dies that change opening widths on the fly for heavy-plate fabrication.
- 2-Way V-Dies: Symmetrical double-V dies that provide efficient two-in-one flexibility in compact bed spaces.
| Tooling Type | Common Applications | Key Advantage |
|---|---|---|
| Straight Punch & Single V | General fabrication, simple brackets | Maximum rigidity and highest load limit |
| Gooseneck & 2-Way Die | Electrical enclosures, box channels | Deep return flange clearance |
| Acute Punch & Multi-V Die | High-mix parts, high-springback metals | Fast thickness changeover and angle flexibility |
| Segmented Punch & Solid Die | 4-sided boxes, trays, pans | Removable ear pieces for tight corner clearance |
Matched Sets and Segmented Tooling Layouts
For standard production lines, we provide matched 90-degree punch and die sets, ground to identical centerlines for immediate drop-in alignment and rapid setup times.
For complex assemblies, our segmented press brake tooling comes pre-cut in standardized lengths (including left and right horn/ear pieces). This enables operators to assemble custom tool lengths across the bed to bend 4-sided boxes, deep electrical enclosures, and narrow return flanges without side-wall interference.
90 Degree Press Brake Tooling Technical Specifications
Core Tooling Specifications
| Parameter | Specification Details |
|---|---|
| Bend Angle Options | 90° (Standard), 88° & 85° (for air bending springback compensation) |
| Tooling Systems | European Precision, American Standard, Wila/Trumpf Style, Promecam |
| Standard Materials | 42CrMo (AISI 4140), 50SiMn, T8A, C45 |
| Hardening Depth | 2 mm to 4 mm induction hardened on working edges |
| Hardness Rating | 47 ± 2 HRC (Through-hardened) / 55–60 HRC (Working areas) |
| Machining Tolerance | Parallelism & Straightness: ±0.01 mm/m; Working Height: ±0.01 mm |
| Standard Lengths | Solid: 415 mm, 500 mm, 835 mm; Segmented sets up to 4100 mm |
Heat Treatment and Surface Grinding Standards
Every 90 degree punch and die undergoes controlled vacuum heat treatment and precision CNC grinding on all critical working surfaces:
- Deep Induction Hardening: Punch tips and die shoulders are induction hardened to 55–60 HRC to prevent deformation under heavy loads.
- Precision CNC Ground Radii: Working radii are ground to tight dimensional limits for consistent sheet metal contact and zero angle drift.
- Mirror-Finished Shoulders: Ground V-die shoulders minimize friction, reduce sheet galling, and protect sensitive surfaces on aluminum and stainless steel.
Profiles, V-Openings, and Length Options
We offer a complete range of punch profiles and matched dies to suit diverse production geometries:
- Punch Geometries: Standard straight punches, deep-relief gooseneck punches, narrow sash punches, and acute-profile options for deep channels.
- V-Die Configurations: Single V-groove blocks, 2-way and 4-way dies, multi-V dies, and adjustable bottom dies. For detailed sizing and opening recommendations, consult our press brake V-die chart and tonnage guide.
- Sectionalized Sets: Standard segmented pieces allow fast setup for four-sided box forming, deep trays, and narrow flange bends. Review our press brake die size chart and dimensions guide to confirm specific dimension cutoffs for your bed length.
Press Brake Machine Compatibility
Our CNC press brake tooling mounts directly into a wide variety of machine clamping configurations without requiring expensive modifications:
- Hydraulic and Hybrid Brakes: Full compatibility with CNC auto-crowning systems and multi-axis backgauges.
- Mechanical and Torsion-Bar Machines: Drop-in fit for standard manual clamps, safety tang receivers, and split-wedge holders.
- Tooling Clamping Interfaces: Available in standard European tangs, traditional American 0.50" x 0.75" tangs, and push-button safety click systems for rapid changeovers.
Selecting the Correct 90° Punch and V-Die
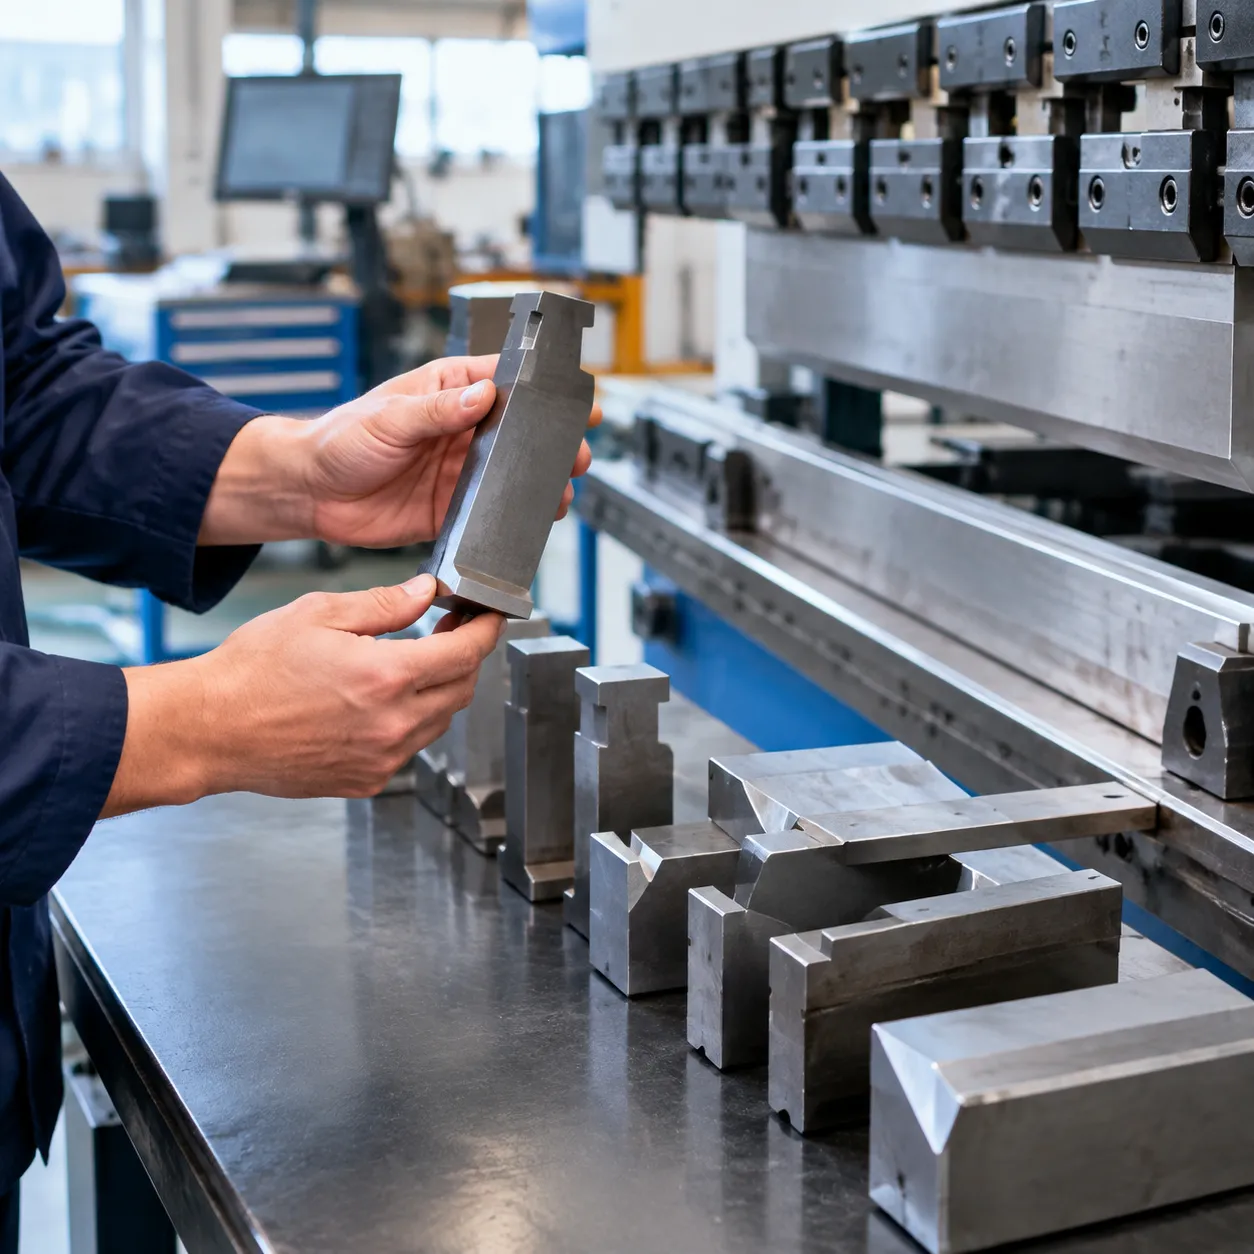
Step-by-Step Tooling Selection Criteria
- Evaluate Material Type, Thickness, and Tensile Strength: Higher-tensile materials like stainless steel require higher bending force and generate more springback than mild steel or soft aluminum. We evaluate your material grade and gauge thickness first to determine the safe working tonnage.
- Select the Proper V-Die Opening: For air bending mild steel to a 90-degree angle, the standard rule of thumb is a V-opening equal to 8 times the material thickness (V = 8 × t). For thicker plate or high-tensile alloys, increasing the opening to 10 × t or 12 × t lowers the required forming tonnage and prevents surface cracking. Pairing the punch with the correct female press brake V-die creates the required inside bend radius (IR approx 16% of the V-opening).
- Compensate for Springback with Acute Profiles: In air bending, standard materials naturally spring open after forming. To achieve a finished 90° profile, we often recommend using an acute punch (such as 85°, 88°, or 86°) to overbend the sheet metal, allowing it to relax into a perfect 90-degree right angle. Reviewing different press brake die types helps identify when an acute or standard 90° profile delivers the tightest tolerance.
- Choose the Punch Tip Radius Carefully: A punch radius that is too sharp can pierce or crease the bend line, while an oversized radius increases the required tonnage. For mild steel, choose a punch tip radius close to the material thickness (R approx 1.0 × t). For high-strength steel or structural aluminum, use a larger radius (R ge 1.5 × t to 2.0 × t) to prevent external tensile cracking.
- Match Tooling Tangs to Machine Clamping: Confirm your machine's upper beam and lower bed style. We supply precision-ground tangs for European Precision, standard American, Wila/Trumpf-style hydraulic clamping, and Promecam systems.
- Verify Tooling Load Capacity and Bending Tonnage: Never exceed the maximum rated load ($kN/m$ or $tons/ft$) marked on the tool body. Deep-profile punches, goosenecks, and narrow V-dies carry specific deflection thresholds that must be calculated against your material's forming resistance.
Quick Reference: 90° Air Bending Selection Guide
| Sheet Metal Thickness (t) | Recommended V-Opening (V) | Inside Bend Radius (Rᵢ) | Minimum Flange Length (bₘᵢₙ) | Recommended Punch Angle |
|---|---|---|---|---|
| 0.8–1.2 mm | 6 × t to 8 × t | ≈ 0.16 × V | ≈ 0.7 × V | 88° or 90° |
| 1.5–3.0 mm | 8 × t | ≈ 0.16 × V | ≈ 0.7 × V | 86° or 88° |
| 4.0–6.0 mm | 8 × t to 10 × t | ≈ 0.16 × V | ≈ 0.75 × V | 85° or 88° |
| 8.0 mm and above | 10 × t to 12 × t | ≈ 0.16 × V | ≈ 0.8 × V | 80° or 85° |
We assist you in calculating exact tonnage requirements, profile depths, and springback allowances to ensure your right angle bending tools operate reliably on your production floor.
Industrial Applications for 90 Degree Press Brake Tooling
Sheet Metal Enclosures, Electrical Cabinets, and Control Boxes
Precision is critical when bending NEMA-rated enclosures, server racks, and industrial control boxes.
Clean Box Forming: Our gooseneck punches and segmented 90 degree punch and die layouts allow you to bend deep return flanges without colliding with previous bends.
Flange Consistency: Accurate 90° corners eliminate gaps during welding and assembly, ensuring seamless door fitting and tight environmental seals.
HVAC Ductwork, Mounting Brackets, and Structural Channels
Standard right-angle profiles keep building ventilation and mechanical assemblies rigid.
Ducting and Channels: Reliable air-bending setups form U-channels, hat profiles, and duct transitions with uniform straightness across full bed lengths.
Heavy Mounting Hardware: For thick reinforcement tabs and structural brackets, standard tooling setups paired with a 50-ton press brake die kit for steel bending deliver dependable performance during continuous production.
Architectural Metalwork, Doors, Frames, and Custom Trims
Architectural applications demand crisp visual lines without surface damage.
Crisp Profiles: Our precision ground right angle press brake tooling forms crisp edges on perimeter trims, metal doors, ceiling panels, and window jambs.
Surface Protection: Ground contact radii prevent galling and excessive tooling marks on prepainted aluminum, copper, and decorative cladding.
Automotive Parts, Agricultural Machinery, and Heavy Equipment Guards
Heavy-duty vehicles and machinery require high-tonnage forming of structural steel plates.
Chassis and Guarding: Forming skid plates, tractor fenders, and heavy equipment guards demands tooling that handles intense point loads.
Thick Plate Forming: For heavy structural components, we pair heavy-duty punches with a 250-ton press brake die set for heavy metal bending to maintain precise 90° angles without tool deflection.
Commercial Food Service and Stainless Steel Kitchen Equipment
Sanitary environments require smooth, gap-free bends that prevent bacterial buildup.
Stainless Steel Fabrication: Polished punch tips protect 304 and 316 stainless steel from surface contamination and micro-cracking during forming.
Tables, Sinks, and Shelving: Precision right-angle bending tools deliver exact 90-degree flanges for splashbacks, countertops, and modular food-grade cabinetry.
Press Brake Compatibility and Tooling Standards
European Precision Style Systems
Our European style press brake tooling utilizes precision-ground Promecam tangs (12.7 mm × 8.4 mm) for fast self-aligning setups. These punches and 90-degree V-dies allow quick sectional changes, making them ideal for high-mix, tight-tolerance sheet metal production.
American Standard Style Punches and Dies
Built with traditional 0.500-inch safety tangs, our American style press brake dies and punches drop directly into standard North American mechanical clamps. They deliver heavy-duty stability across high-tonnage right-angle forming operations.
Wila and Trumpf Style Tooling
We supply 90-degree punches and dies configured for New Standard (NS) hydraulic and pneumatic clamping bars. Fitted with precision safety pins and buttons, these tools allow direct vertical loading and push-button tool changes on Trumpf and Wila-equipped machines.
Promecam-Compatible Tang Configurations
Every Promecam-style punch features standard safety grooves and accurate centerlines. They mount directly into standard manual clamps, hydraulic power-clamping systems, and intermediate punch holders without shimming.
Custom Adapters and Retrofit Mounting Solutions
For shops managing mixed-brand press brake fleets, we provide heavy-duty conversion adapters. These allow you to run European precision tooling on American-style brakes, or mount specialized 90-degree dies onto older mechanical machines without replacing existing clamping systems.
| Clamping Standard | Tang Style | Compatible Machine Brands | Key Benefit |
|---|---|---|---|
| European Precision | Promecam / Euro (12.7 mm tang) | Amada, Bystronic, Durma, Prima Power | Self-centering alignment for high precision |
| American Standard | Traditional hook/safety tang (0.50") | Cincinnati, Accurpress, Standard Industrial | High structural load capacity |
| New Standard (Wila/Trumpf) | Hydraulic pin / safety click | Trumpf, Wila, SafanDarley | Fast vertical drop-in tool changes |
| Retrofit Adapters | Custom intermediate conversion | Universal CNC & mechanical brakes | Run modern tooling on legacy equipment |
Manufacturing Standards and Quality Control for 90 Degree Press Brake Tooling
We manufacture our 90 degree press brake tooling using certified alloy steels selected for high tensile strength, structural fatigue resistance, and long-term durability. Every batch of raw material undergoes ultrasonic flaw detection, hardness verification, and spectral chemical analysis before entering production. Explore the alloy characteristics and heat treatment properties in our press brake tooling material guide.
Precision Manufacturing Process
To deliver repeatable accuracy across every bend, our production follows strict machining, heat treating, and finishing protocols:
- CNC Machining & Controlled Vacuum Hardening: Blank stock is rough-machined on multi-axis CNC milling centers, followed by controlled vacuum heat treatment. Working surfaces and tool tips undergo deep laser or induction hardening (56–60 HRC), while the tool core retains toughness to absorb high bending shocks without cracking.
- Micro-Finish Precision Grinding: All punch tip radii, V-die shoulders, working faces, and clamping tangs are finished on high-precision CNC surface and profile grinders. We maintain critical dimensional tolerances within ±0.01 mm, ensuring seamless tool alignment across individual and sectionalized setups.
- 100% Dimensional and Angle Verification: Every 90 degree press brake punch and die is checked on optical coordinate measuring machines (CMM) and laser profile projectors to verify angle symmetry, centerline accuracy, and exact radius dimensions.
- Surface Protection and Export Packaging: Finished tools receive anti-rust coatings or black oxide surface treatments. Tools are then vacuum-sealed with heavy-duty protective film and packed into custom reinforced wooden crates for secure global transit.
| Quality Inspection Parameter | CAMT Standard Tolerance | Measuring Method |
|---|---|---|
| Bending Angle Accuracy | ±15′ (±0.25°) | Optical Angle Gauge / CMM |
| Working Height & Centerline | ±0.01 mm (±0.0004″) | Digital Height Gauge & Micrometer |
| Punch Tip & Shoulder Radius | ±0.02 mm | Optical Profile Projector |
| Surface Hardness (Working Areas) | 56–60 HRC | Digital Rockwell Hardness Tester |
| Surface Finish (Ra) | ≤ 0.4–0.8 μm | Surface Roughness Tester |
Custom Right Angle Press Brake Tooling Options
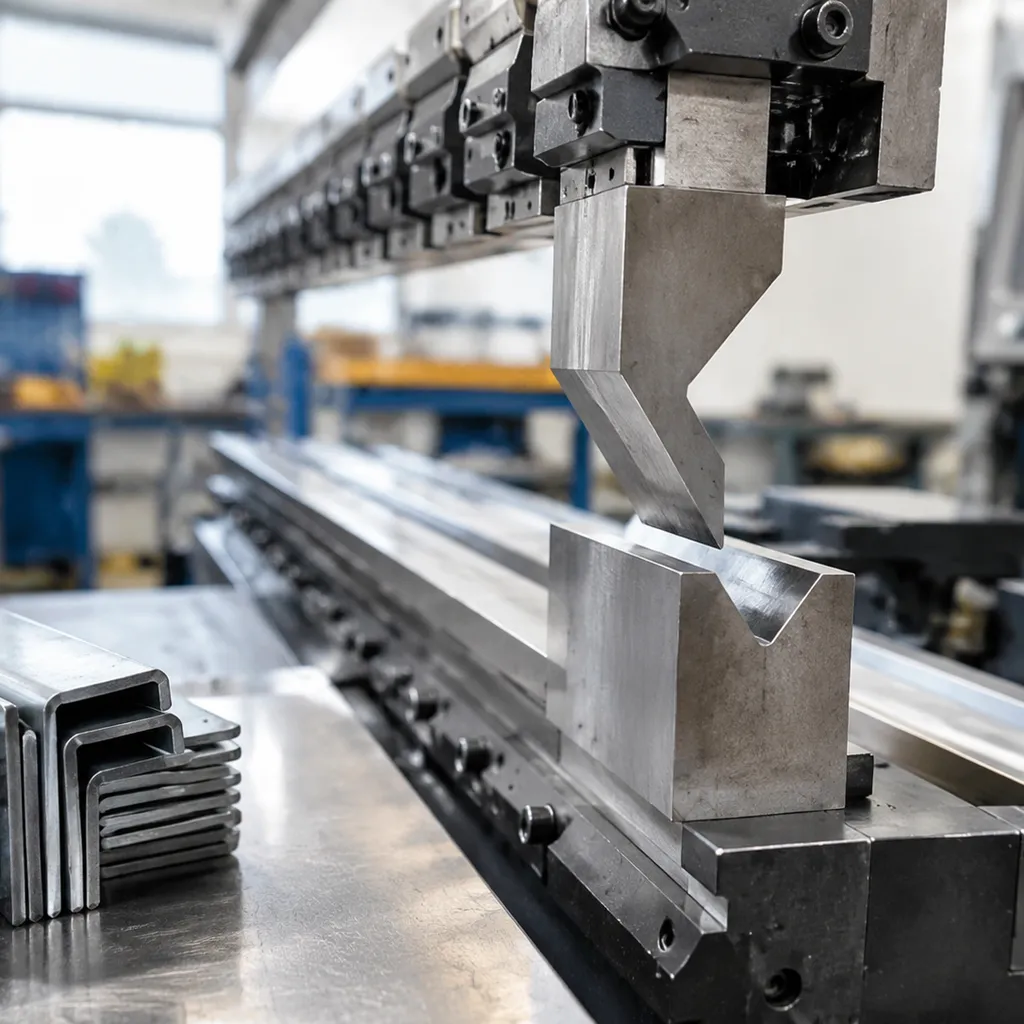
Standard tooling cannot always resolve difficult part clearances or severe return flanges. When your sheet metal geometry requires extra reach, unique offsets, or non-standard profiles, we manufacture built-to-order 90 degree press brake tooling and customized profiles to match your exact bending sequences.
Engineered Punches and Gooseneck Profiles
We engineer specialized punches to clear previous bends and narrow channels without colliding with the workpiece:
Deep-Relief Goosenecks: Sized specifically to clear high return flanges on electrical boxes and deep tray profiles.
Narrow & Sash Punches: Ultra-slim tool bodies designed for tight seams, small offsets, and narrow channel forming.
Heavy-Duty Window Cutouts: Built with reinforced structural backs to retain maximum load-bearing tonnage while providing necessary part clearance.
Specialized Radii, Angles, and Extra-Deep V-Dies
Material springback, surface marking, and severe bend requirements often call for modified geometry:
Custom Punch Tip Radii: Ranging from R0.2 mm to over R25 mm to eliminate inner-corner cracking across hard-temper alloys.
Non-Standard Relief Angles: Custom acute punch and die angles (such as 85°, 86°, or 88°) to yield true right angles on high-tensile springback metals.
Extra-Deep V-Openings: Custom press brake V-dies with deep relief channels that allow long flanges to swing down cleanly during the bend cycle without clipping the die shoulder.
Custom Sectional Lengths for Box and Pan Forming
We produce segmented tooling sets matched to your part dimensions:
Standard & Custom Segmentations: Full sections split into targeted lengths (e.g., 10, 15, 20, 40, 50, 100, 200, 300, and 500 mm).
Horned Left/Right End Sections: Relieved ear sections that prevent collisions with adjacent side-flanges when finishing 4-sided closed boxes.
| Customization Option | Available Range / Options | Typical Application |
|---|---|---|
| Punch Geometry | Extra-deep gooseneck, sash, windowed | Multi-bend panels, deep return flanges |
| Die Configuration | Deep single-V, acute V, dynamic opening | Custom channel depths, high-tensile bending |
| Segmentation | 10 mm to 1,000+ mm with horned ears | Four-sided boxes, trays, enclosure covers |
| Material & Hardness | 42CrMo, Cr12MoV, 56–60 HRC | High-tonnage wear resistance, stainless steel |
| Clamping Style | European, Wila/Trumpf, American, Promecam | Retrofits and non-standard press brake beams |
Direct-from-Drawing Fabrication and Reverse Engineering
Whether developing a new component or replacing obsolete tooling:
CAD/CAM Modeling from Part Drawings: Send us your 2D/3D part files (.STEP, .DXF, .DWG), and our engineering team simulates the bend cycle to develop collision-free custom press brake punch and die profiles.
Worn-Tool Reverse Engineering: We can accurately measure, scan, and re-manufacture existing custom precision press brake dies and punches to original factory tolerances, upgrading tool steel grades and heat treatments for improved service life.
FAQs About 90 Degree Press Brake Tooling
Can a 90-degree punch make an exact 90-degree bend?
In air bending, a standard 90-degree punch cannot produce a finished 90-degree bend because sheet metal naturally experiences material springback. When the punch releases pressure, the material relaxes outward by 1° to 3° for mild steel and up to 5° or more for stainless steel. To achieve an exact 90° finished profile:
Air Bending: Use an acute punch (such as 85°, 88°, or 30°) to overbend the sheet metal, allowing it to spring back precisely to 90°.
Bottom Bending / Coining: A 90° punch paired with a 90° die can form exact 90° profiles by stamping the material into the bottom of the die pocket, though this requires significantly higher machine tonnage.
What V-die opening should I use for a 90-degree bend?
As a standard fabrication rule of thumb, the recommended press brake V-die opening is determined by sheet thickness (t):
| Material Gauge / Thickness | Recommended V-Opening (V) | Approx. Inside Bend Radius (Rᵢ) |
|---|---|---|
| Thin Sheet (< 3 mm) | 6 × t to 8 × t | ≈ 1 × t to 1.25 × t |
| Medium Plate (3–6 mm) | 8 × t to 10 × t | ≈ 1.25 × t to 1.5 × t |
| Heavy Plate (> 6 mm) | 10 × t to 12 × t | ≈ 1.5 × t to 2 × t |
For specialized profiles and non-standard tensile requirements, refer to our detailed press brake die clearance guide for better bending to calculate exact tonnage and opening dimensions.
What is the difference between a 90-degree punch and an acute punch?
A 90-degree punch features a symmetrical 90° tool tip profile and is primarily used for bottoming, coining, or forming materials where springback is negligible.
In contrast, acute punches feature narrower tool angles (typically 30°, 60°, 85°, or 88°). This narrower tip allows the press brake to push the sheet metal past 90 degrees during air bending, delivering accurate 90° right-angle parts after the metal springs back.
Can CAMT make tooling for my existing press brake?
Yes. We manufacture right angle press brake tooling compatible with all major global machine mounting standards:
European / Promecam Style: Standard 8.4 mm × 3.5 mm tangs and safety grooved punches.
American Traditional Style: Standard 0.500'' tangs with safety tang notches.
Wila / Trumpf Style: Precision hydraulic and mechanical self-seating tangs.
Bystronic, LVD, and Japanese Standards: Machine-specific clamping tangs and adapted direct-mount bases.
If your machine uses custom clamping plates or older mechanical beam holders, we engineer custom-ground tool tangs and base risers built to your exact machine specifications.
Is segmented tooling available for box and pan bending?
Yes. We supply segmented press brake tooling cut into standard precision-ground section sets (e.g., 10 mm, 15 mm, 20 mm, 40 mm, 50 mm, 100 mm, 200 mm, 300 mm).
Punches include left and right horn segments (ears) to provide side-flange relief when forming 4-sided boxes, deep electrical enclosures, and chassis pans.
All individual segmented sections are ground simultaneously to a tight tolerance of ±0.01 mm for complete interchangeability across the full bed length.
Can this 90-degree tooling bend heavy-gauge stainless steel?
Yes. Our heavy-duty 90-degree punch and die sets are manufactured from high-tensile alloy tool steels (42CrMo / AISI 4140 or Cr12MoV / D2). The working contact surfaces—including the punch tip radius and the die shoulder radii—undergo precision CNC induction hardening to reach HRC 50–55. This prevents shoulder galling, tool deformation, and premature wear when bending high-yield stainless steel and structural plate.
Do you supply both individual tooling components and matched sets?
We supply both individual components and complete tooling setups:
Individual Punches & Dies: Order single replacement punches, special gooseneck sections, or individual V-dies to replace damaged tools or expand existing tooling libraries.
Matched 90 Degree Punch and Die Sets: Precision-matched pairs ground to identical centerline alignments, ensuring instant plug-and-play setup on CNC press brakes.
Why Choose CAMT for 90 Degree Press Brake Tooling
We manufacture and supply industrial-grade 90 degree press brake tooling engineered for long service life, strict angle repeatability, and seamless machine compatibility. By working directly with our factory team, fabricators eliminate middleman markups and gain direct access to practical tooling engineering and support.
CAMT Manufacturing Advantages
| Feature | CAMT Standard | Typical Market Standard |
|---|---|---|
| Material Base | 42CrMo / 42CrMo4 forged alloy steel | Standard carbon steel or unverified alloy |
| Working Hardness | 47–52 HRC deep-hardened working surfaces | 40–45 HRC or surface-only treatment |
| Grinding Tolerance | ±0.01 mm on critical heights and radii | ±0.03 mm to ±0.05 mm |
| Interchangeability | 100% matched section alignment | Variable fit across split sections |
| Clamping Standards | European, American, Wila/Trumpf, Promecam | Limited standard profiles |
Direct Engineering and Global Support
- Direct Technical Support: We evaluate your material specs, sheet thickness, and tonnage requirements to match the right punch profile and precision press brake V-die options for your specific production line.
- Universal Machine Compatibility: Our tooling fits standard mechanical, hydraulic, and synchronized CNC press brakes without custom fitting hassles.
- Repeatable Precision: Every segment undergoes precision CNC deep grinding, ensuring seamless alignment across full-length beds and split box-bending setups.
- Custom Tooling Development: We manufacture custom goosenecks, return-flange punches, and specialized press brake bottom dies directly from your DXF/CAD drawings.
- Reliable Global Delivery: All tools are treated with anti-corrosion protection, securely crated for export, and shipped globally with fast turnaround times.